With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Automatic pneumatic conveying systems represent a sophisticated technology for material handling, offering efficient and flexible solutions for transporting bulk materials over varying distances and within diverse industrial settings. These systems operate by utilizing compressed air to move powders, granules, or other particulate materials through a network of pipes, making them an essential component in many manufacturing and processing industries.
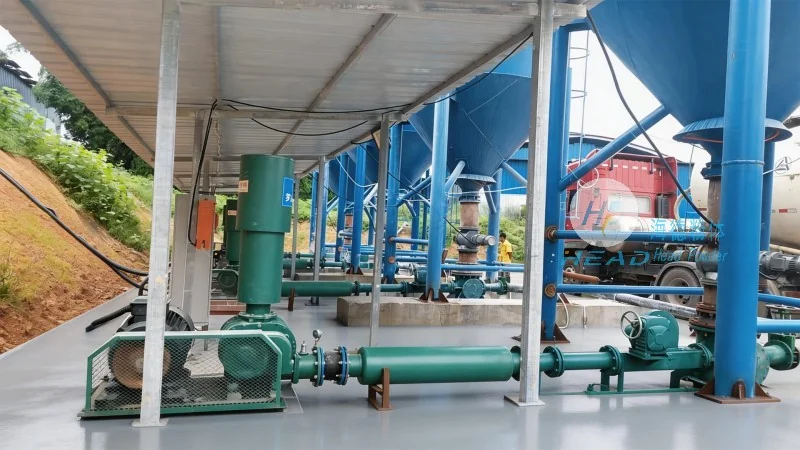
The fundamental principle of pneumatic conveying is the use of air flow to create a pressure differential that propels material through the system. In a typical setup, a material is introduced into a hopper or feeder, where it is then drawn into a pipeline by the suction or pressure generated by a blower or compressor. The air and material mixture travels through the pipeline, with the air providing the necessary force to transport the material to its destination. Key components include the air source (blower or compressor), material feeders, conveying lines, and discharge equipment. The choice between pressure and vacuum systems depends on the specific application, with pressure systems generally used for short to medium distances and vacuum systems for longer or more complex routes.

Automatic pneumatic conveying systems are widely applied across various industries due to their adaptability and efficiency. In the food and pharmaceutical sectors, these systems ensure hygienic and dust-free material handling, which is critical for maintaining product quality and compliance with regulatory standards. For example, in food processing plants, they are used to transport flour, sugar, or other dry ingredients from storage silos to production lines without the risk of contamination. In the chemical industry, they handle powders and granules that require controlled environments, such as in the production of fertilizers or specialty chemicals. The systems also find applications in the mining and minerals sector, where they transport raw materials like coal or ore from processing facilities to storage or further processing units. Additionally, in the cement and construction materials industry, pneumatic conveyors efficiently move raw materials like limestone or clinker, reducing labor costs and improving operational safety by eliminating manual handling of heavy or hazardous materials.
One of the primary advantages of automatic pneumatic conveying systems is their ability to handle a wide range of materials, from fine powders to larger granules, with minimal maintenance. The enclosed system design prevents dust emissions, making it suitable for environments where air quality is a concern. Another key feature is the flexibility in system design, allowing for customization based on the specific needs of the application, such as varying pipe lengths, changes in elevation, or multiple discharge points. The systems also offer high throughput rates, enabling efficient material flow and reducing downtime in production processes. Furthermore, the use of automated controls allows for precise regulation of material flow, ensuring consistent performance and minimizing waste. In terms of operational safety, these systems eliminate the need for manual handling of materials, reducing the risk of accidents and improving workplace safety.
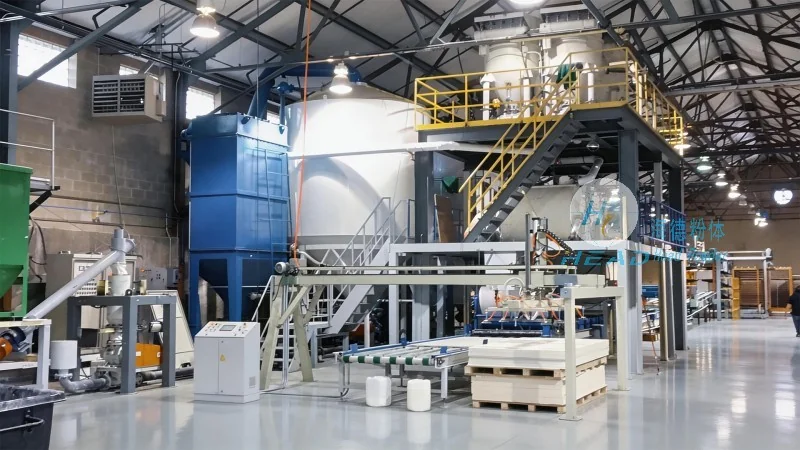
HeadPowder, as a leading manufacturer in the field of material handling solutions, specializes in the design, manufacturing, and installation of automatic pneumatic conveying systems. With a strong presence in China, particularly in Shandong province, the company has built a reputation for delivering high-quality, reliable equipment tailored to the diverse needs of its clients. The company's expertise lies in understanding the unique challenges of each industry and providing customized solutions that enhance operational efficiency and product quality. By leveraging advanced technology and rigorous quality control, HeadPowder ensures that its systems meet the highest standards of performance and durability. The company's commitment to customer satisfaction and technical support has made it a trusted partner for businesses seeking to optimize their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top