

Working Principle and Features of Rare Earth Powder Handling Systems
For industries dealing with rare earth powders, efficient and reliable handling systems are crucial to ensure production efficiency and product quality. This article explores the working principle and key features of rare earth powder handling systems, highlighting how they contribute to seamless material transport and processing.
Working Principle of Rare Earth Powder Handling Systems
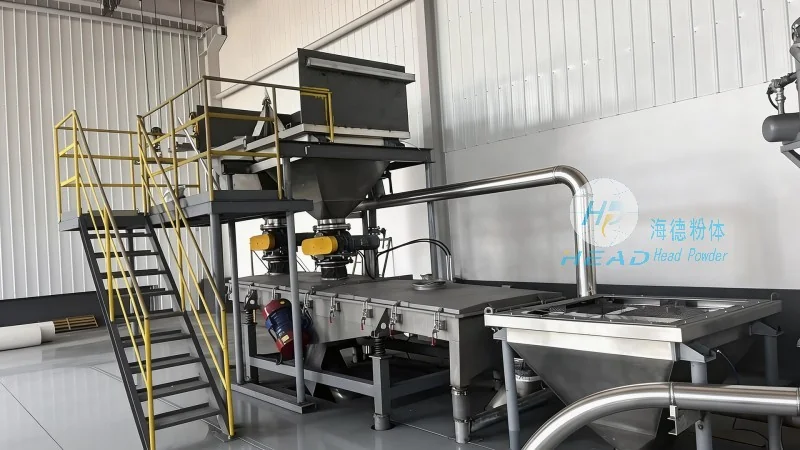
Rare earth powder handling systems typically consist of several integrated components designed to manage the flow, storage, and distribution of these fine powders. The core working principle revolves around the use of specialized equipment such as screw conveyors, pneumatic conveying systems, and storage silos, each playing a critical role in the overall operation.
Screw conveyors, for instance, utilize rotating screws to move powders in a controlled manner, ensuring minimal segregation and loss. These conveyors are often equipped with variable speed drives to adjust the flow rate based on operational needs. Pneumatic conveying systems, on the other hand, employ air pressure to transport powders through pipelines, offering flexibility in layout and the ability to handle both dry and slightly moist powders. Storage silos are used to store large quantities of rare earth powders, providing a stable environment that prevents contamination and moisture absorption.
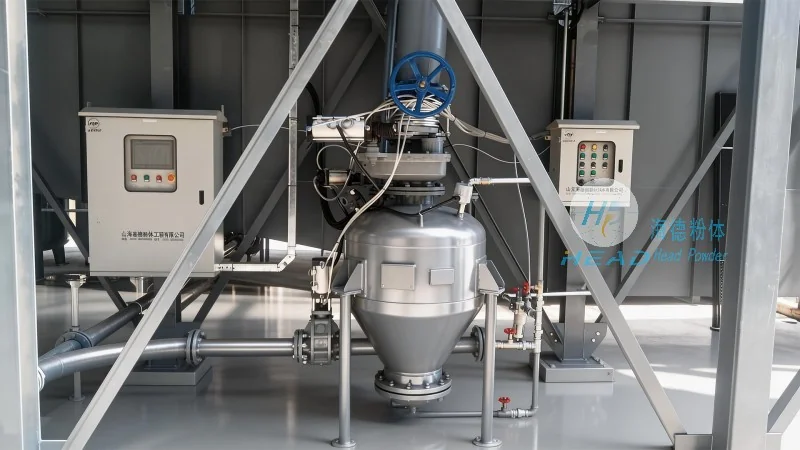
The system operates by first receiving raw rare earth powders from a hopper or storage area. The powders are then transferred to the conveying equipment, which moves them to the processing or packaging stations. This continuous flow is managed through a control system that monitors parameters like pressure, flow rate, and temperature, ensuring optimal performance and safety.
Key Features of Rare Earth Powder Handling Systems
When evaluating rare earth powder handling systems, several key features stand out as essential for effective operation. These features are designed to address the unique challenges of handling fine, abrasive powders, such as dust generation, material segregation, and equipment wear.
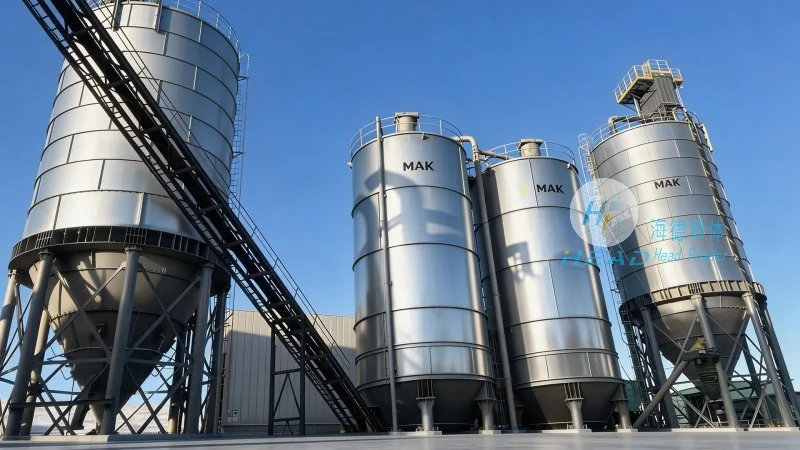
Firstly, the systems are engineered for high efficiency and low maintenance. Advanced materials and robust construction minimize wear and tear, reducing downtime and operational costs. For example, the use of stainless steel or corrosion-resistant alloys in components like hoppers and pipelines helps prevent material degradation and contamination.
Secondly, these systems prioritize safety and environmental compliance. Features such as dust collection systems, explosion-proof designs, and sealed conveyor sections help mitigate the risks associated with handling fine powders, ensuring a safe working environment. Additionally, the systems are designed to minimize dust emissions, adhering to environmental regulations and promoting workplace safety.
Thirdly, the systems offer flexibility and adaptability to different production requirements. Modular designs allow for easy expansion or reconfiguration as production needs change. This flexibility is particularly valuable in industries where product specifications or processing methods may evolve over time.
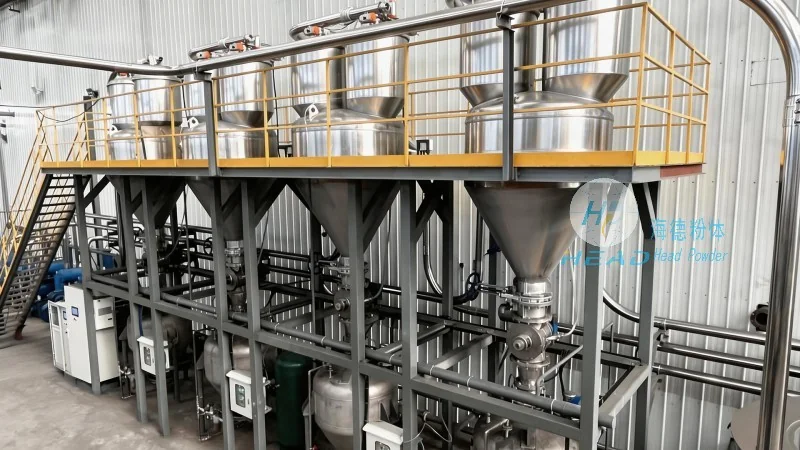
Furthermore, the integration of automation and control systems enhances operational efficiency. Modern rare earth powder handling systems often incorporate sensors and control panels that monitor and adjust parameters in real-time, optimizing performance and reducing human error. This level of automation also enables remote monitoring and troubleshooting, improving overall system reliability.
Conclusion
Rare earth powder handling systems are critical components in the production and processing of rare earth materials, offering a combination of efficiency, safety, and adaptability. By understanding their working principles and key features, industries can select and implement systems that meet their specific needs, ensuring smooth operations and high-quality product output. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems, leveraging advanced technology and expertise to deliver reliable solutions for rare earth powder handling.