With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Multi-hopper pneumatic conveying systems represent a sophisticated solution for the efficient handling and transportation of bulk powders. At the core of this technology lies the multi-hopper pump, which is engineered to manage the flow of powder materials with precision and reliability. This article delves into the working principle and key features of such systems, providing a comprehensive overview for industry professionals seeking to understand or implement this advanced powder handling technology.
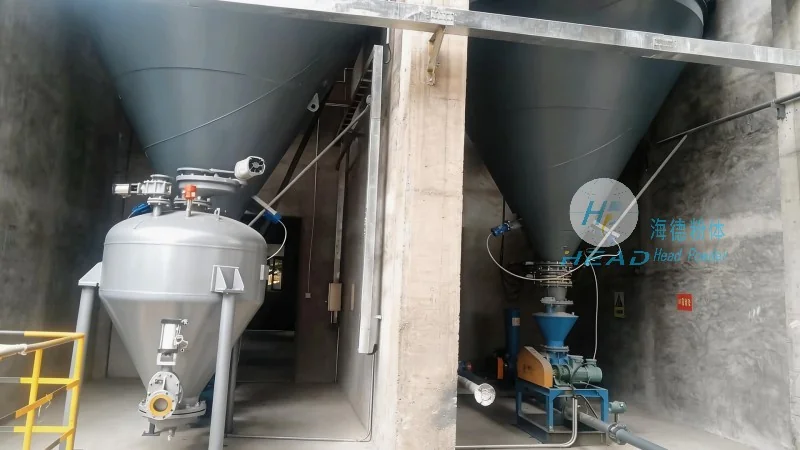
The operation of a multi-hopper pneumatic conveying system is based on the principles of pneumatic transport, where powder is conveyed through a pipeline using compressed air or other gases. The system typically consists of multiple hoppers, each containing a different powder material, and a central pump that regulates the flow from each hopper. The working principle can be broken down into several key steps:
First, the powder is fed from the hoppers into the conveying line. The multi-hopper pump, often a positive displacement type, creates a pressure differential that draws the powder into the system. As the pump operates, it generates a vacuum or pressure that moves the powder through the pipeline. The compressed air or gas then carries the powder particles along the pipeline, ensuring consistent and controlled transport. The system may include components like airlocks, filters, and separation devices to maintain the quality of the conveyed material and prevent clogging or contamination.
One of the critical aspects of the working principle is the ability to handle multiple powders simultaneously or sequentially. The multi-hopper design allows for the storage and controlled release of different powder types, enabling the system to switch between materials without interruption. This flexibility is achieved through precise control mechanisms that regulate the flow from each hopper, ensuring that the correct powder is delivered to the destination. The pump's capacity and pressure settings are tailored to the specific characteristics of the powder, such as particle size, density, and moisture content, to optimize performance and prevent material degradation.
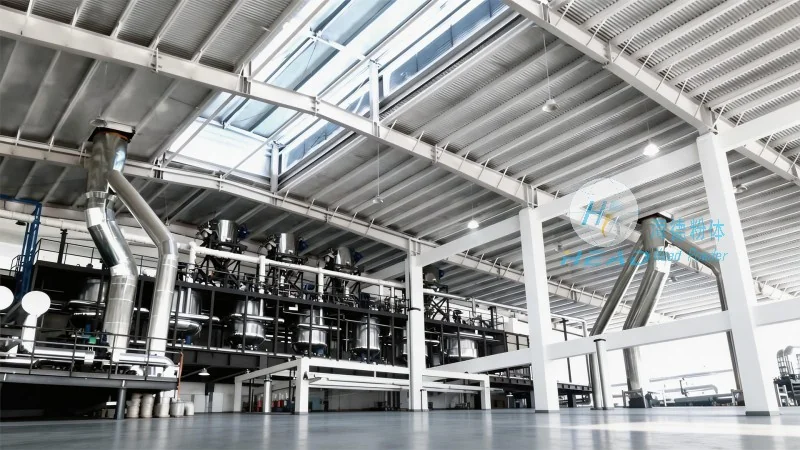
Multi-hopper pneumatic conveying systems offer several distinct features that make them an attractive choice for various industrial applications. These features enhance efficiency, reliability, and versatility in powder handling operations. The primary features include:
1. Multi-Source Material Handling: The most significant feature is the ability to handle multiple powder sources simultaneously. This allows for the integration of different raw materials or products in a single conveying system, reducing the need for separate equipment and streamlining production processes. The system can switch between hoppers to deliver the required material, ensuring continuous operation without downtime.
2. Positive Displacement Pump Technology: The use of positive displacement pumps, such as rotary lobe or diaphragm pumps, provides consistent and reliable flow control. These pumps are designed to handle abrasive and high-density powders, ensuring long service life and minimal maintenance. The pump's ability to maintain a stable pressure and flow rate is crucial for preventing material degradation and ensuring the integrity of the conveyed product.
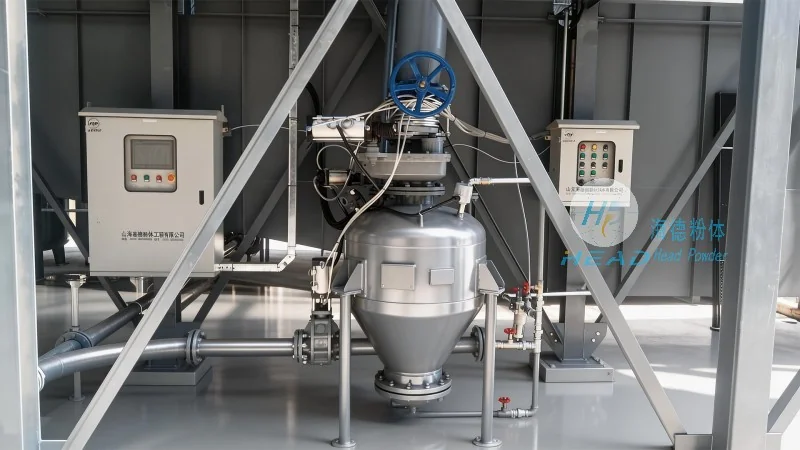
3. Flexible and Scalable Design: Multi-hopper systems are highly adaptable and can be scaled to meet the needs of different production volumes. The number of hoppers and the capacity of the pump can be adjusted to accommodate changes in production requirements. This flexibility makes the system suitable for both small-scale and large-scale industrial applications, from pharmaceutical manufacturing to bulk material handling in the chemical industry.
4. Energy Efficiency and Environmental Considerations: Modern multi-hopper pneumatic conveying systems are designed with energy efficiency in mind. Advanced control systems optimize air usage, reducing operational costs and minimizing environmental impact. The systems also incorporate features like dust collection and filtration to comply with environmental regulations and maintain a clean working environment.
5. Low Maintenance and Durability: The robust construction of the multi-hopper pump and the overall system design contribute to low maintenance requirements. High-quality materials and components are used to withstand the abrasive nature of powders, ensuring long-term reliability and reduced downtime. This durability is essential for continuous production in demanding industrial environments.
Multi-hopper pneumatic conveying systems find wide application across various industries, including pharmaceuticals, chemicals, food processing, and mining. The benefits of these systems extend beyond their technical features, providing tangible advantages to industrial operations. For example, in the pharmaceutical industry, the system's ability to handle multiple raw materials while maintaining product purity is critical. The positive displacement pump ensures that the powder is conveyed without contamination, meeting stringent regulatory requirements. In the chemical industry, the system's efficiency in handling abrasive powders reduces equipment wear and maintenance costs, improving overall operational efficiency.
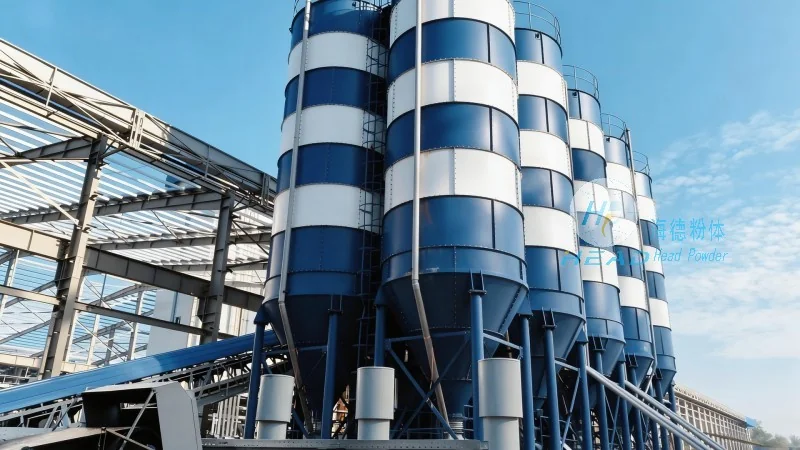
In the food processing sector, the system's hygienic design and ability to handle different food powders make it suitable for applications like flour, sugar, and dairy products. The flexibility of the multi-hopper design allows for the seamless transition between different product lines, enhancing production flexibility and reducing changeover times. For mining and mineral processing, the system's capacity to handle large volumes of bulk materials efficiently supports increased productivity and reduced transportation costs.
Overall, the multi-hopper pneumatic conveying system offers a comprehensive solution for the challenges of powder handling, combining advanced technology with practical benefits. The working principle, based on pneumatic transport and positive displacement pumping, ensures reliable and efficient material transport. The key features, including multi-source handling, energy efficiency, and durability, make the system a versatile and cost-effective choice for industrial applications.
As a leading provider of powder handling solutions, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing multi-hopper pneumatic conveying systems tailored to the specific needs of clients. With a focus on innovation and quality, the company ensures that its systems meet the highest standards of performance and reliability. Based in China, the company leverages its expertise to deliver solutions that enhance operational efficiency and support sustainable industrial practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top