

Working Principle and Features of Compound Fertilizer Pneumatic Conveying Systems
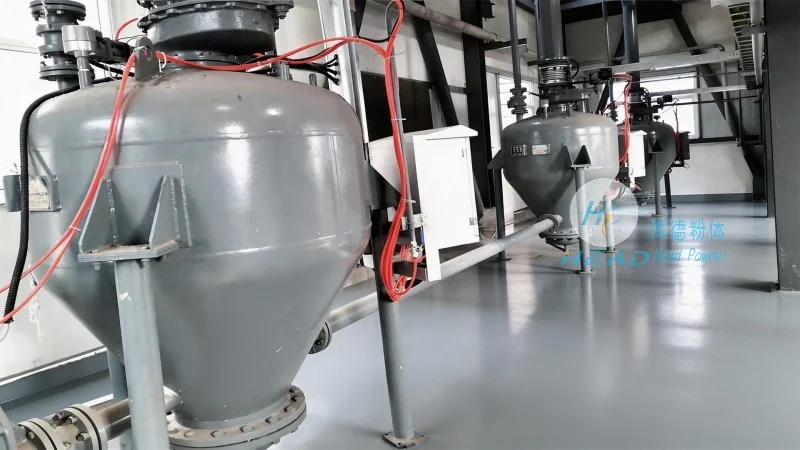
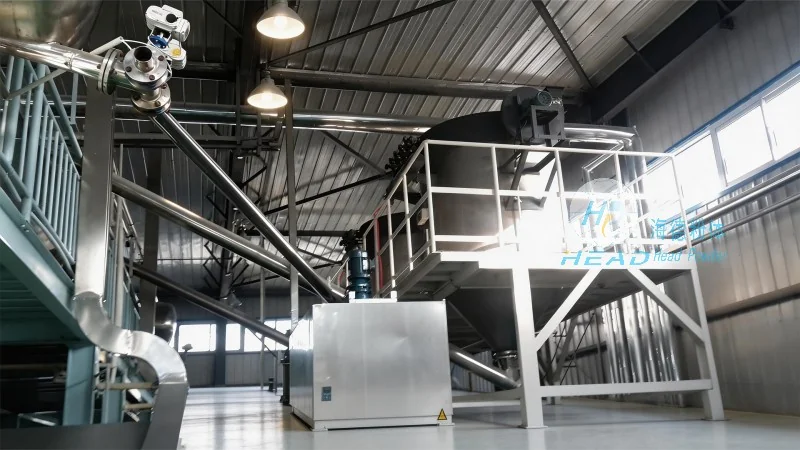
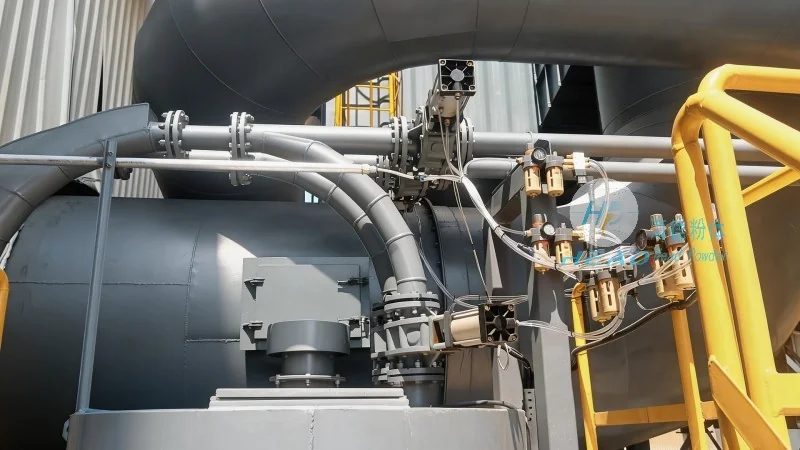
Compound fertilizer pneumatic conveying systems operate by utilizing compressed air as the primary medium to transport bulk fertilizer materials. The process begins with the fertilizer being loaded into a hopper or storage silo. A high-pressure blower or fan generates an air stream that creates a negative pressure environment within the conveying pipeline. This negative pressure draws the fertilizer particles into the system, where they are carried along by the air flow. The system typically includes components such as cyclone separators, filters, and dust collectors to separate the material from the air and maintain a clean, efficient transport. The working principle relies on maintaining the air velocity above the material's terminal velocity, which prevents clogging and ensures smooth material flow throughout the pipeline. This method enables continuous and automated transfer of fertilizer from storage to processing or packaging areas, enhancing operational efficiency and reducing manual handling.
Key Features of Compound Fertilizer Pneumatic Conveying Systems
These systems are designed with several key features that enhance performance and reliability. One critical feature is the ability to handle diverse types of compound fertilizers, including those with varying particle sizes, moisture content, and chemical compositions, without compromising transport efficiency. Adjustable air pressure and flow control mechanisms allow operators to fine-tune the conveying process, adapting to different material characteristics and pipeline lengths. The use of durable materials, such as stainless steel or corrosion-resistant alloys, ensures the system's longevity and resistance to the chemical properties of fertilizers, minimizing maintenance needs and operational costs. Safety features are also integral, with built-in pressure relief valves and emergency shut-off systems to prevent over-pressurization and ensure safe operation. The compact design of these systems makes them suitable for installation in various industrial settings, from small-scale agricultural operations to large-scale fertilizer production facilities, optimizing space utilization and improving workflow.
Company Information and Expertise
HeadPowder, a leading manufacturer in the fertilizer processing equipment sector, specializes in the design, manufacturing, and installation of compound fertilizer pneumatic conveying systems. HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has built a strong reputation for delivering high-quality, reliable equipment tailored to the specific needs of fertilizer producers. The company leverages advanced engineering techniques and rigorous quality control processes to ensure that each system meets industry standards and customer expectations. HeadPowder's expertise extends to providing comprehensive solutions, including system integration, maintenance services, and technical support, to help clients maximize the efficiency and longevity of their conveying operations. By partnering with HeadPowder, clients gain access to equipment that enhances productivity, reduces downtime, and ensures the safe and efficient handling of bulk fertilizers. The company's commitment to innovation and customer satisfaction has made it a preferred choice for businesses seeking to improve their fertilizer processing capabilities.