What is a Carbon Black Material Pneumatic Conveyor? What are its Design Principles?
For industrial applications involving the handling of carbon black, selecting the right equipment is crucial for efficiency and safety. A carbon black material pneumatic conveyor is a specialized system designed to transport carbon black powder and other fine particulate materials through a pipeline using air or gas as the conveying medium. This article explores the functionality and design principles of such conveyors, providing insights into how they operate and why they are essential in processing industries.
Introduction to Carbon Black Material Pneumatic Conveyors
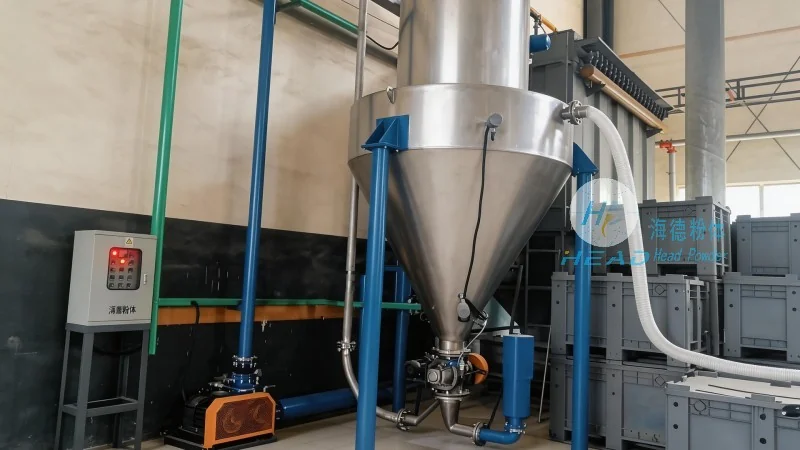
Carbon black is a widely used industrial material, often employed in the production of tires, plastics, inks, and other products. Handling this material requires equipment capable of managing its fine, abrasive nature while ensuring minimal dust generation and efficient transport. Pneumatic conveyors offer a solution by utilizing air pressure to move carbon black particles through a sealed system, reducing the risk of contamination and improving process control.
HeadPowder Engineering: A Leader in Pneumatic Conveyor Solutions
Shandong HeadPowder Engineering Co., Ltd., based in China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored to the needs of carbon black and other fine material industries. With years of experience, HeadPowder has developed a reputation for producing reliable, high-performance conveyors that meet the stringent requirements of modern processing facilities.
Key Components of a Carbon Black Pneumatic Conveyor System
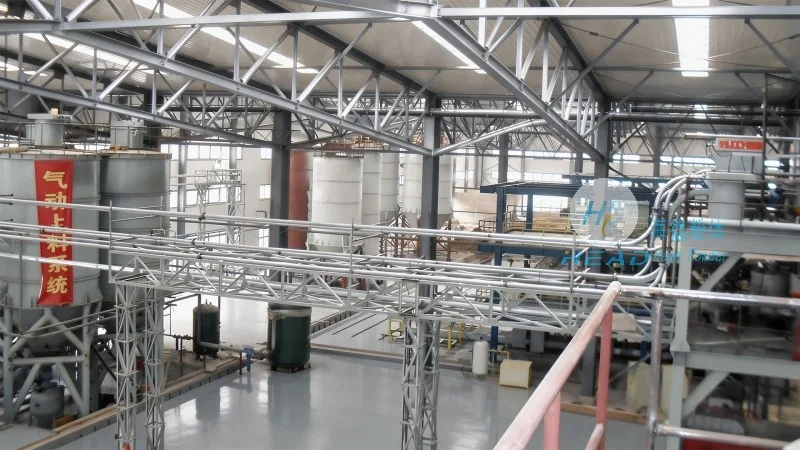
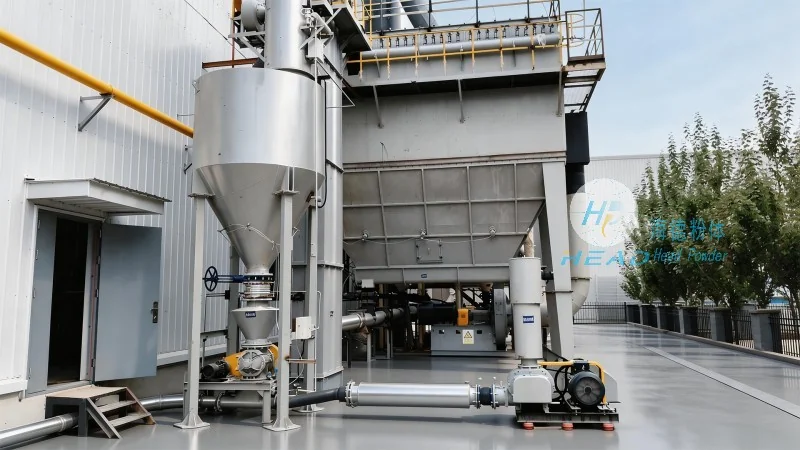
A typical carbon black pneumatic conveyor system consists of several key components that work together to ensure smooth material transport. These include a hopper for material storage, a feeder to control the flow rate, a pipeline network for conveying, and a receiver for depositing the material at the destination. Each component is designed to handle the unique properties of carbon black, such as its fine particle size and high abrasiveness.
Design Principles for Efficient Carbon Black Conveying
The design of a carbon black pneumatic conveyor focuses on several critical principles to maximize efficiency and minimize operational issues. One key principle is maintaining consistent air pressure and flow rates to prevent material buildup or blockages in the pipeline. This is achieved through the use of appropriate air compressors and flow control devices that ensure a steady supply of air to move the carbon black particles.
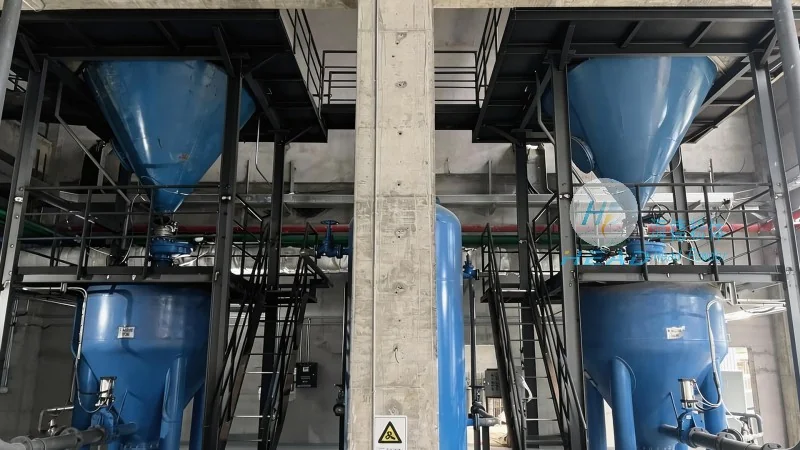
Another important design principle is the selection of suitable materials for the conveyor components. Carbon black is abrasive and can cause wear on metal surfaces, so components such as hoppers, pipelines, and valves are often made from corrosion-resistant materials like stainless steel or specialized alloys. This helps to extend the lifespan of the equipment and reduce maintenance costs.
Advantages of Using a Carbon Black Pneumatic Conveyor
Implementing a carbon black pneumatic conveyor offers several advantages over traditional methods of material handling. One major benefit is the ability to transport materials in a sealed system, which reduces dust emissions and improves workplace safety. This is particularly important in industries where carbon black dust can be a health hazard. Additionally, pneumatic conveyors can handle long-distance transport and multiple destinations, making them ideal for large-scale processing operations.
Applications of Carbon Black Pneumatic Conveyors
Carbon black pneumatic conveyors are used in a variety of applications across different industries. In the tire manufacturing industry, they are used to transport carbon black from storage to mixing facilities. In the plastics industry, they help to move carbon black into extrusion and molding equipment. In the printing and ink industry, they are used to convey carbon black for ink production. The versatility of these conveyors makes them suitable for a wide range of applications where fine particulate materials need to be handled efficiently.
Maintenance and Operational Considerations
Proper maintenance is essential to ensure the long-term performance of a carbon black pneumatic conveyor. Regular cleaning of the hopper and pipeline is necessary to prevent material buildup, which can lead to blockages and reduced efficiency. Additionally, checking the air compressor and flow control devices for proper operation is important to maintain consistent air pressure. HeadPowder recommends following a regular maintenance schedule to keep the conveyor in optimal condition and minimize downtime.
Conclusion
A carbon black material pneumatic conveyor is a vital piece of equipment for industries that rely on carbon black processing. By understanding its design principles and operational requirements, businesses can select and maintain the right system to improve efficiency, reduce costs, and ensure workplace safety. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., industrial facilities can benefit from advanced pneumatic conveying solutions that meet their specific needs.