With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Calcined ash material conveying is a specialized process in industrial material handling that focuses on the efficient transportation of calcined ash, a byproduct commonly generated from thermal power plants and other industrial combustion processes. This method is crucial for optimizing the handling and utilization of calcined ash, which can be repurposed in various applications such as construction materials, soil amendments, and industrial raw materials. The design of calcined ash conveying systems must address the unique properties of calcined ash, including its particle size, moisture content, and potential abrasive characteristics, to ensure safe and reliable operation.
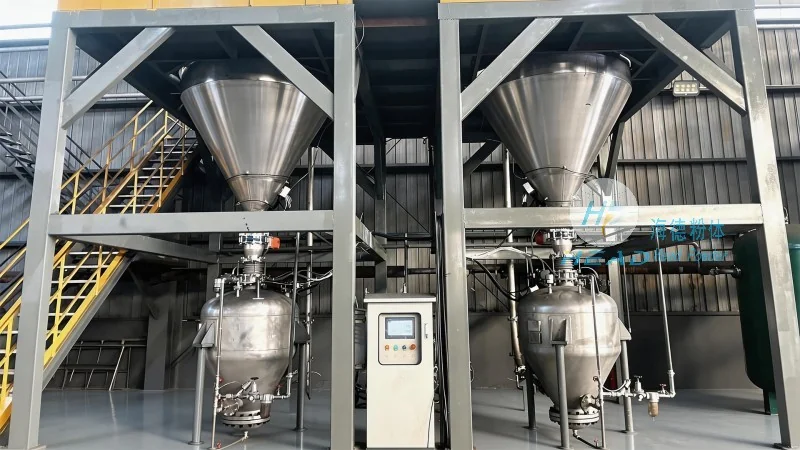
The design of calcined ash conveying systems is guided by several critical principles to ensure efficiency, safety, and durability. First, the system must be tailored to the specific characteristics of the calcined ash being handled. This includes considering the ash's particle size distribution, which can range from fine powders to coarse granules, and its moisture content, as excessive moisture can lead to caking or blockages in the conveying equipment. Second, the selection of conveying equipment is paramount. Common options include pneumatic conveying systems, which use air to transport the material, and mechanical conveying systems like belt conveyors or screw conveyors, which are suitable for bulk material handling. The choice depends on factors such as the distance to be covered, the volume of material, and the environmental regulations in the operating area.
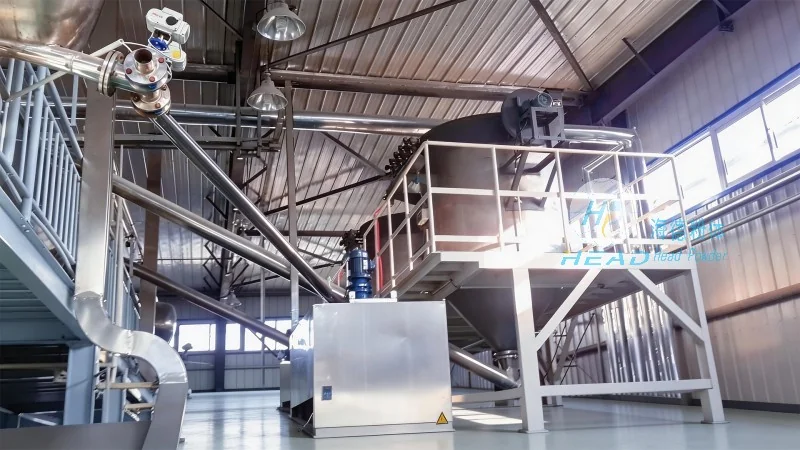
A typical calcined ash conveying system consists of several key components that work in tandem to ensure smooth operation. The primary components include the ash collection hopper, which collects the calcined ash from the source (e.g., a boiler or storage silo); the conveying equipment (such as a pneumatic pipeline or mechanical conveyor); and the discharge point, where the ash is delivered to its final destination. The ash collection hopper is designed to minimize dust emissions and prevent material buildup, often equipped with dust collection systems or sealing mechanisms. The conveying equipment must be robust enough to handle the abrasive nature of calcined ash, which can cause wear and tear on components over time. Regular maintenance and the use of wear-resistant materials in critical parts are essential to extend the system's lifespan and maintain performance.
The efficient conveyance of calcined ash offers several benefits to industrial operations. By streamlining the handling process, calcined ash can be transported to storage facilities, processing plants, or end-use applications with minimal downtime and operational costs. This not only improves the overall productivity of the facility but also enhances safety by reducing the need for manual handling of the material. Additionally, proper conveying systems help in reducing environmental impact by preventing dust emissions and ensuring that the ash is utilized in a controlled manner. For example, calcined ash can be used as a raw material in the production of cement or as a soil amendment to improve soil structure and fertility. The design of the conveying system plays a crucial role in enabling these applications by ensuring the material is transported in a consistent and manageable form.
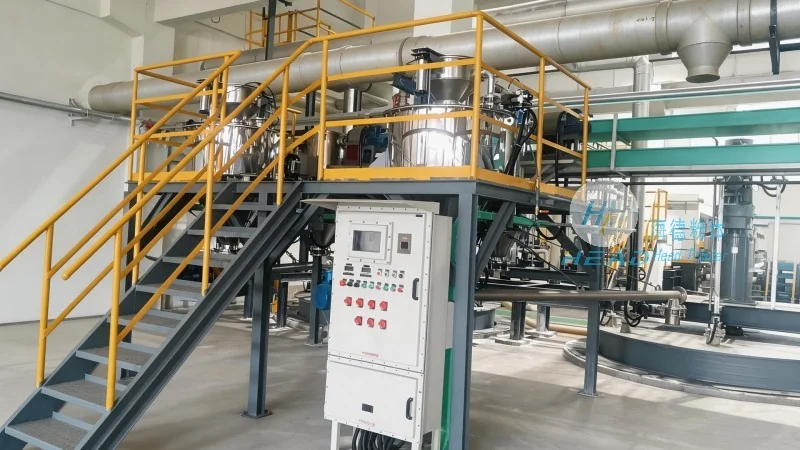
Shandong HeadPowder Engineering Co., Ltd. specializes in providing comprehensive calcined ash conveying solutions tailored to the unique needs of industrial clients. With years of experience in the field, HeadPowder understands the challenges associated with handling calcined ash and offers customized systems that address the specific requirements of each project. The company's team of engineers and technicians work closely with clients to assess their material handling needs, design efficient conveying systems, and provide ongoing support and maintenance. HeadPowder's solutions are designed to meet industry standards and regulatory requirements, ensuring that the calcined ash is handled safely and effectively. The company's commitment to quality and customer satisfaction has made it a trusted partner for many industrial facilities seeking reliable calcined ash conveying systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top