With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Coke material conveying lines are essential industrial systems designed to transport coke, a critical byproduct of the coking process, from production sites to various processing or storage locations. These systems are integral to the efficient operation of coke production facilities, ensuring that coke is moved safely, reliably, and in compliance with industry standards. The design and implementation of such lines involve careful consideration of material properties, operational requirements, and environmental factors to optimize performance and minimize downtime.
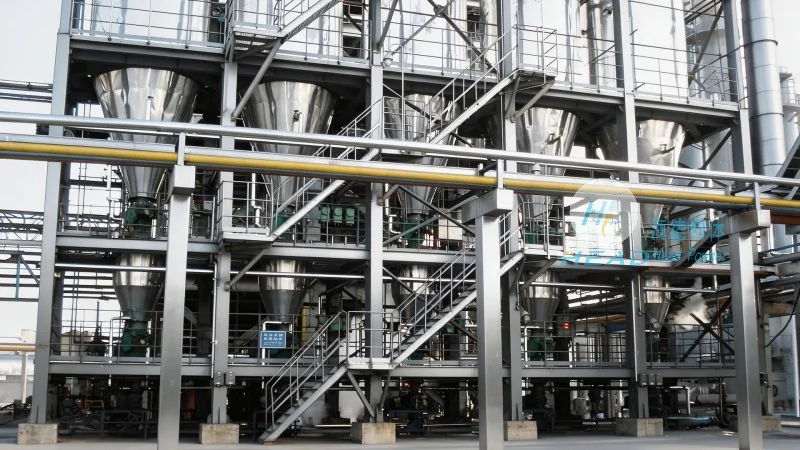
A typical coke material conveying line consists of several key components that work in tandem to ensure smooth material flow. These include:
Conveyors: Such as belt conveyors, screw conveyors, or bucket elevators, which are chosen based on the specific characteristics of the coke, including its size, moisture content, and bulk density.
Hoppers and Feeders: Used to store and control the flow of coke from storage silos or production areas into the conveyor system.
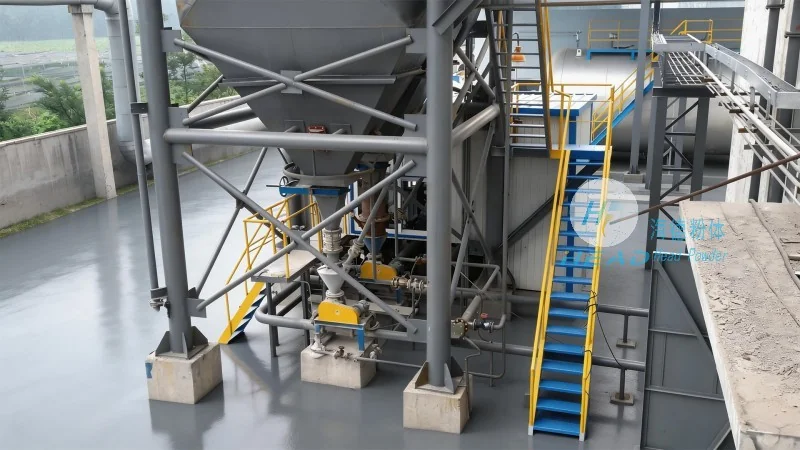
Dust Control Systems: Essential for managing dust emissions, as coke is a fine particulate material that can create health and safety hazards if not properly contained.
Control Panels and Sensors: Provide real-time monitoring and control of the conveying process, ensuring that the system operates within safe and efficient parameters.
The design of a coke material conveying line follows several core principles to maximize efficiency and reliability:
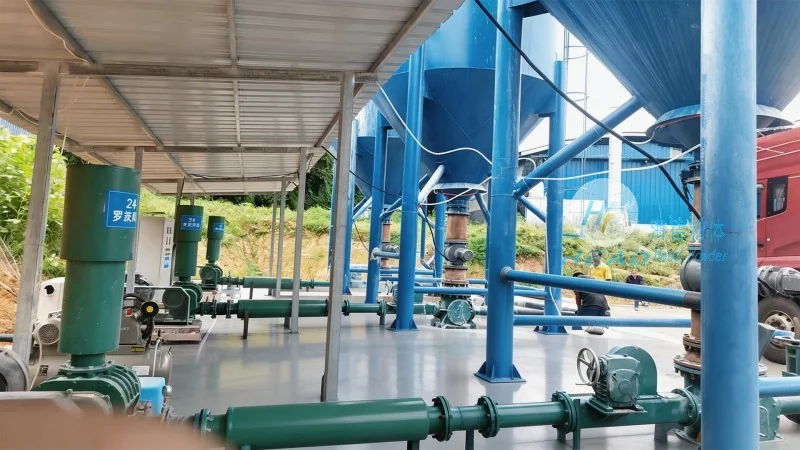
Material Compatibility: The system must be constructed from materials that are resistant to the chemical and physical properties of coke, such as high temperatures and abrasive particles.
Flow Optimization: Proper design of hoppers, chutes, and conveyor angles ensures that coke flows smoothly without blockages or segregation.
Safety and Environmental Compliance: Incorporating dust suppression systems, explosion-proof components, and proper ventilation is crucial to meet regulatory requirements and protect personnel.
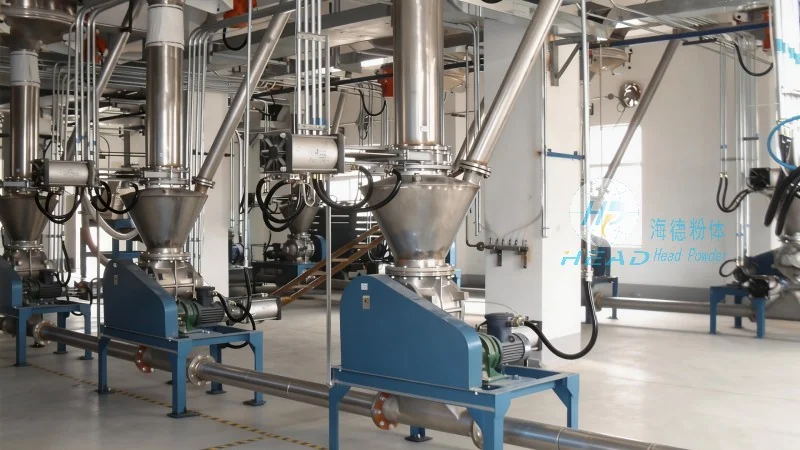
Scalability and Flexibility: The system should be designed to accommodate future expansions or changes in production volume, allowing for adaptability as the facility grows.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial conveying solutions, specializes in designing and manufacturing coke material conveying lines tailored to the unique needs of each client. With a strong focus on engineering excellence and customer satisfaction, HeadPowder leverages years of experience in the industry to deliver systems that meet the highest standards of performance and reliability. The company’s team of experts works closely with clients to understand their specific requirements, from material characteristics to operational constraints, and develops customized solutions that address all aspects of the conveying process.
In summary, coke material conveying lines are critical infrastructure in coke production facilities, and their design and operation are governed by principles that prioritize efficiency, safety, and compliance. By integrating advanced technology and expert engineering, companies like Shandong HeadPowder Engineering Co., Ltd. provide the solutions needed to ensure that coke is handled effectively and safely. The investment in a well-designed conveying system not only improves operational efficiency but also contributes to long-term sustainability and profitability in the coke industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top