With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Coal ash, a byproduct of coal combustion in power plants and industrial facilities, presents substantial challenges in handling and disposal. Traditional methods such as truck transport or belt conveyors often encounter issues like dust pollution, material loss, and operational inefficiencies. Pneumatic conveying offers a modern solution to transport coal ash efficiently and safely. This article explores the fundamental principles and working mechanisms of coal ash pneumatic conveying systems, highlighting how they revolutionize powder handling in industrial applications.
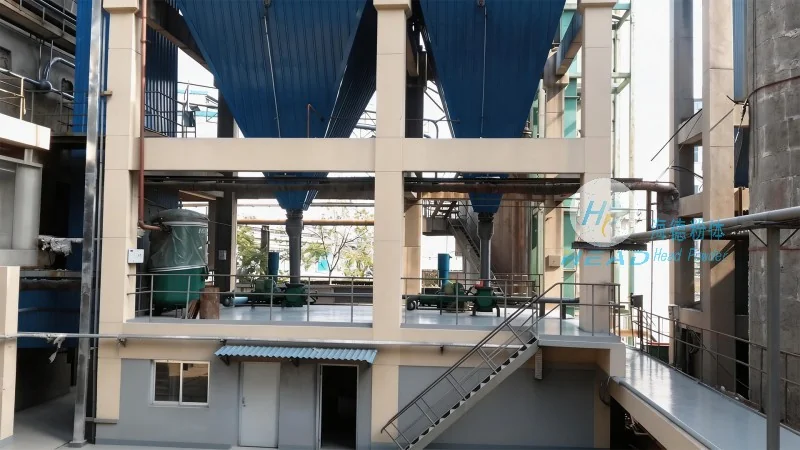
HeadPowder Engineering Co., Ltd. is a leading provider of advanced powder handling solutions, specializing in the design, manufacturing, and installation of pneumatic conveying systems. With a strong presence in Shandong, China, the company has established itself as a trusted partner for industries seeking reliable and efficient coal ash transport solutions. HeadPowder's expertise lies in customizing systems to meet specific operational requirements, ensuring optimal performance and minimal environmental impact.
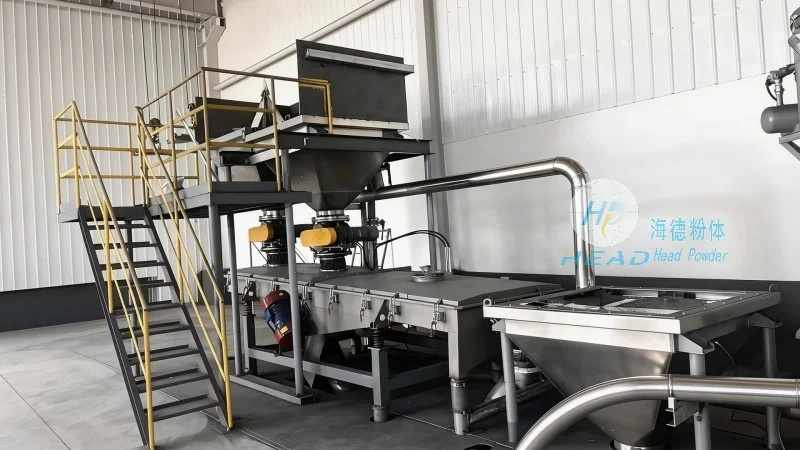
Pneumatic conveying systems utilize compressed air or gas to transport bulk materials like coal ash through a network of pipes. The process typically involves two main modes: dilute-phase and dense-phase conveying. In dilute-phase systems, the material is suspended in a high-velocity air stream, allowing for long-distance transport with minimal pressure drops. Dense-phase systems, on the other hand, use lower air velocities to form a dense slurry of material and air, reducing wear on equipment and improving material integrity. The system components include a hopper for material storage, a feeder to control the flow rate, a compressor to generate the air pressure, and a pipeline network connecting the source and destination points. The working process begins with the material being fed into the hopper, where it is then drawn into the pipeline by the air flow. The compressed air propels the coal ash through the system, ensuring smooth and continuous transport. At the receiving end, the material is deposited into a storage silo or processing unit, with the air being filtered and recycled back to the system.
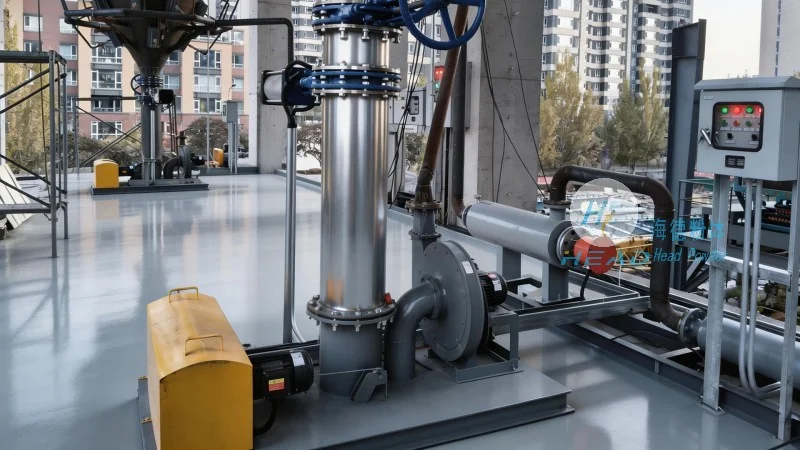
Compared to traditional transport methods, coal ash pneumatic conveying offers several key advantages. Firstly, it eliminates the need for heavy machinery and reduces labor costs by automating the transport process. Secondly, the enclosed system minimizes dust emissions, enhancing workplace safety and compliance with environmental regulations. Thirdly, the system can handle a wide range of particle sizes and moisture contents, making it versatile for various industrial applications. Additionally, pneumatic conveying systems are compact and can be installed in confined spaces, saving valuable floor space in industrial facilities. The efficiency of the system is further enhanced by the ability to control the flow rate and pressure, ensuring consistent material delivery to downstream processes.
Coal ash pneumatic conveying systems are widely used in power plants, cement factories, and other industrial facilities where large volumes of coal ash need to be transported. In power plants, the system efficiently conveys ash from boiler hoppers to storage silos or disposal sites. In cement plants, the ash is used as a supplementary cementitious material (SCM), and the conveying system ensures a steady supply of ash to the mixing and grinding units. The versatility of the system also makes it suitable for other applications, such as transporting ash from industrial furnaces or incinerators to treatment facilities. By integrating with existing infrastructure, the system can be customized to fit the specific needs of each facility, ensuring seamless operation and minimal disruption to production.
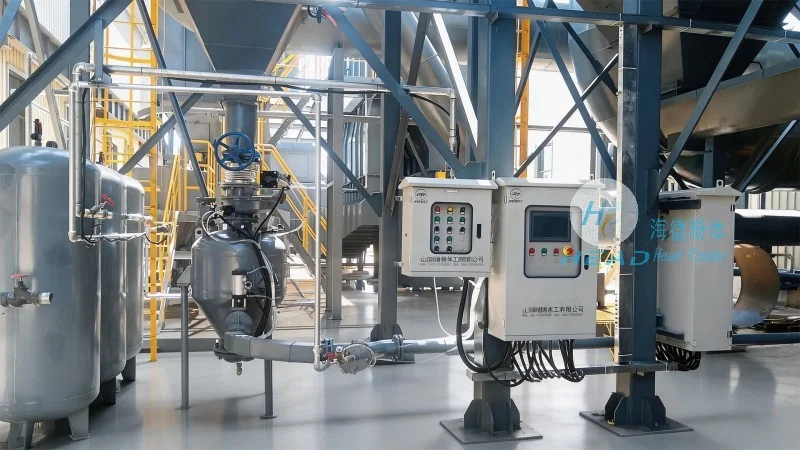
Coal ash pneumatic conveying represents a significant advancement in powder handling technology, offering efficient, safe, and environmentally friendly solutions for industrial applications. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., industries can leverage these systems to improve operational efficiency, reduce costs, and comply with environmental regulations. As the demand for sustainable and efficient material transport continues to grow, pneumatic conveying systems will play an increasingly important role in the future of industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top