With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a professional engineering company based in Shandong, China. The company specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems, particularly tailored for the transportation of potash fertilizer. With a strong focus on efficiency, reliability, and safety, headpowder has established itself as a leading provider in the fertilizer industry, delivering comprehensive solutions that meet the unique demands of modern potash fertilizer production and handling.
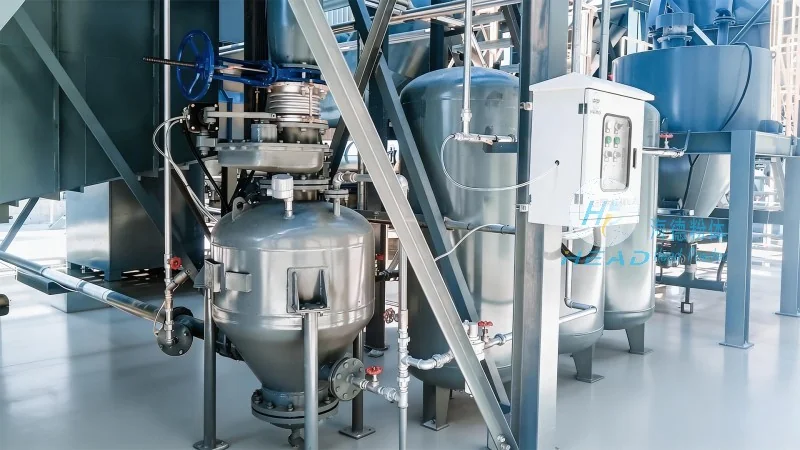
The potash fertilizer pneumatic conveying system is a sophisticated engineering solution designed to transport bulk potash fertilizer from storage silos, processing units, or production lines to storage facilities, packaging areas, or shipping points. This system utilizes air as the primary medium to move the solid fertilizer particles, eliminating the need for traditional mechanical conveyors and reducing operational costs associated with wear and maintenance. The system is engineered to handle various types of potash fertilizers, including muriate of potash (MOP), sulfate of potash (SOP), and other potassium-based fertilizers, ensuring compatibility with different chemical compositions and particle sizes.
The potash fertilizer pneumatic conveying system comprises several critical components, each contributing to its overall performance and reliability. The main components include a feed hopper, a rotary airlock valve, a conveying pipeline system, a dust collection unit, and a control panel. The feed hopper is designed to store and feed the potash fertilizer into the system at a controlled rate, preventing overloading and ensuring consistent flow. The rotary airlock valve acts as a seal between the hopper and the pipeline, preventing air leakage and maintaining the system's pressure. The conveying pipeline is typically made of high-quality materials such as stainless steel or corrosion-resistant alloys, which are resistant to the chemical properties of potash fertilizers and ensure long-term durability. The dust collection unit is integrated to capture and filter any airborne particles, maintaining a clean and safe working environment. The control panel allows operators to monitor and adjust the system's parameters, such as air pressure, flow rate, and temperature, ensuring optimal performance and preventing system failures.
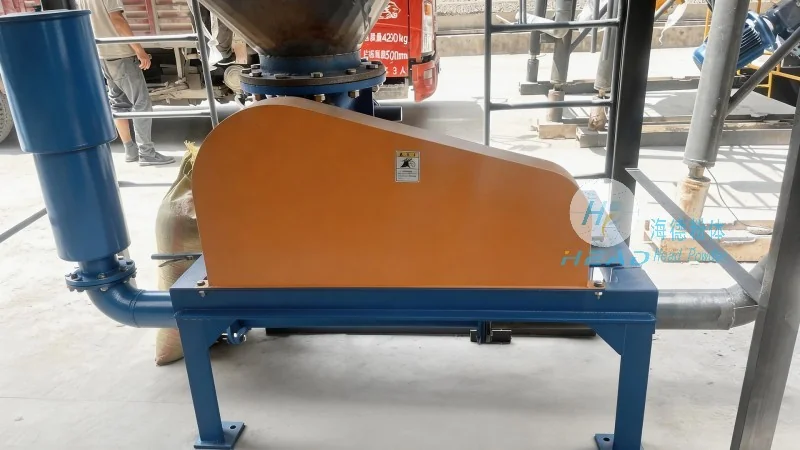
One of the primary advantages of the potash fertilizer pneumatic conveying system is its high efficiency in transporting bulk materials. By using air as the conveying medium, the system can move large quantities of potash fertilizer over long distances with minimal energy consumption. This reduces the need for multiple mechanical conveyors and reduces the overall footprint of the facility, making it an ideal solution for both new and existing potash fertilizer plants. The system also minimizes material loss and contamination, as the sealed pipeline prevents dust and moisture from entering or exiting the system. This not only improves product quality but also reduces waste and operational costs. Additionally, the system's modular design allows for easy expansion and modification, enabling companies to adapt to changing production needs without significant capital investment.
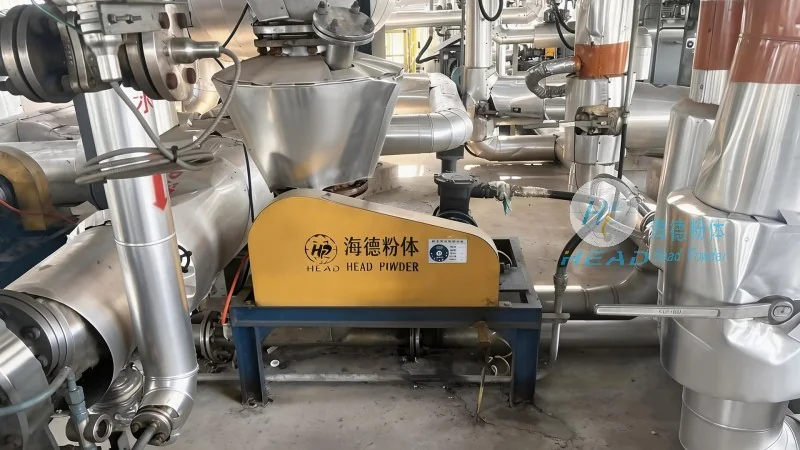
Reliability and safety are paramount in the potash fertilizer industry, and the pneumatic conveying system is designed with these considerations in mind. The system incorporates multiple safety features, including pressure relief valves, emergency shut-off switches, and automatic shutdown mechanisms in case of abnormal conditions. The use of corrosion-resistant materials and sealed components minimizes the risk of leaks and contamination, ensuring compliance with environmental regulations and industry standards. The system's control panel provides real-time monitoring of key parameters, allowing operators to detect and address issues promptly, preventing downtime and ensuring continuous operation. Furthermore, the system's low maintenance requirements reduce the risk of equipment failure and extend the lifespan of the components, resulting in lower long-term operational costs.
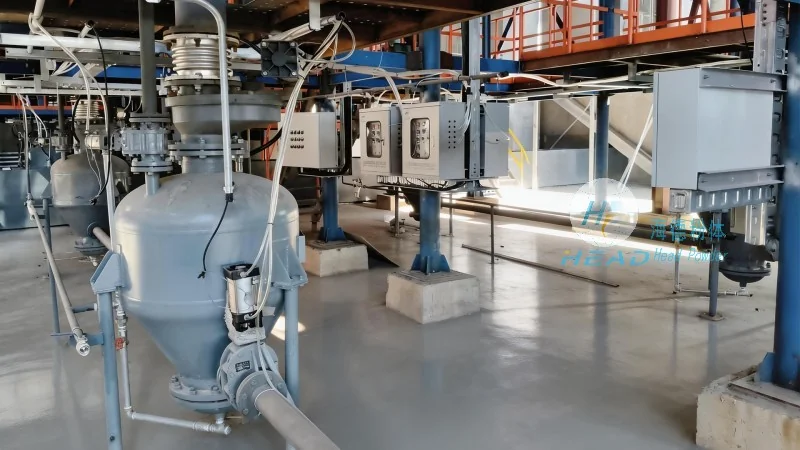
The potash fertilizer pneumatic conveying system is suitable for a wide range of applications in the fertilizer industry. It can be used in potash fertilizer production plants to transport raw materials from storage to processing units, or to move finished products from production lines to storage or packaging areas. The system is also ideal for fertilizer storage facilities, where it can transport potash fertilizer from storage silos to loading docks or shipping containers. Additionally, the system can be customized to meet the specific requirements of individual clients, including different conveying capacities, pipeline lengths, and material types. The engineering team at headpowder works closely with clients to understand their unique needs and design a system that is tailored to their specific application, ensuring optimal performance and satisfaction.
Shandong HeadPowder Engineering Co., Ltd. offers a comprehensive potash fertilizer pneumatic conveying system that combines advanced technology, efficient design, and reliable performance. The system is designed to meet the demanding requirements of the fertilizer industry, providing a cost-effective and sustainable solution for the transportation of bulk potash fertilizer. With its focus on efficiency, safety, and customization, the system is an ideal choice for companies looking to improve their production processes and reduce operational costs. As a leading provider in the industry, headpowder continues to innovate and develop new solutions to meet the evolving needs of the fertilizer market, ensuring that its clients remain competitive and successful in the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top