With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider in the field, specializes in advanced pneumatic conveying solutions tailored for rice grain handling. This technology has become increasingly vital in modern rice processing and logistics, offering efficient, dust-free, and hygienic methods for transporting rice from production sites to processing facilities and storage areas. The company, based in Shandong, China, leverages decades of experience to develop systems that meet the stringent requirements of the rice industry, ensuring high-quality transport while minimizing operational challenges.
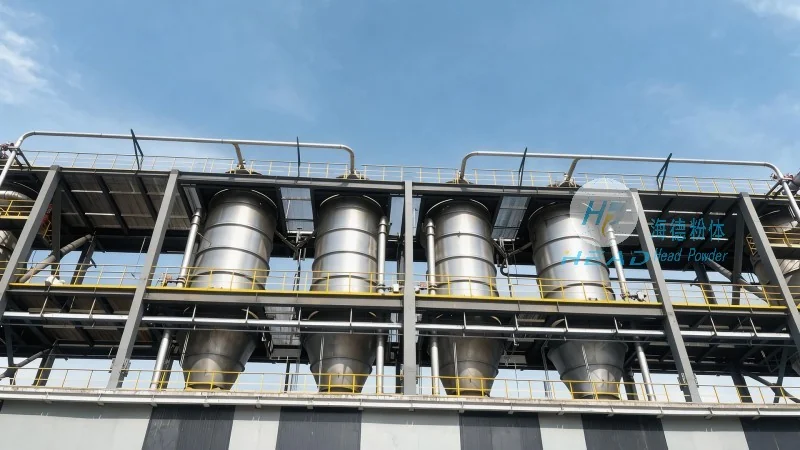
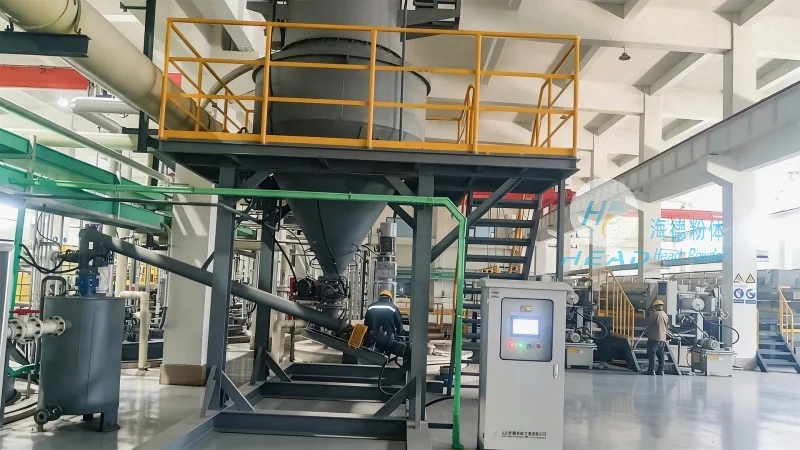
The core principle of pneumatic conveying involves using a pressurized or vacuum air stream to transport bulk materials like rice grains. In this system, rice particles are suspended and carried by the air flow, moving through pipelines. There are two main types: pressure and vacuum systems. Pressure systems use positive pressure to push the material forward, while vacuum systems use negative pressure to draw it. For rice grains, which are relatively light and have a certain density, the selection of system type depends on factors such as the distance of transport, the required flow rate, and the need for dust control. The design of the conveying system includes components like the hopper, feeder, pipeline, and receiver, all of which are optimized to minimize particle breakage and maintain product quality. The air velocity in the pipeline is critical; it must be high enough to keep the rice grains suspended but low enough to prevent excessive wear on the equipment and to avoid excessive energy consumption. Proper air filtration and cleaning are also essential to maintain system efficiency and prevent clogging from rice dust. The engineering approach at HeadPowder focuses on balancing these factors to deliver reliable and efficient conveying solutions.
Pneumatic conveying technology is widely applied in various stages of rice grain handling. In the milling process, after cleaning and sorting, rice grains are often conveyed to the milling machines. The system ensures that the grains move smoothly without contamination, maintaining the quality of the final product. During storage, rice grains can be transferred from silos or storage bins to processing lines or packaging units. This method is particularly useful in large-scale rice mills where multiple storage locations are involved. The technology is also used in the distribution phase, moving rice from processing plants to warehouses or directly to retailers. The benefits in these applications include reduced labor costs, improved safety (as there is no manual handling of bulk materials), and enhanced product hygiene, which is crucial for meeting food safety standards. Additionally, the system can handle different rice varieties and grades, allowing for flexible and efficient sorting and transfer processes. HeadPowder's solutions are designed to adapt to these diverse needs, providing customized systems that enhance operational efficiency across the entire rice supply chain.
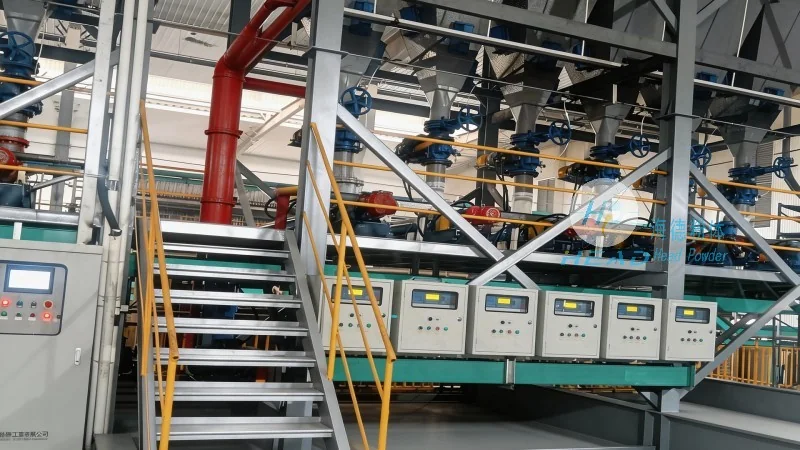
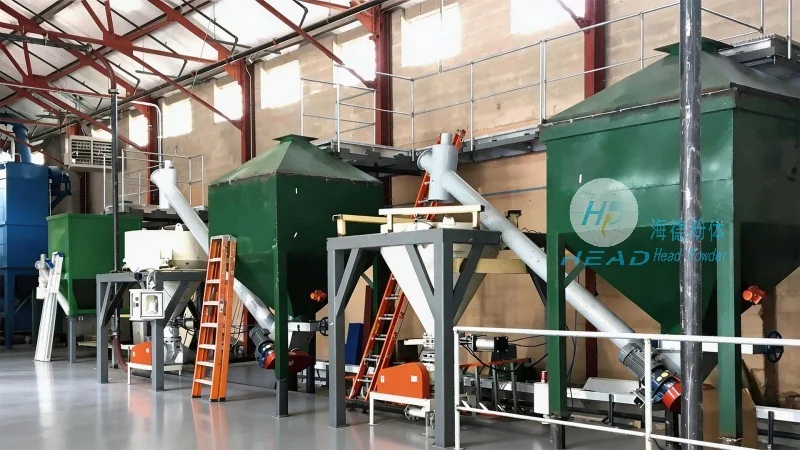
Over the years, the pneumatic conveying technology for rice grains has seen significant advancements. Modern systems now incorporate intelligent control systems that monitor air pressure, flow rate, and particle flow in real-time, allowing for automatic adjustments to optimize performance. This automation reduces operational costs and improves reliability. Material science has also played a role, with the development of more durable and corrosion-resistant pipeline materials, such as stainless steel and special alloys, which can withstand the abrasive nature of rice grains and the potential presence of moisture or chemicals in the environment. Energy efficiency has become a key focus, with the implementation of variable frequency drives (VFDs) to adjust motor speeds based on the conveying load, thus reducing energy consumption. Furthermore, research is ongoing to improve the system's ability to handle fine or broken rice particles, which are more challenging to convey due to their lower density and tendency to settle. Innovations in hopper design and feeder mechanisms are also being explored to enhance the uniformity of material flow and reduce the risk of blockages. The future of rice grain pneumatic conveying is likely to see more integration with digital technologies, such as IoT sensors and data analytics, to provide predictive maintenance and optimize operational efficiency. These developments aim to further enhance the reliability and sustainability of rice grain handling processes. HeadPowder is at the forefront of these advancements, continuously investing in research and development to offer cutting-edge solutions to its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top