What is a Gravity Dust Removal Material Pneumatic Conveying Machine? And What Are Its Design Princip
Industrial material handling systems often rely on efficient and reliable equipment to manage the movement of bulk materials. Among the various technologies available, pneumatic conveying systems have emerged as a versatile solution for transporting dry powders and granular materials. A specific type of such system is the gravity dust removal material pneumatic conveying machine, which combines the principles of gravity separation with pneumatic transport to enhance material handling efficiency. This article explores the functionality of this equipment and delves into its design principles, while also highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China.
Understanding the Gravity Dust Removal Material Pneumatic Conveying Machine
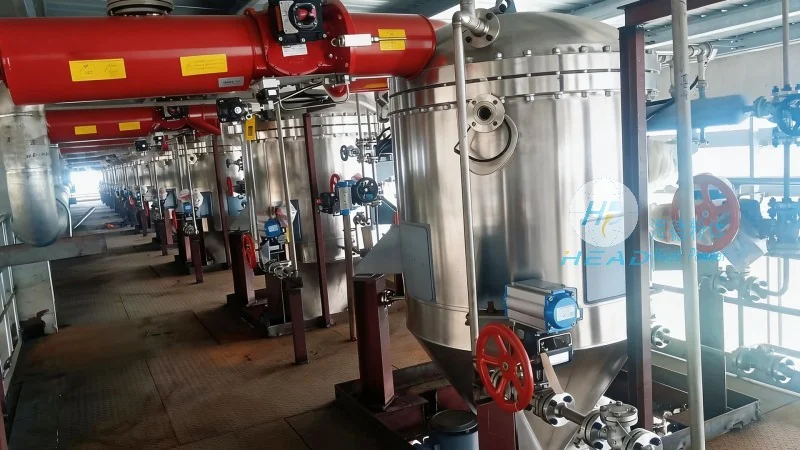
The gravity dust removal material pneumatic conveying machine is a specialized device designed to transport dry powders and fine particulate materials from one location to another using a combination of gravity and air pressure. Unlike traditional pneumatic conveyors that rely solely on air flow to move materials, this machine incorporates a gravity separation component that allows for the removal of dust and fine particles from the conveyed material stream. This separation process is crucial in industries where material purity and air quality are critical, such as in pharmaceuticals, food processing, and chemical manufacturing.
Key Components and Working Principle
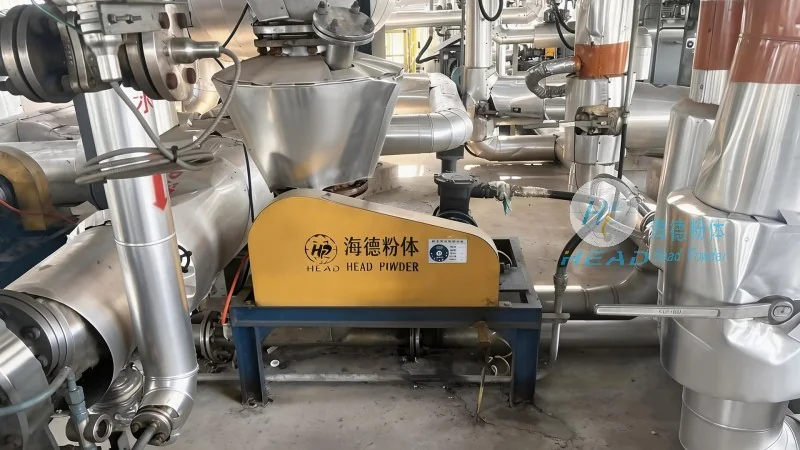
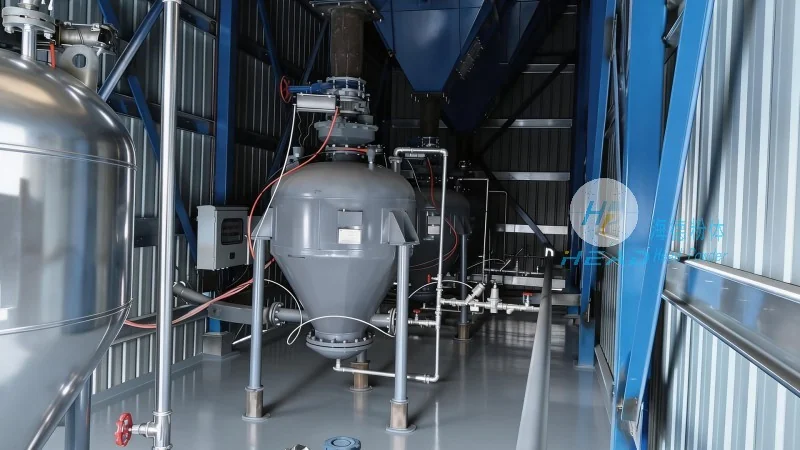
The operation of a gravity dust removal material pneumatic conveying machine involves several key components, each playing a vital role in the overall system. The primary components include a hopper for material storage, a conveying pipe system, a dust separator (often a cyclone or a bag filter), and a control system for regulating air flow and material movement. The machine works by first feeding the material into the hopper, where it is then introduced into the conveying pipe. As the material travels through the pipe, it is carried by a stream of air generated by a blower or fan. The air flow creates a low-pressure zone that pulls the material forward. Simultaneously, the gravity separation component, typically a cyclone separator, is integrated into the system to separate the fine dust particles from the bulk material. The dust is captured and removed from the air stream, while the larger, cleaner particles continue to be transported to the destination point.
Design Principles for Optimal Performance
The design of a gravity dust removal material pneumatic conveying machine is based on several critical principles to ensure efficient operation and minimal material loss. One of the fundamental principles is the balance between air velocity and material velocity. The air velocity must be sufficient to carry the material through the conveying pipe without causing excessive wear or degradation of the material. At the same time, the material velocity should be controlled to prevent the material from settling or clogging the pipe. Another key design principle is the proper sizing of the conveying pipe and the hopper. The pipe diameter and length are determined based on the material's properties, such as particle size, density, and flowability, to ensure smooth and continuous transport. The hopper design is also critical, as it must provide adequate storage capacity while maintaining a consistent feed rate to the conveying system. Additionally, the integration of the dust separator is a critical design consideration. The separator must be capable of effectively capturing fine particles without causing excessive pressure drop or energy consumption. The design also emphasizes energy efficiency, with the blower or fan sized appropriately to minimize power consumption while maintaining the required air flow rate.
Applications and Benefits in Industrial Settings
The gravity dust removal material pneumatic conveying machine finds wide applications across various industries due to its ability to handle fine powders and granular materials while maintaining high levels of material purity and air quality. In the pharmaceutical industry, for example, this equipment is used to transport active pharmaceutical ingredients (APIs) and other fine powders, ensuring that the material remains free from contamination and dust. In the food processing industry, it is used to transport ingredients like flour, sugar, and spices, maintaining the quality and safety of the final product. The chemical industry also benefits from this equipment, as it can handle hazardous powders and chemicals while preventing exposure to workers and the environment. The primary benefits of using this machine include improved material handling efficiency, reduced labor costs, and enhanced product quality. By separating dust from the material stream, the equipment also helps to maintain a clean and safe working environment, reducing the risk of respiratory issues and other health hazards associated with fine particulate exposure.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of industrial material handling equipment, including pneumatic conveying systems. The company is based in Shandong, China, and has established itself as a trusted provider of high-quality, reliable equipment for various industrial applications. HeadPowder specializes in designing and manufacturing custom pneumatic conveying solutions tailored to the specific needs of its clients. The company's products are known for their durability, efficiency, and adherence to industry standards. With a strong commitment to innovation and customer satisfaction, HeadPowder has built a reputation for delivering equipment that meets the highest performance and safety requirements. The company's team of experienced engineers and technicians work closely with clients to understand their material handling challenges and develop effective solutions that enhance operational efficiency and reduce costs. HeadPowder's facilities are equipped with state-of-the-art technology and quality control measures to ensure that every product meets the highest standards of performance and reliability.