

Principles and Application Scenarios of Dust-Free and Airtight Material Conveying
Efficient and safe material handling is a critical concern in industries where dust control and product purity are paramount. The principles of dust-free and airtight material conveying address these needs by ensuring that materials are transported without releasing particles into the environment. This method is particularly vital in sectors such as pharmaceuticals, food processing, and chemical manufacturing, where contamination risks can have severe consequences. By understanding the core principles and application scenarios of this technology, businesses can enhance operational safety and compliance with industry standards.
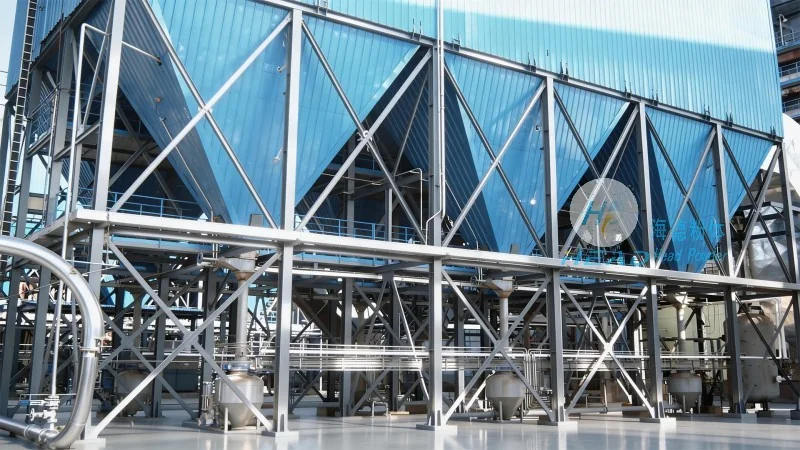
HeadPowder: A Leader in Engineering Solutions
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in providing advanced engineering solutions for material handling systems. With a focus on innovation and precision, HeadPowder has established itself as a trusted partner for companies seeking reliable and efficient conveying solutions. The company’s expertise lies in designing systems that meet stringent requirements for dust containment and operational efficiency, catering to diverse industrial needs.
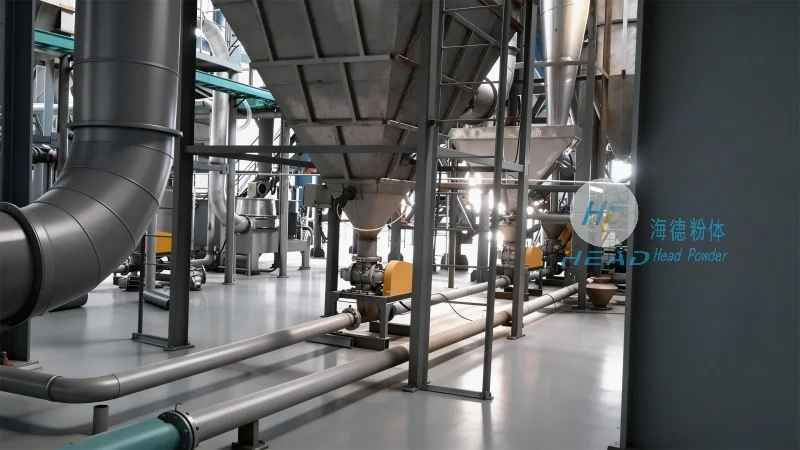
The Core Principles of Dust-Free Conveying
The foundation of dust-free and airtight material conveying lies in the integration of robust sealing mechanisms and controlled air flow. Key principles include the use of airtight hoppers, sealed conveyor lines, and positive pressure or vacuum systems to maintain a controlled environment. These systems prevent dust from escaping into the workspace while ensuring smooth material transfer. For instance, in pneumatic conveying systems, air is used to transport materials through a sealed pipeline, minimizing particle dispersion. Mechanical conveyors, such as screw or belt conveyors, are also equipped with dust-tight enclosures to contain particulates. The design emphasizes leak-proof connections and regular maintenance to sustain optimal performance.
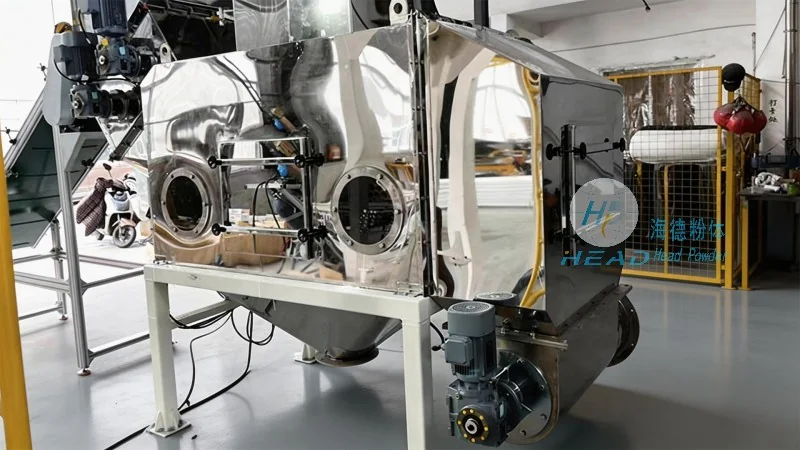
Application Scenarios: Where Dust-Free Conveying Makes a Difference
Dust-free and airtight material conveying is widely applied across various industries, each with unique operational demands. In the pharmaceutical industry, for example, the system ensures that active ingredients and finished products remain free from contamination, adhering to Good Manufacturing Practices (GMP). The sealed environment prevents cross-contamination and maintains product integrity throughout the conveying process. In food processing, similar principles are applied to handle powders like flour, sugar, or spices, ensuring that the final products are safe for consumption and free from allergens or impurities. The chemical industry also benefits from these systems when handling hazardous powders, as they prevent exposure to toxic substances and protect workers from inhalation risks.
Key Features and Advantages of HeadPowder's Solutions
HeadPowder’s dust-free conveying systems are equipped with several features that enhance performance and reliability. These include automatic cleaning mechanisms to prevent clogging, adjustable speed controls for precise material flow, and real-time monitoring systems to detect any deviations in pressure or flow. The company’s solutions are designed to be scalable, allowing businesses to adapt the system as their production needs evolve. Additionally, the use of high-quality materials, such as stainless steel and food-grade plastics, ensures durability and compliance with industry regulations. The result is a system that not only meets but exceeds the standards for dust containment and operational efficiency.
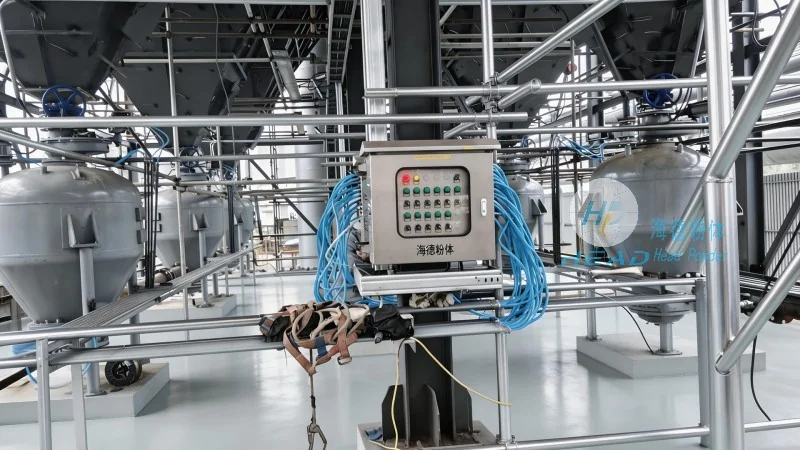
Conclusion: Enhancing Safety and Efficiency with Dust-Free Conveying
By implementing dust-free and airtight material conveying systems, industries can significantly improve their safety protocols and product quality. The technology not only reduces the risk of dust-related health issues but also minimizes environmental impact. As a leader in this field, Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide tailored solutions that address the specific challenges of each client. With a commitment to excellence and customer satisfaction, HeadPowder remains at the forefront of engineering solutions for modern material handling needs.