With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a prominent enterprise based in Shandong, China, specializes in the design, manufacturing, and supply of advanced pneumatic conveying equipment tailored for handling rare earth mineral powders. This article delves into the fundamental principles behind such equipment and highlights the key characteristics of its operational scenarios, providing a comprehensive understanding for potential users and industry stakeholders.
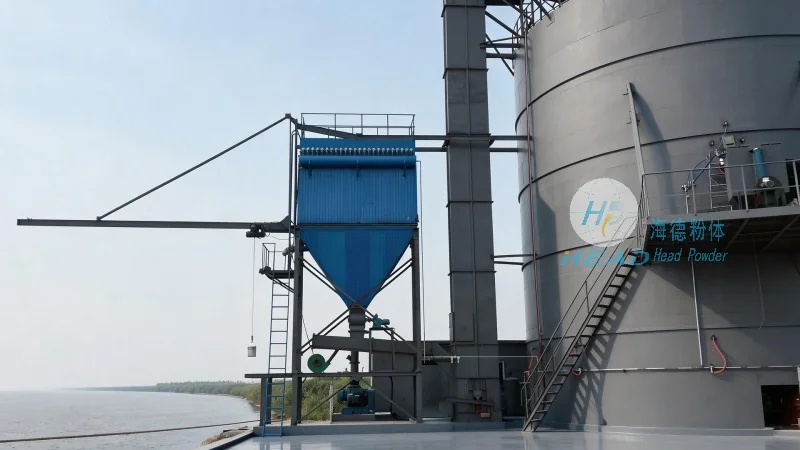
Pneumatic conveying systems utilize the force of compressed air or gas to transport bulk materials like rare earth mineral powders through a pipeline network. The core mechanism involves creating a pressure differential between the material source and the destination, enabling the powders to be suspended and carried by the moving air stream. For rare earth mineral powders, which often have specific handling requirements due to their chemical properties and particle size distribution, specialized equipment is essential to ensure efficient and safe transport. The system typically comprises a hopper for material storage, a blower or compressor to generate the air flow, a pipeline system for material transport, and a receiver or discharge unit for material collection. The selection of air velocity, pressure, and pipeline design is critical to prevent material degradation, blockages, or excessive energy consumption. HeadPowder's equipment is engineered to optimize these parameters, ensuring reliable performance for diverse rare earth mineral powder applications.
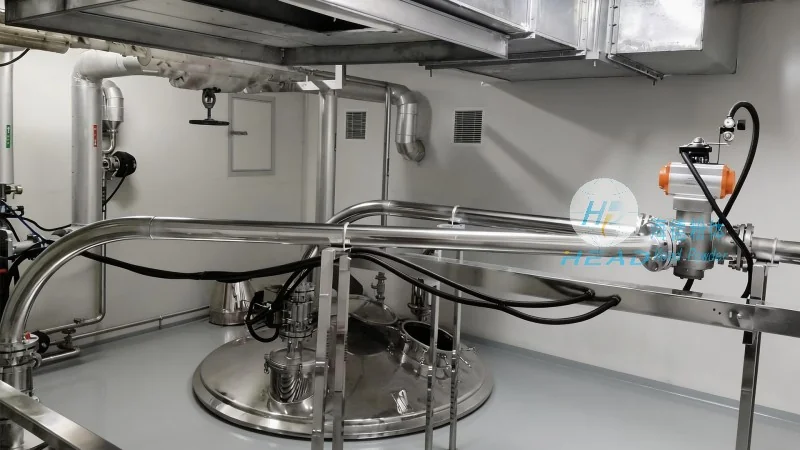
The operational scenarios for rare earth mineral powder pneumatic conveying equipment vary based on the specific industrial processes and material handling needs. Common applications include the transport of rare earth concentrates from mining sites to processing facilities, the movement of intermediate products between different stages of refining, and the delivery of finished rare earth compounds to storage or packaging areas. In these scenarios, the equipment must adapt to different material flow rates, particle sizes, and moisture content. For instance, in mining operations, the equipment may need to handle large volumes of raw ore with high moisture levels, requiring robust design to prevent clogging and maintain consistent air flow. In refining plants, the equipment must ensure precise control over the material's temperature and moisture to avoid chemical reactions or degradation during transport. HeadPowder's solutions are designed to address these varied requirements, offering flexibility in system configuration and material compatibility. The working scenes also involve considerations of space constraints, as industrial facilities often have limited room for large equipment installations. HeadPowder's compact and modular designs help accommodate such constraints while maintaining high efficiency and reliability. Additionally, the equipment operates in environments where safety and environmental compliance are paramount. The systems are equipped with features like dust collection and explosion-proof mechanisms to mitigate risks associated with handling potentially hazardous materials. These characteristics make the equipment suitable for a wide range of industrial settings, from small-scale processing plants to large-scale mining operations.
When evaluating pneumatic conveying equipment for rare earth mineral powders, several key features and advantages stand out. First, the ability to handle fine powders without causing agglomeration or loss of material is crucial. HeadPowder's equipment uses advanced air distribution and pipeline designs to maintain particle integrity, ensuring that the material reaches its destination in the desired form. Second, the system's energy efficiency is a significant advantage, as rare earth processing often involves high operational costs. By optimizing air flow and pressure, HeadPowder's solutions reduce energy consumption while maintaining high transport rates. Third, the equipment's durability and low maintenance requirements contribute to long-term cost savings. The use of high-quality materials and robust construction minimizes downtime and repair needs, making it a reliable choice for continuous industrial operations. Fourth, the flexibility in system integration allows for seamless incorporation into existing production lines. HeadPowder's equipment can be customized to fit various operational workflows, from batch processing to continuous flow, enhancing overall productivity. These features collectively make the equipment an ideal solution for industries dealing with rare earth mineral powders, offering both performance and economic benefits.
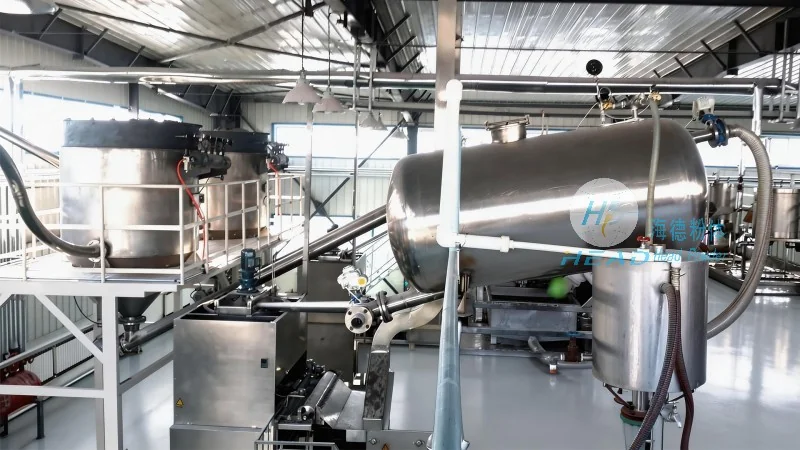
In conclusion, the pneumatic conveying equipment for rare earth mineral powders, as developed and supplied by HeadPowder, represents a sophisticated solution for efficient material handling in the rare earth industry. By understanding the fundamental principles of pneumatic transport and the specific characteristics of operational scenarios, users can leverage these systems to improve productivity, reduce costs, and ensure safe handling of rare earth materials. HeadPowder's commitment to innovation and quality ensures that their equipment meets the evolving needs of the industry, providing reliable and efficient solutions for a wide range of applications. As the demand for rare earth minerals continues to grow, the role of advanced conveying systems like these becomes increasingly vital in supporting industrial processes and maintaining competitiveness in the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top