What is a Protein Powder Material Pneumatic Conveying System? What Are Its Design Principles?
Protein powder, a key component in the food and supplement sectors, demands efficient and hygienic handling from production to packaging. The protein powder material pneumatic conveying system is a specialized solution engineered to meet these requirements, ensuring the safe and effective transport of this sensitive material. This article delves into the core aspects of such systems, exploring their design principles and the critical factors that make them suitable for protein powder applications.
Understanding Pneumatic Conveying Systems for Protein Powder
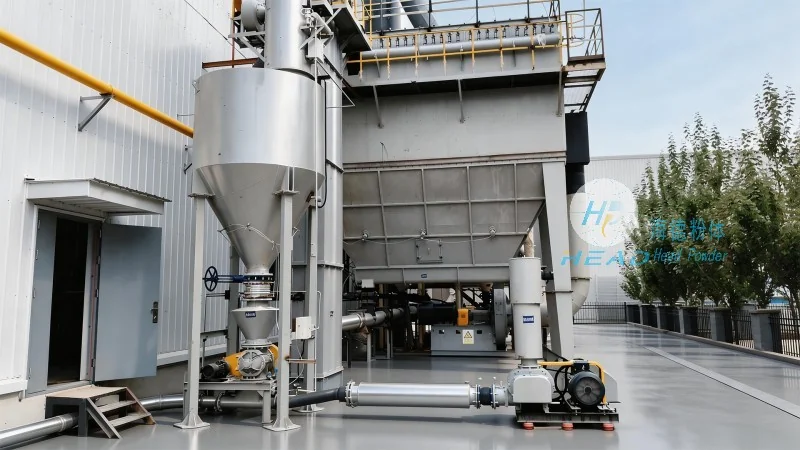
Pneumatic conveying systems utilize air or other gases to transport bulk materials like protein powder through a network of pipes. Unlike traditional mechanical conveying methods, which may introduce contamination or damage to the product, pneumatic systems provide a closed-loop, dust-free environment that preserves the quality and integrity of the powder. For protein powders—often sensitive to moisture, temperature, and physical stress—this is particularly vital. The system typically includes a hopper, conveyor line, and discharge unit, all connected by airtight piping to maintain product purity.
Key Design Principles for Protein Powder Conveying
The design of a protein powder pneumatic conveying system must adhere to several critical principles to ensure optimal performance and product quality. First, the system must maintain consistent air flow and pressure to prevent clogging or uneven material distribution. This is achieved through high-quality air compressors and flow control devices that regulate air volume and velocity within the pipes. Second, the materials used in system construction must be food-grade and corrosion-resistant, such as stainless steel, to avoid contamination and ensure longevity. Piping and components are often smooth and rounded to minimize friction and prevent powder residue accumulation, which could lead to bacterial growth or product degradation.
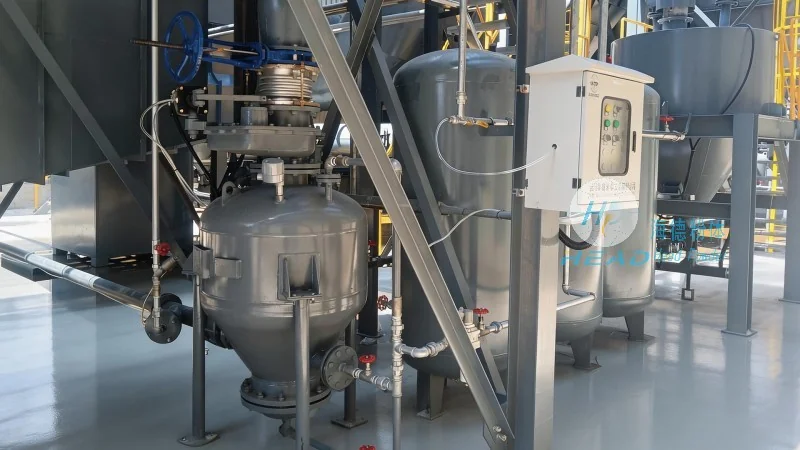
Third, the system must incorporate effective dust collection and filtration mechanisms. Protein powders are fine and can easily become airborne, posing health and safety risks if not properly contained. The design includes cyclone separators and bag filters that capture and retain powder particles, ensuring only clean air is released. This protects workers and maintains product purity by preventing cross-contamination from external sources.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading engineering firm based in Shandong, China, specializes in designing and manufacturing advanced pneumatic conveying systems for the food and pharmaceutical industries. With years of experience, the company has built a reputation for delivering high-quality, customized solutions tailored to protein powder manufacturers' specific needs. Their team of engineers and technicians collaborate closely with clients to understand production processes and material characteristics, ensuring the final system is both efficient and reliable.
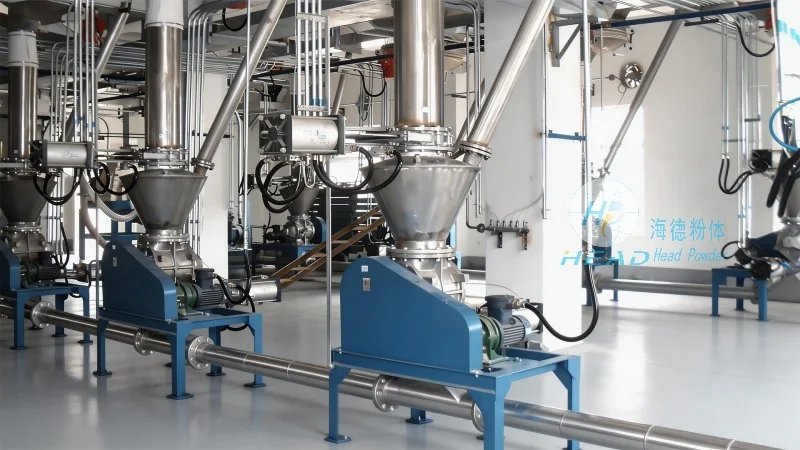
Application and Benefits in Protein Powder Production
The protein powder material pneumatic conveying system offers numerous advantages for manufacturers. By eliminating manual handling and traditional belt conveyors, it reduces labor costs and minimizes product contamination risk. The closed-loop design also improves operational efficiency by reducing downtime from maintenance and cleaning. Additionally, its ability to handle fine powders without clogging or degradation makes it ideal for high-volume production environments. For protein powders used in sensitive applications like infant formula or sports supplements, the system's hygienic design is crucial for meeting regulatory standards and maintaining consumer trust.
Conclusion
In summary, the protein powder material pneumatic conveying system is a sophisticated and essential component of modern protein powder production. Its design principles, centered on hygiene, efficiency, and product integrity, make it the preferred choice for manufacturers seeking to optimize operations. With companies like Shandong HeadPowder Engineering Co., Ltd. providing specialized solutions, the industry can rely on advanced technology to meet growing demand for high-quality protein powders while ensuring safety and compliance.