

What is a Multi-functional Material Handling Conveyor? And What Are Its Design Principles?
Multi-functional material handling conveyors are advanced industrial systems engineered to efficiently transport various types of materials within manufacturing, warehousing, and logistics environments. These versatile systems integrate multiple functionalities, such as sorting, stacking, and automated processing, to streamline material flow and enhance operational efficiency. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such sophisticated conveyor solutions tailored to meet diverse industrial needs.
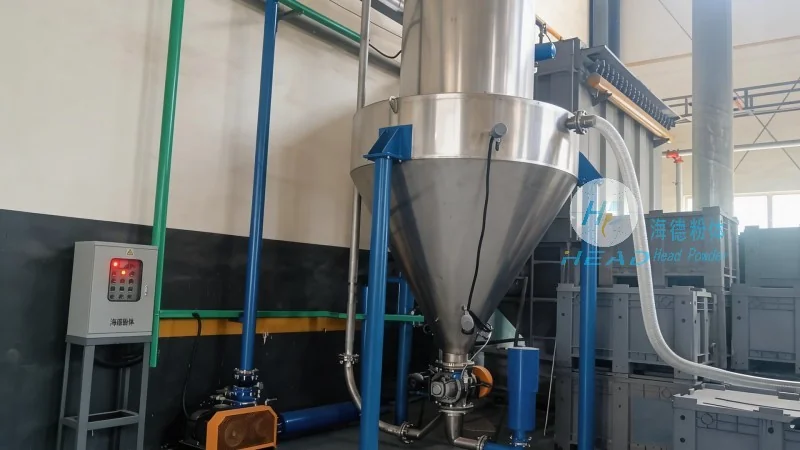
Understanding the Core Components of Multi-functional Material Handling Conveyors
At the heart of a multi-functional material handling conveyor lies a robust framework comprising several key components. These include motorized rollers or chains, control systems, sensors, and modular sections that can be customized for specific tasks. The motorized components enable precise movement and speed adjustments, while the control systems allow for automated operation and integration with other industrial equipment. Sensors are strategically placed to detect material presence, ensuring safe and efficient handling. Modular design is a critical feature, as it allows for easy reconfiguration and adaptation to changing production requirements.
Design Principles Behind Multi-functional Material Handling Conveyors
The design principles of multi-functional material handling conveyors prioritize flexibility, efficiency, and adaptability. Engineers at Shandong HeadPowder Engineering Co., Ltd. focus on creating systems that can handle a wide range of materials, from lightweight parts to heavy industrial components. The design incorporates load-bearing capabilities, ensuring durability under continuous operation. Additionally, the integration of sorting mechanisms, such as optical sensors or mechanical dividers, allows for automated material separation based on size, weight, or other characteristics. This enhances the overall efficiency of material processing and reduces manual intervention.
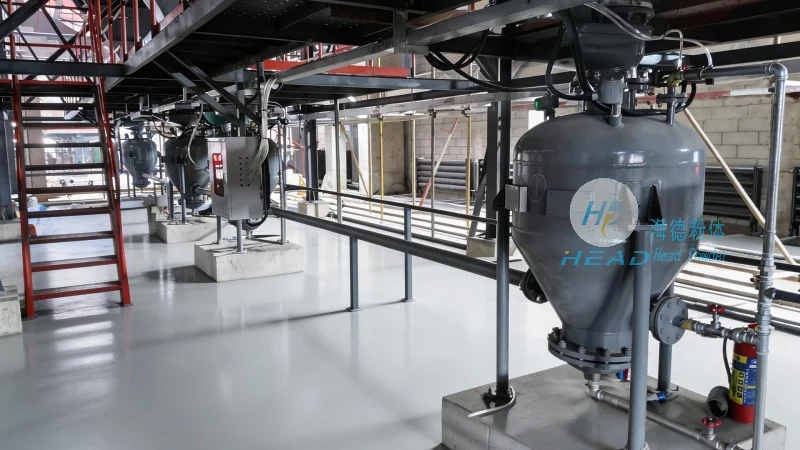
Customization and Application Flexibility
One of the standout features of multi-functional material handling conveyors is their ability to be customized for specific applications. Shandong HeadPowder Engineering Co., Ltd. works closely with clients to understand their unique operational needs and tailor the conveyor system accordingly. This may involve adding features like inclined sections for vertical transport, accumulation zones to prevent bottlenecks, or integrated labeling systems for traceability. The modular nature of these conveyors enables easy expansion or modification as production scales up or processes evolve. Such flexibility ensures that the system remains effective and efficient throughout its operational lifecycle.
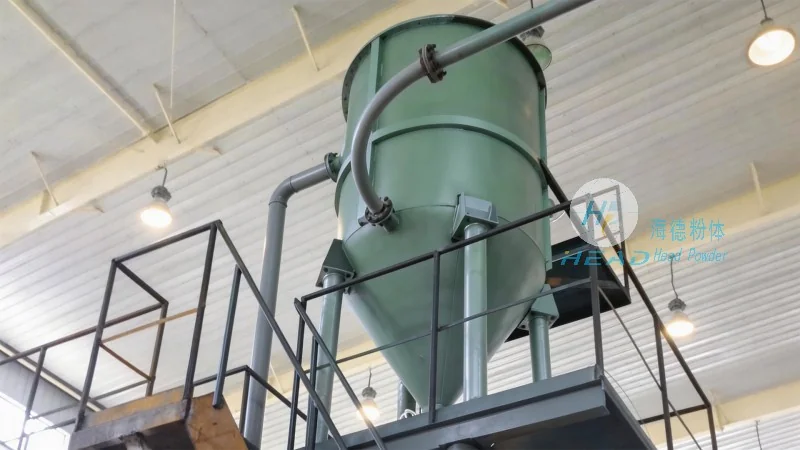
Enhancing Operational Efficiency and Productivity
By integrating multiple functions into a single conveyor system, multi-functional material handling solutions significantly enhance operational efficiency. The elimination of separate equipment for different tasks reduces floor space requirements and minimizes the need for manual handling, thereby lowering labor costs and improving safety. Automated sorting and processing capabilities enable faster material throughput, which is crucial in high-volume production environments. Furthermore, the consistent and reliable performance of these systems ensures that production lines operate smoothly without interruptions. This leads to increased productivity and reduced downtime, contributing to overall business success.
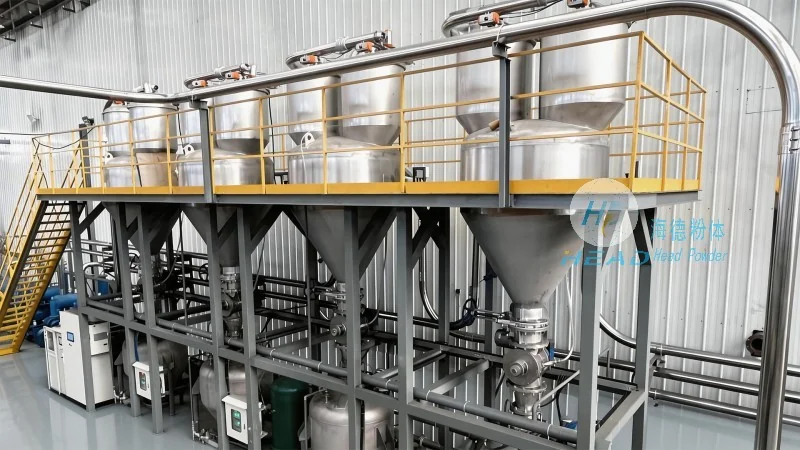
Reliability and Maintenance Considerations
Reliability is a paramount consideration in the design and operation of multi-functional material handling conveyors. Shandong HeadPowder Engineering Co., Ltd. employs high-quality materials and precision engineering to ensure long-term durability and minimal maintenance requirements. The modular design facilitates easy access to components for maintenance, reducing downtime during servicing. Regular maintenance schedules are recommended to keep the system in optimal condition, and the company provides comprehensive support, including technical guidance and spare parts availability. This focus on reliability ensures that the conveyor system delivers consistent performance over its operational life, providing a solid return on investment for clients.
Conclusion
Multi-functional material handling conveyors represent a sophisticated solution for modern industrial material transport needs. By combining multiple functionalities into a single, adaptable system, these conveyors enhance efficiency, reduce costs, and improve operational flexibility. Shandong HeadPowder Engineering Co., Ltd., with its expertise in engineering and manufacturing, offers tailored solutions that meet the diverse requirements of various industries. The design principles and components discussed highlight the advanced technology and thoughtful engineering behind these systems, making them essential tools for optimizing material handling processes. As industries continue to evolve, the demand for such versatile and efficient conveyor systems will only grow, underscoring their importance in modern manufacturing and logistics operations.