With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
When it comes to transporting chocolate powders and related products, selecting the right pneumatic conveying system is crucial for maintaining product quality, efficiency, and operational safety. Two primary methods dominate the industry: positive pressure and negative pressure systems. Understanding the differences between these approaches is essential for chocolate manufacturers to make informed decisions that align with their production needs. In this article, we explore the key characteristics of each system and provide guidance on how to choose the most suitable option for chocolate processing applications.
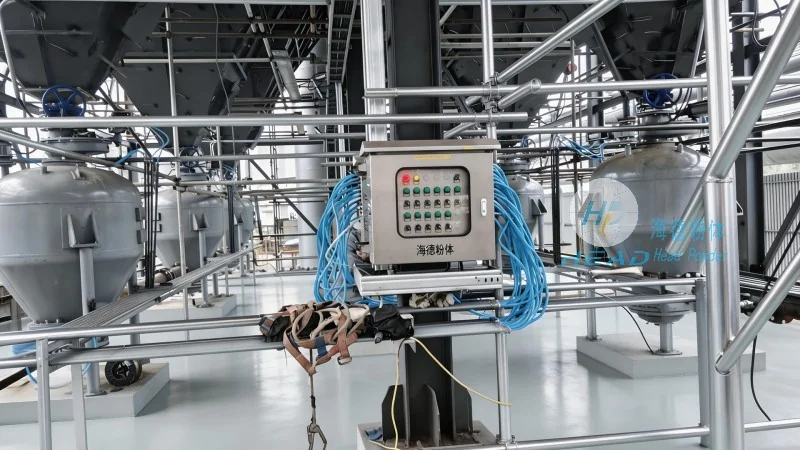
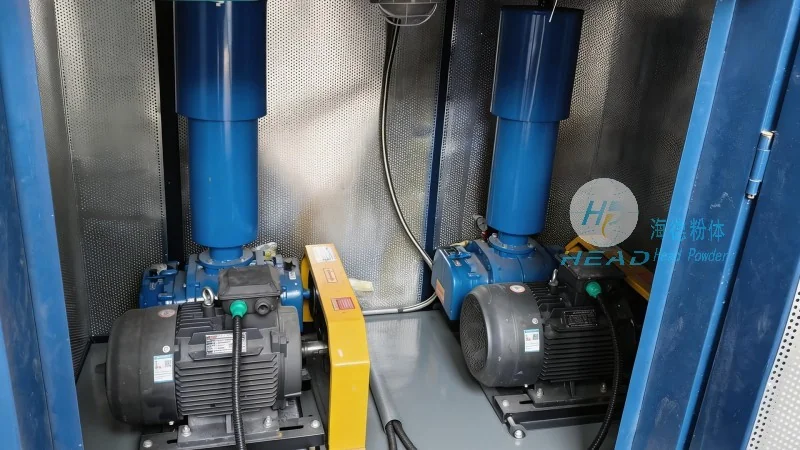
Positive pressure systems operate by blowing air or a carrier gas into the conveying line, creating a pressure higher than the ambient environment. This method is often preferred for chocolate applications due to its ability to handle abrasive materials and prevent product contamination. The headpowder system, as a leading provider in the field, offers advanced positive pressure solutions tailored for chocolate processing. These systems typically use a positive displacement blower or a rotary lobe pump to generate the necessary pressure, ensuring consistent material flow and minimal product degradation. The positive pressure approach is particularly effective for conveying chocolate powders over long distances or through complex piping networks, as it maintains a positive pressure throughout the system, reducing the risk of dust accumulation and product spillage.
HeadPowder’s positive pressure conveying systems for chocolate are designed with several key features that enhance performance and reliability. The systems utilize high-quality materials, such as stainless steel, to prevent corrosion and maintain hygiene standards required in food processing environments. The positive pressure design ensures that the chocolate remains in a sealed environment, minimizing exposure to contaminants and preserving its flavor and texture. Additionally, these systems are equipped with advanced control mechanisms that allow for precise regulation of air flow and pressure, ensuring optimal conveying efficiency. The positive pressure approach also facilitates easy integration with existing production lines, as it can be connected to existing ductwork and equipment without significant modifications. This makes it a versatile solution for chocolate manufacturers looking to upgrade or expand their conveying capabilities.
Negative pressure systems, on the other hand, work by creating a vacuum or negative pressure within the conveying line, drawing material from the source into the system. This method is often used for applications where the material is light and requires gentle handling. However, for chocolate powders, negative pressure systems may present challenges related to product quality and system maintenance. The headpowder engineering team has extensive experience in evaluating the suitability of negative pressure systems for chocolate applications, and our expertise can help manufacturers determine if this approach is appropriate for their specific needs. Negative pressure systems typically use a vacuum pump or a fan to create the necessary suction, and they are often more suitable for short-distance conveying or for materials that are less abrasive. The main advantage of negative pressure systems is their lower initial cost and simplicity, as they require less complex equipment compared to positive pressure systems. However, they may be less effective for handling large volumes of chocolate powders or for conveying materials over long distances, as the vacuum can lead to product degradation and increased energy consumption.
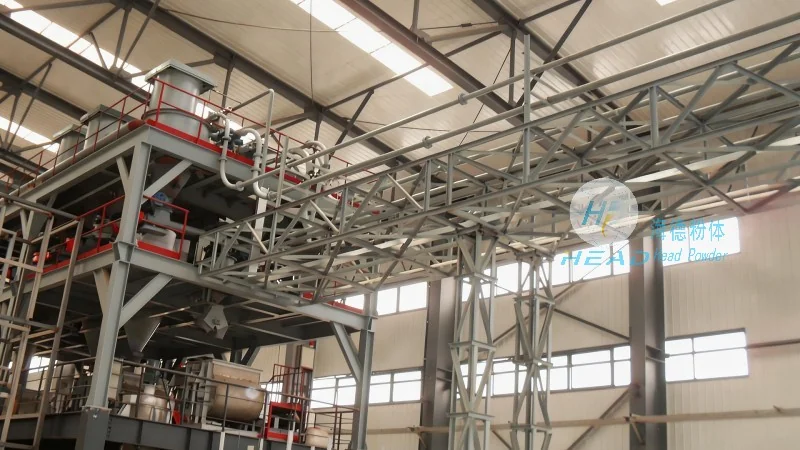
So, how can chocolate manufacturers distinguish between positive and negative pressure pneumatic conveying systems? The primary factor is the direction of air flow and the pressure differential within the system. Positive pressure systems push material through the line using compressed air, while negative pressure systems pull material using a vacuum. Another key difference is the impact on product quality. Positive pressure systems are generally better at preserving the texture and flavor of chocolate powders, as they minimize exposure to air and moisture. Negative pressure systems, while less expensive, may lead to increased product degradation due to the longer exposure time to the vacuum and potential for moisture absorption. Additionally, the maintenance requirements differ between the two systems. Positive pressure systems may require more frequent cleaning and maintenance to prevent dust buildup, while negative pressure systems may need more attention to prevent clogging and ensure consistent suction. The choice between positive and negative pressure systems also depends on the specific characteristics of the chocolate product, such as its moisture content, particle size, and flowability. Manufacturers should consider these factors, along with their production volume and budget, when selecting the most suitable conveying system.
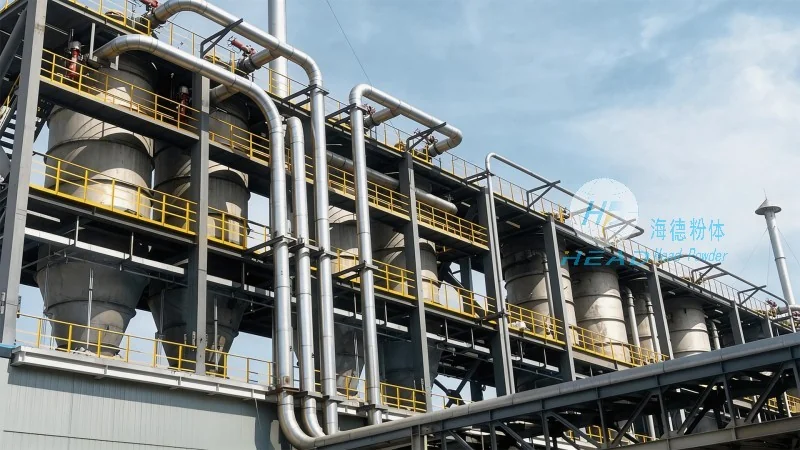
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of pneumatic conveying solutions for the chocolate industry. With years of experience and a commitment to quality, HeadPowder offers customized systems that meet the unique needs of chocolate manufacturers. Our team of engineers and technicians has extensive knowledge of both positive and negative pressure systems and can provide expert guidance on the most suitable approach for each application. We understand that chocolate powders require careful handling to maintain their quality, and our systems are designed with this in mind. Whether you need a positive pressure system for long-distance conveying or a negative pressure system for short-distance applications, HeadPowder can provide a solution that enhances your production efficiency and product quality. Our systems are built with high-quality components and are backed by comprehensive support services, including installation, maintenance, and technical assistance. We are committed to helping chocolate manufacturers achieve their production goals while maintaining the highest standards of product quality and safety.
Choosing between positive and negative pressure pneumatic conveying systems for chocolate is a critical decision that impacts production efficiency, product quality, and operational costs. By understanding the differences between these systems and considering the specific requirements of your chocolate processing operation, you can make an informed choice that maximizes performance and minimizes risks. HeadPowder’s expertise and advanced solutions provide chocolate manufacturers with the tools they need to succeed in their conveying needs. Whether you opt for a positive pressure system or a negative pressure system, our commitment to quality and customer satisfaction ensures that you receive a reliable and effective solution tailored to your specific requirements. Contact HeadPowder today to learn more about our chocolate pneumatic conveying systems and how we can help you optimize your production processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top