With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in the field of bulk material handling technology, specializes in the design, manufacturing, and implementation of intelligent pneumatic conveying systems. With a focus on innovation and precision, the company has established itself as a trusted partner for industries requiring efficient and reliable material transport solutions. HeadPowder's systems are engineered to meet the diverse needs of various sectors, including food, pharmaceuticals, chemicals, and industrial manufacturing, ensuring compliance with industry standards and operational excellence.
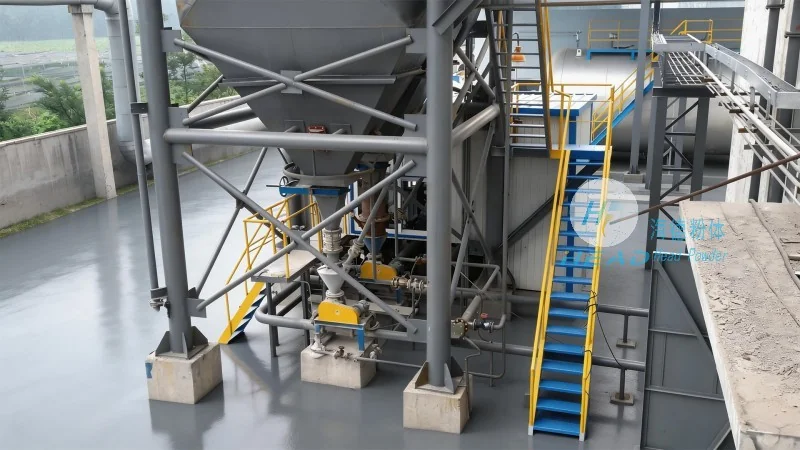
Pneumatic conveying systems utilize air or gas as the medium to transport bulk materials from one location to another. These systems are widely adopted due to their flexibility, ability to handle a wide range of materials, and minimal environmental impact compared to traditional mechanical conveyors. The core components of a pneumatic conveying system typically include a material hopper, a conveyor line, a control system, and a dust collection unit. The intelligent features integrated into modern systems enhance operational efficiency, safety, and data management capabilities.
The intelligent bulk material pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. incorporates several critical components that work in tandem to ensure smooth and efficient material transport. The material hopper is designed to store and feed the bulk material into the system, with features such as level sensors to monitor inventory levels and prevent overfilling. The conveyor line, which can be either positive or negative pressure based on the application, is equipped with high-efficiency air blowers that generate the necessary airflow to move the material. The control system, often integrated with advanced sensors and automation technology, monitors and adjusts the system parameters in real-time, optimizing performance and reducing energy consumption. Additionally, a dust collection unit is included to capture and filter any airborne particles, ensuring a clean and safe working environment.
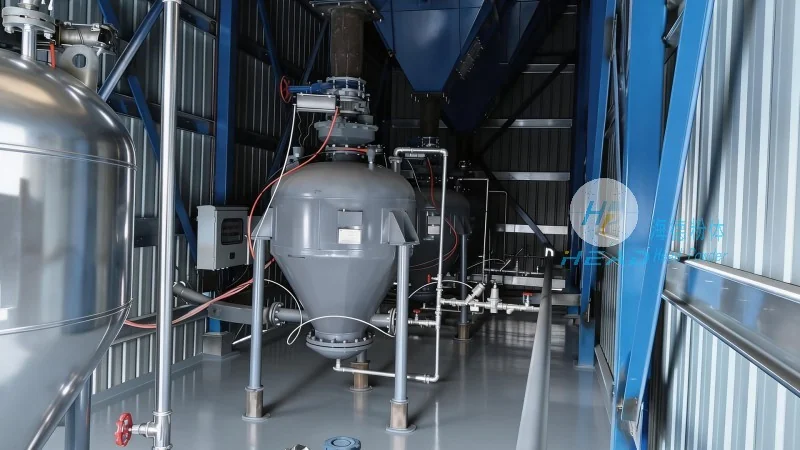
The operation of the intelligent bulk material pneumatic conveying system follows a systematic process that begins with material loading into the hopper. Once the material is ready, the control system activates the air blower, generating the required airflow. The material is then drawn from the hopper and conveyed through the pipeline to the discharge point. The system continuously monitors the pressure, flow rate, and material level, adjusting the airflow as needed to maintain consistent transport. Advanced sensors provide real-time data on system performance, allowing for immediate adjustments to optimize efficiency. The intelligent control module also includes safety features such as overload protection and automatic shutdown in case of abnormal conditions, ensuring operational safety and reliability.
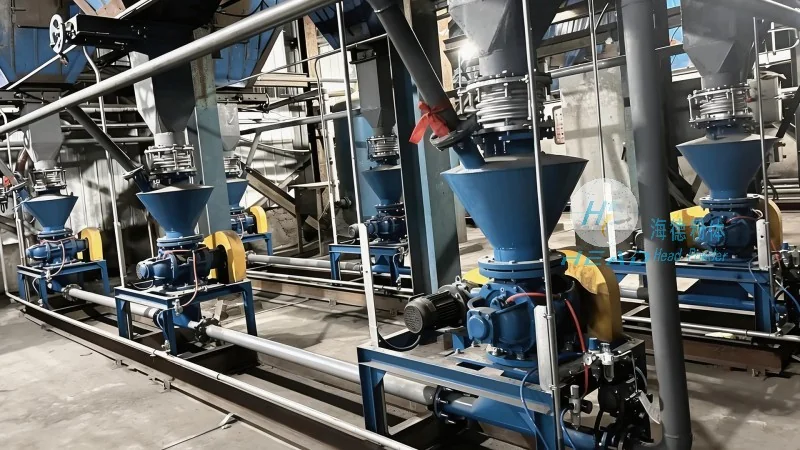
The working principle of the intelligent bulk material pneumatic conveying system is based on the fundamental physics of fluid dynamics and material transport. In a positive pressure system, the air blower pressurizes the air, which then carries the material particles through the pipeline. The air velocity is maintained above the material's terminal velocity to prevent settling and ensure smooth transport. The system uses a combination of air pressure and material flow dynamics to achieve efficient movement. In a negative pressure system, the air is drawn from the discharge end, creating a vacuum that pulls the material from the hopper. Both systems are designed to handle various material characteristics, including particle size, density, and moisture content, by adjusting the air flow rate and pressure. The intelligent features enhance the system's adaptability by allowing real-time adjustments based on material properties and operational conditions.
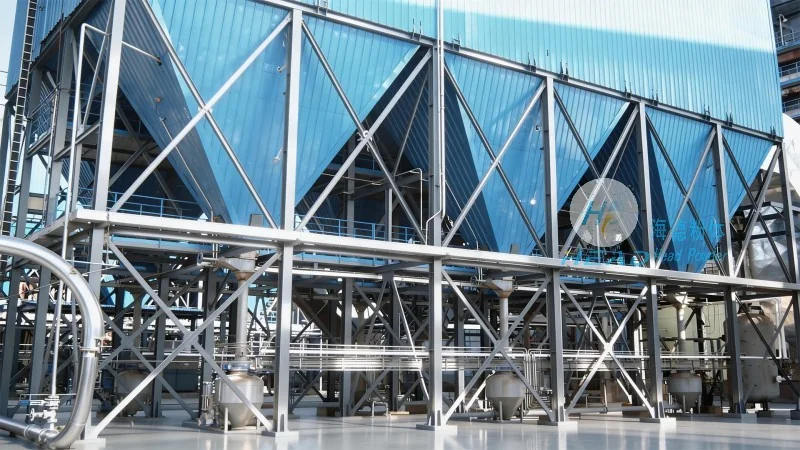
The intelligent bulk material pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. offers numerous benefits that make it an ideal choice for industries requiring reliable material transport solutions. The system's ability to handle a wide range of materials, including powders, granules, and bulk solids, makes it versatile for various applications. The intelligent control system enhances operational efficiency by optimizing energy usage and reducing downtime. The system also improves safety by incorporating features such as dust collection and automatic shutdown in case of emergencies. Additionally, the real-time monitoring and data logging capabilities provide valuable insights for maintenance and performance improvement. Industries such as food and pharmaceuticals benefit from the system's ability to maintain a clean and hygienic environment, while chemical and industrial manufacturing sectors appreciate the system's durability and adaptability.
Shandong HeadPowder Engineering Co., Ltd.'s intelligent bulk material pneumatic conveying system represents a significant advancement in bulk material handling technology. By integrating advanced automation, real-time monitoring, and intelligent control, the system ensures efficient, reliable, and safe material transport. With its ability to handle diverse materials and adapt to changing operational conditions, the system is a valuable asset for industries seeking to improve their material handling processes. The company's commitment to innovation and quality ensures that customers receive a robust and reliable solution tailored to their specific needs. As a leading provider in the field, HeadPowder continues to set new standards in bulk material conveying technology, delivering solutions that meet the evolving demands of modern industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top