What Are Sugar Material Handling Systems and Their Design Principles?
For businesses involved in the sugar industry, the efficient and reliable handling of raw materials and finished products is crucial for operational success. This article explores the components, functionality, and design principles of sugar material handling systems, highlighting how specialized equipment from Shandong HeadPowder Engineering Co., Ltd. can enhance productivity and safety in sugar processing operations.
Understanding Sugar Material Handling Systems
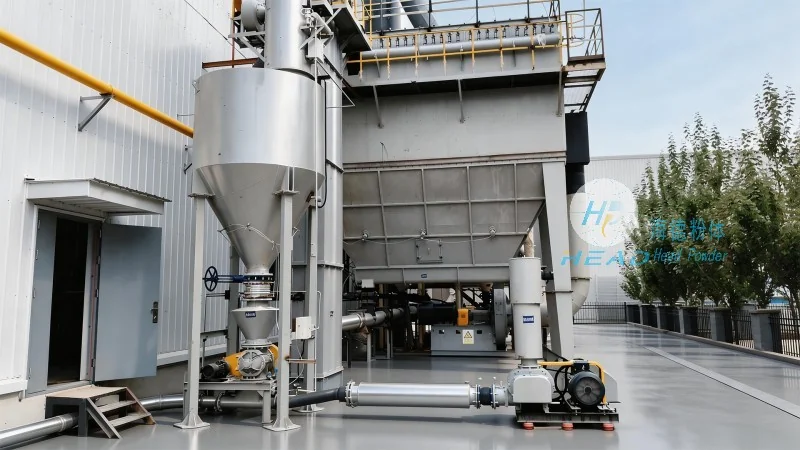
Sugar material handling systems are engineered to manage the flow of sugar from its raw form to final packaging. These systems integrate various equipment such as conveyors, elevators, and storage silos to ensure smooth and continuous processing. The primary goal is to minimize downtime, reduce labor costs, and maintain product quality throughout the handling process.
Key Components of a Sugar Material Handling System
At the core of any effective sugar handling system are several critical components. Conveyors, including belt and screw types, are commonly used to transport sugar in bulk. Elevators, like bucket or chain elevators, lift sugar vertically to different levels of the processing facility. Storage silos and hoppers are essential for storing raw sugar or intermediate products, ensuring a steady supply for downstream operations. Additionally, screening and cleaning equipment may be integrated to remove impurities, maintaining the purity of the sugar.
Design Principles for Optimal Performance
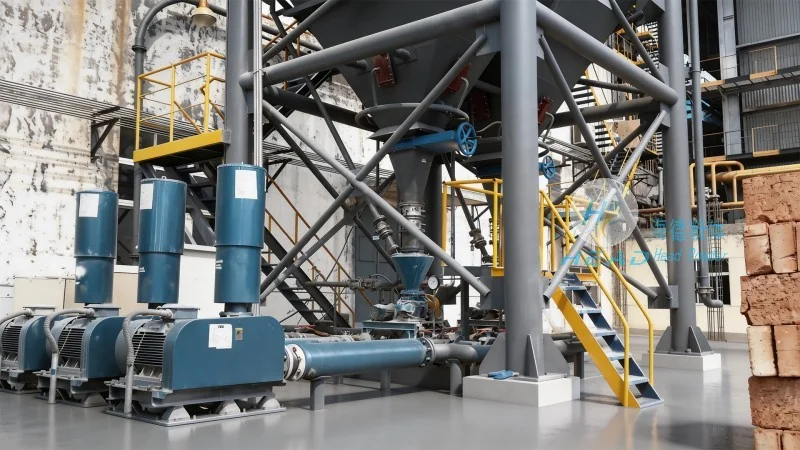
The design of a sugar material handling system must consider several factors to ensure efficiency and durability. Material compatibility is paramount, as sugar can be abrasive and sticky, requiring equipment made from materials like stainless steel or specialized plastics to prevent corrosion and blockages. The system's layout should be optimized for workflow, minimizing the distance between processing stages and reducing the risk of material spillage or contamination. Furthermore, the design must incorporate safety features, such as emergency stop mechanisms and enclosed systems, to protect operators and comply with industry regulations.
Role of Shandong HeadPowder Engineering Co., Ltd. in Sugar Handling Solutions
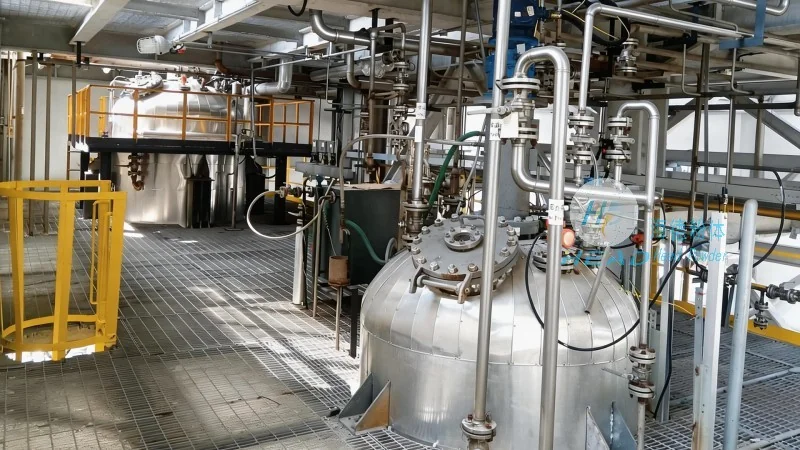
Shandong HeadPowder Engineering Co., Ltd., a leading provider of industrial engineering solutions, specializes in designing and manufacturing customized sugar material handling systems. With years of experience in the industry, the company understands the unique challenges of sugar processing, including the need for equipment that can handle high volumes of sugar while maintaining product integrity. Their systems are engineered to meet specific operational requirements, ensuring that clients receive tailored solutions that enhance productivity and reduce maintenance costs.
Benefits of Implementing Advanced Sugar Handling Systems
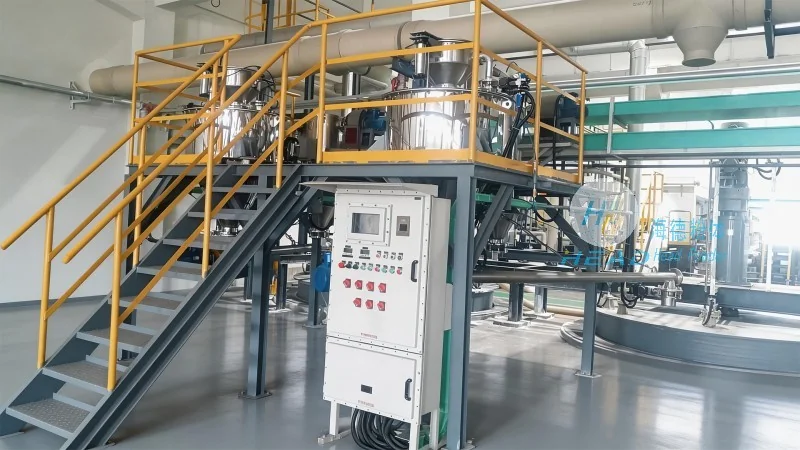
Investing in a well-designed sugar material handling system offers numerous benefits for sugar processing facilities. Improved efficiency through automated material movement reduces labor requirements and increases throughput. Enhanced product quality is achieved by minimizing handling-related damage and contamination. Additionally, the optimized layout of the system can free up floor space, allowing for better facility organization and potential expansion. From small-scale operations to large industrial plants, these systems provide a reliable foundation for consistent and high-quality sugar production.
Conclusion
Sugar material handling systems are essential for modern sugar processing facilities, combining advanced engineering with practical design to ensure efficient material flow. By understanding the key components and design principles, businesses can select or design systems that meet their specific needs. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in delivering these solutions, helping clients achieve operational excellence and maintain a competitive edge in the sugar industry.