With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Positive pressure powder conveying machines are essential equipment in the powder handling industry, designed to transport bulk powders efficiently and safely. As a leading manufacturer, Shandong HeadPowder Engineering Co., Ltd. specializes in providing high-quality solutions for various powder conveying applications. This article delves into the operation process and working principle of these machines, highlighting their key features and benefits.
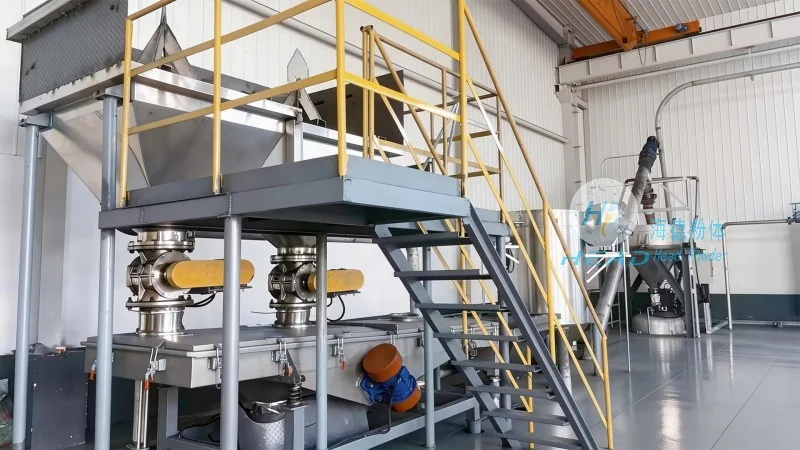
Positive pressure powder conveying systems utilize a pressurized air stream to move powders from a source to a destination. Unlike negative pressure systems, which rely on suction, positive pressure systems push the material forward, ensuring consistent flow and minimal product degradation. These machines are widely used in industries such as pharmaceuticals, food processing, chemicals, and mining, where precise and reliable powder transport is critical.
The core components of a positive pressure powder conveying machine include the hopper, conveyor tube, air compressor, control panel, and discharge outlet. The hopper is where the powder is loaded, and it features a smooth interior to prevent material buildup and ensure uniform flow. The conveyor tube is typically made of stainless steel or other corrosion-resistant materials to handle a variety of powders without contamination. The air compressor generates the necessary pressure to move the powder through the system, while the control panel allows operators to adjust parameters such as pressure, flow rate, and speed. The discharge outlet is where the powder is released at the destination, often equipped with a filter to prevent dust emissions.
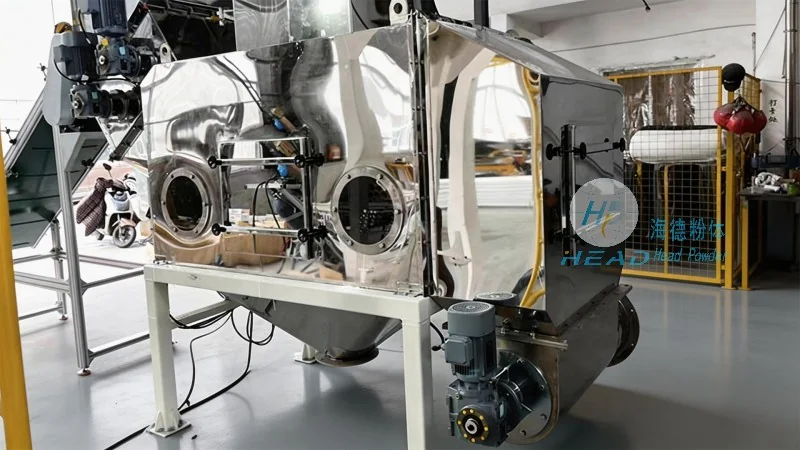
The operation process of a positive pressure powder conveying machine involves several steps, starting with the loading of the powder into the hopper. Once the hopper is filled, the air compressor is activated, creating a pressurized air stream that flows through the conveyor tube. The powder is then entrained by the air and carried forward to the discharge outlet. The speed of the air flow can be adjusted to control the conveying rate, ensuring that the powder is transported at the desired speed without causing excessive wear on the system components. The control panel allows operators to monitor and adjust these parameters in real-time, optimizing the conveying process for different powder types and application requirements.
The working principle of a positive pressure powder conveying machine is based on the principle of fluidization and entrainment. When the air compressor generates a high-pressure air stream, it creates a pressure differential between the hopper and the discharge outlet. This pressure differential causes the powder to be lifted and carried along the conveyor tube. The air flow rate is carefully controlled to ensure that the powder particles are fully entrained by the air, preventing blockages and ensuring smooth transport. The machine operates by continuously feeding the powder into the system and maintaining a consistent pressure and flow rate, which results in efficient and reliable powder transport.
Positive pressure powder conveying machines offer several advantages over other conveying methods. First, they provide a high conveying capacity, making them suitable for large-scale powder handling applications. Second, they are capable of transporting powders over long distances without the need for multiple transfer points. Third, they minimize product degradation by using gentle handling and avoiding high-speed impacts. Fourth, they are easy to clean and maintain, as the system components are designed for quick disassembly and reassembly. Finally, they are energy-efficient, as the air compressor can be adjusted to operate at the optimal pressure and flow rate for the specific application.
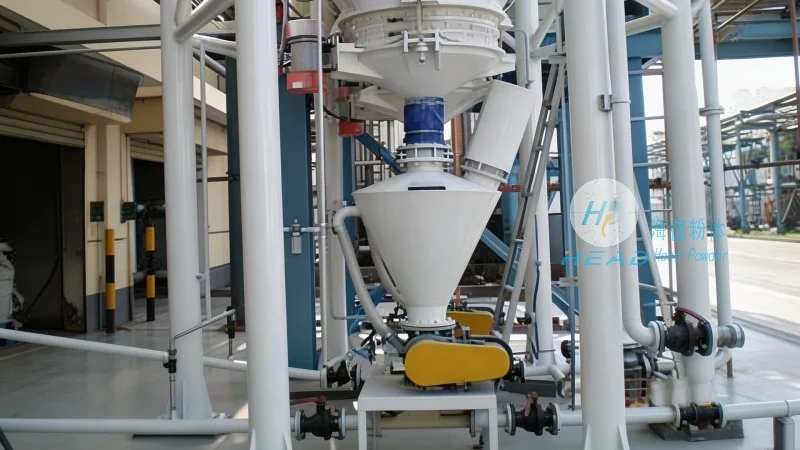
Positive pressure powder conveying machines are used in a wide range of applications, including the transportation of pharmaceutical powders, food ingredients, chemical powders, and mining products. In the pharmaceutical industry, these machines are used to transport active ingredients and excipients with high precision and minimal contamination. In the food processing industry, they are used to convey flour, sugar, and other food powders, ensuring that the products remain fresh and free from contamination. In the chemical industry, they are used to transport various chemical powders, such as pigments and catalysts, with high efficiency and reliability. In the mining industry, they are used to transport ore and other minerals from the mine to processing facilities, ensuring that the material is handled safely and efficiently.
Maintenance of a positive pressure powder conveying machine is crucial to ensure its long-term performance and reliability. Regular maintenance includes cleaning the hopper and conveyor tube to prevent material buildup, checking the air compressor for proper operation, and inspecting the control panel for any issues. Safety considerations are also important, as the machine operates at high pressures and can pose a risk of injury if not handled properly. Operators should wear appropriate personal protective equipment (PPE), such as gloves and safety glasses, and follow all safety guidelines provided by the manufacturer. Additionally, the machine should be inspected regularly for any signs of wear or damage, and any issues should be addressed immediately to prevent accidents.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top