With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider in the field of powder handling technology, specializes in the design, manufacturing, and application of dilute phase powder conveying systems. Based in Shandong, China, the company has established itself as a trusted partner for industries requiring efficient and reliable powder transport solutions. This article delves into the operation process and working principle of dilute phase powder conveying, highlighting the key components, operational dynamics, and the technical advantages that make such systems indispensable in modern industrial applications.
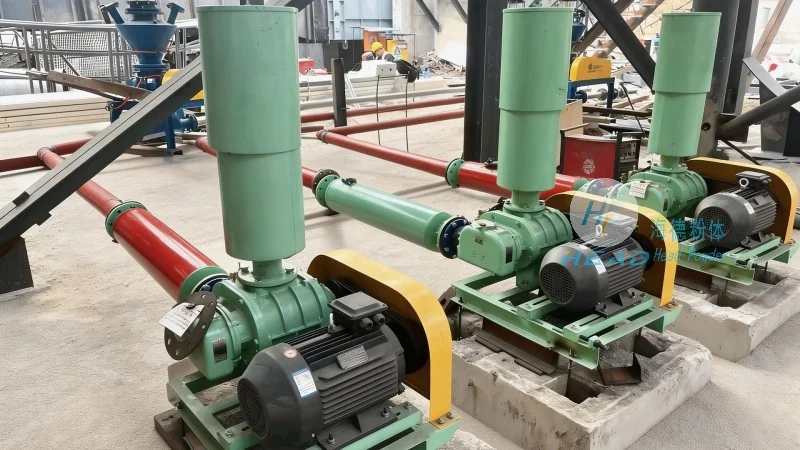
Dilute phase powder conveying is a method of transporting particulate materials through a pipeline using a high-velocity gas stream. Unlike dense phase conveying, where the material forms a plug and moves in a more compact manner, dilute phase systems rely on the suspension of particles in the gas flow. This approach is particularly suitable for long-distance transport and applications where the material needs to be transported at higher speeds with minimal pressure drop. The core principle involves creating a pneumatic conveying system where the powder is entrained by a high-pressure air or gas stream, ensuring that the particles remain suspended and travel through the pipeline efficiently.
A typical dilute phase powder conveying system consists of several critical components that work in tandem to ensure smooth operation. The primary components include a material feeder, a compressor or blower, a pipeline system, and a receiver or discharge unit. The material feeder is responsible for feeding the powder into the system at a controlled rate, ensuring a consistent flow. The compressor or blower generates the necessary pressure and velocity to entrain the particles. The pipeline system, often made of stainless steel or other corrosion-resistant materials, transports the powder and gas mixture. The receiver or discharge unit collects the material at the end of the pipeline, separating it from the gas and returning the gas to the system for reuse or venting.
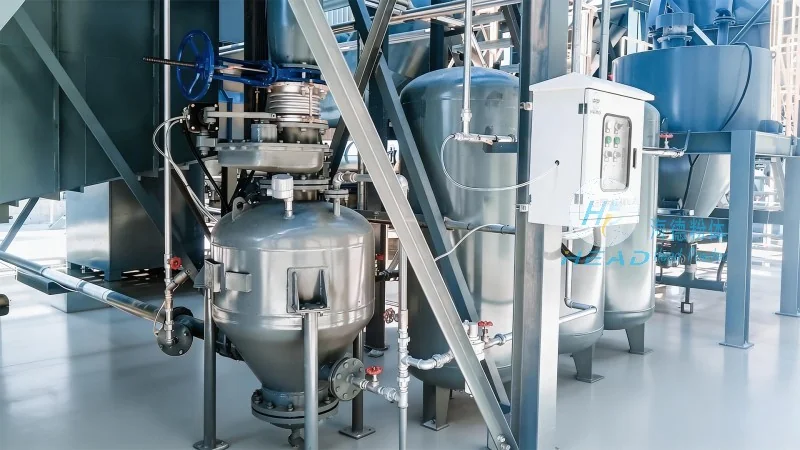
The operation of a dilute phase powder conveying system follows a systematic process. Initially, the material feeder introduces the powder into the pipeline at a predetermined rate. Simultaneously, the compressor or blower supplies high-pressure air or gas, which creates a high-velocity flow within the pipeline. As the gas moves through the pipe, it entrains the powder particles, forming a dilute mixture. The mixture travels through the pipeline, maintaining the particles in suspension due to the high velocity and turbulence. At the receiving end, the mixture is directed into a receiver where the gas is separated from the powder. The gas may be filtered and recirculated, while the powder is collected and discharged. This cycle repeats as material is continuously fed and transported.
The working principle of dilute phase powder conveying is rooted in fluid dynamics and particle mechanics. The key is to achieve a sufficient gas velocity to overcome the gravitational and drag forces acting on the particles. The gas flow must be high enough to keep the particles suspended, preventing them from settling and clogging the pipeline. The pressure drop along the pipeline is a critical factor, as it determines the energy required to transport the material. Efficient design of the system minimizes pressure drop while maintaining the necessary velocity to ensure stable conveying. The system also considers factors such as particle size, density, and moisture content, as these properties affect the conveying characteristics and the required gas velocity.
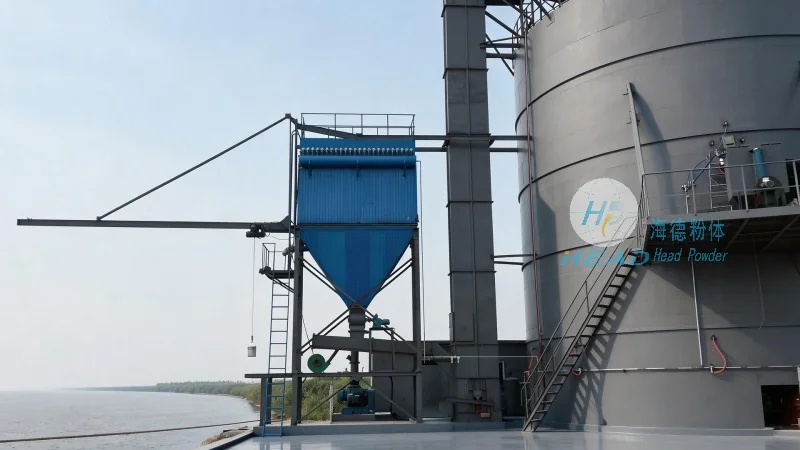
Dilute phase powder conveying offers several advantages that make it a preferred choice for many industries. It is capable of transporting materials over long distances with relatively low energy consumption compared to other methods. The system is also flexible, allowing for changes in material feed rate and pipeline configuration. Industries such as cement, pharmaceuticals, food processing, and chemical manufacturing widely use dilute phase systems for transporting powders like cement, flour, and various chemicals. The technology ensures minimal product degradation, as the particles are not subjected to high shear or pressure, preserving their quality and properties.
HeadPowder's expertise in dilute phase powder conveying systems reflects a deep understanding of the operational processes and working principles involved. By leveraging advanced engineering and material handling technologies, the company provides tailored solutions that meet the specific needs of various industries. The efficient and reliable operation of dilute phase conveying systems, as described, underscores the importance of proper design, component selection, and operational management. For businesses seeking to enhance their powder transport capabilities, HeadPowder offers comprehensive solutions that ensure optimal performance and longevity of the conveying systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top