

Principle and Working Scene Characteristics of Nitrogen-Protected Pneumatic Conveying Systems
Shandong HeadPowder Engineering Co., Ltd., commonly known as Headpowder, is a professional manufacturer and supplier based in Shandong, China. The company specializes in the design, development, and implementation of advanced pneumatic conveying systems, with a particular focus on nitrogen-protected solutions that ensure the integrity and quality of conveyed materials.
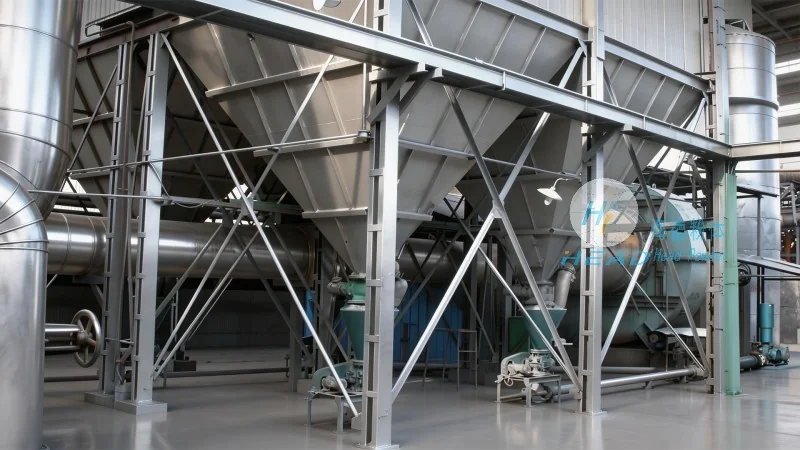
Introduction to Nitrogen-Protected Pneumatic Conveying Systems
Nitrogen-protected pneumatic conveying systems represent a sophisticated approach to material handling, particularly for products that are sensitive to atmospheric conditions such as oxidation, moisture, or contamination. At the core of this technology is the use of nitrogen gas as a protective medium, which is introduced into the conveying pipeline to create an inert environment. This method is widely adopted in industries where material purity and process safety are paramount, including pharmaceuticals, food processing, and high-purity chemicals.
The Fundamental Principle of Pneumatic Conveying
The basic principle of pneumatic conveying involves the transport of bulk materials through a pipeline using a gas stream, typically air or a specialized gas like nitrogen. In a nitrogen-protected system, the gas is replaced or supplemented with nitrogen to maintain a low-oxygen atmosphere. This process ensures that the conveyed material remains protected from external factors that could degrade its quality or safety. The system operates by generating a pressure differential, either through positive pressure (where the conveying line is pressurized) or negative pressure (where the line is vacuumed), to move the material from the source to the destination.
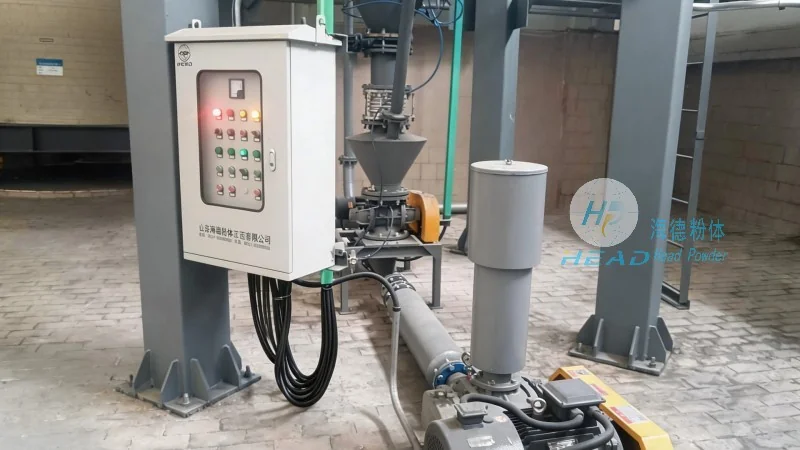
Key Working Scene Characteristics
The working scene characteristics of nitrogen-protected pneumatic conveying systems are tailored to meet the specific demands of various industrial applications. These systems are designed to handle a wide range of materials, from fine powders to granules, with precision and efficiency. One of the primary advantages is the ability to maintain a consistent flow rate and pressure, which minimizes material degradation and ensures uniform product quality. Additionally, the nitrogen environment reduces the risk of fire or explosion, making it suitable for handling flammable or explosive materials under controlled conditions.
Applications in Different Industries
The versatility of nitrogen-protected pneumatic conveying systems makes them indispensable in several sectors. In the pharmaceutical industry, these systems are crucial for transporting active pharmaceutical ingredients (APIs) and other sensitive powders, where contamination and oxidation can compromise drug efficacy and safety. The food processing sector utilizes such systems to handle ingredients like flour, sugar, and spices, ensuring that the products remain fresh and free from spoilage. In the chemical industry, especially for high-purity chemicals and specialty materials, the nitrogen protection prevents chemical reactions that could alter the material's properties, thus maintaining product integrity throughout the conveying process.
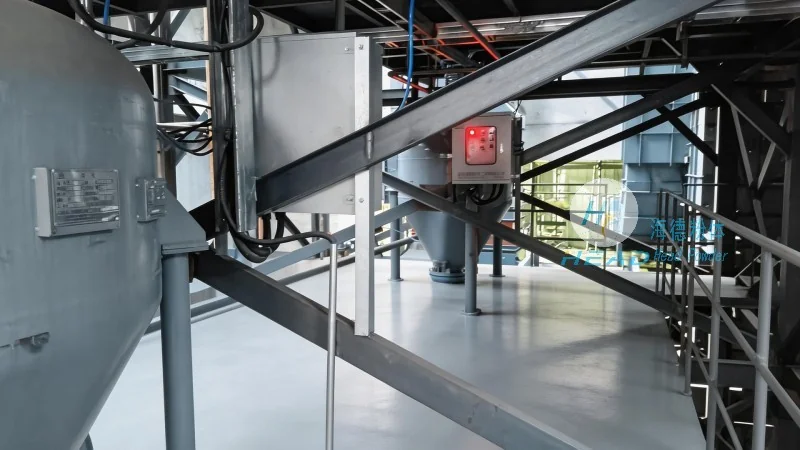
Advantages and Operational Benefits
Implementing a nitrogen-protected pneumatic conveying system offers several operational benefits. Firstly, it enhances material safety by eliminating the presence of oxygen, which is critical for preventing combustion or chemical reactions in flammable materials. Secondly, the system improves product quality by protecting the material from moisture and contaminants, which is vital for industries where product purity is a regulatory requirement. Furthermore, the use of nitrogen as a conveying medium can reduce the need for additional drying or cleaning steps, as the material remains in a controlled environment from source to destination. The systems are also designed for energy efficiency, with optimized pressure and flow rates that minimize operational costs while maximizing throughput.
Conclusion
Shandong HeadPowder Engineering Co., Ltd. leverages its expertise in engineering and material handling to provide customized nitrogen-protected pneumatic conveying solutions that meet the stringent requirements of modern industries. By integrating advanced technology with robust design, the company ensures that its systems deliver reliable performance, enhanced safety, and superior product protection. As a leading provider in this field, Headpowder continues to innovate and adapt its solutions to address the evolving needs of its clients, solidifying its position as a trusted partner in efficient and safe material transport.