With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design and implementation of advanced material handling solutions tailored for organic salt applications. The organic salt material handling system is engineered to efficiently transport and manage organic salt materials, addressing the unique challenges posed by these substances in industrial processes. This system integrates cutting-edge technology and robust engineering to ensure reliable operation and optimal performance in various industrial settings.
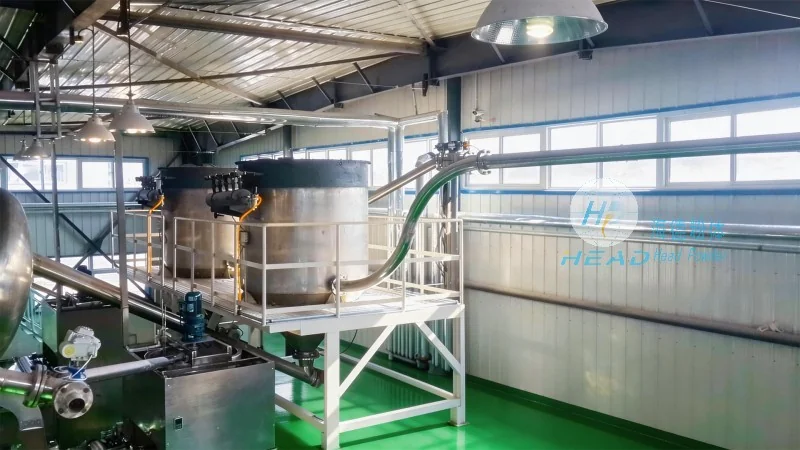
The core principle of the organic salt material handling system revolves around the seamless integration of mechanical, pneumatic, or hydraulic components to facilitate the movement of organic salt materials from storage to processing units. The system typically includes components such as conveyors, feeders, and control mechanisms that work in tandem to maintain consistent material flow. The design emphasizes efficiency, safety, and durability, ensuring that the system can handle the physical and chemical properties of organic salts without degradation or contamination. Key to the system's operation is the precise control of material movement, which is achieved through advanced sensors and automation technologies that monitor and adjust the flow rate and direction as needed.
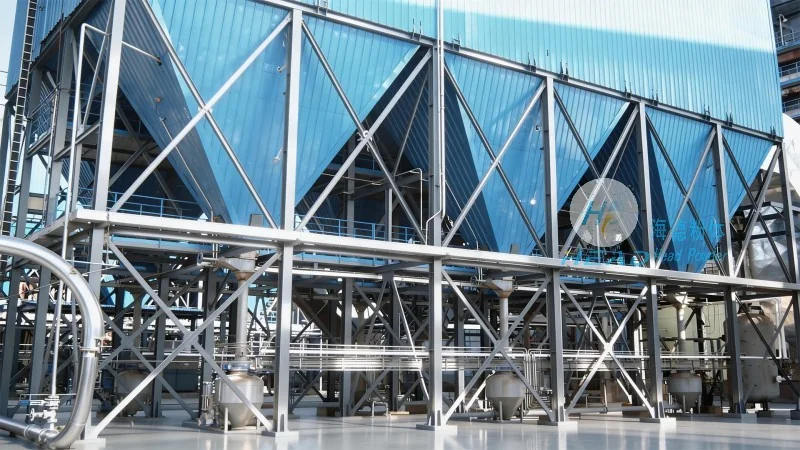
Organic salt material handling systems are deployed in diverse industrial scenarios, each with specific requirements that the system addresses. For instance, in chemical manufacturing facilities, these systems are used to transport organic salts from bulk storage to reactors or mixing tanks, ensuring a continuous and controlled supply of raw materials. In food processing industries, the systems are adapted to handle organic salt products with strict hygiene standards, incorporating sanitary design elements to prevent contamination. Additionally, in mining and mineral processing operations, the systems are utilized to transport organic salt concentrates from extraction sites to processing plants, optimizing the material's utilization and reducing operational costs. The versatility of the system allows it to be customized for different applications, making it a reliable solution across various sectors.
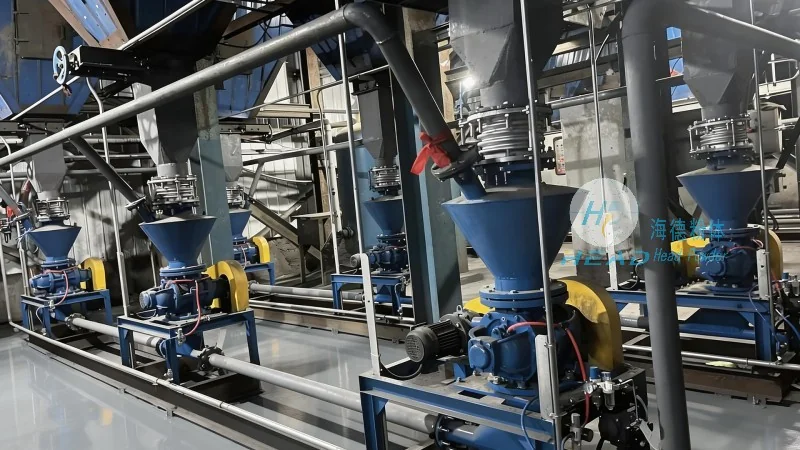
The organic salt material handling system comprises several critical components, each playing a vital role in the overall operation. The primary components include conveyor belts or screw conveyors, which are designed to handle the bulk movement of organic salt materials. These conveyors are equipped with materials that resist corrosion and wear, ensuring long-term durability. Feeders, such as vibratory or rotary feeders, are used to regulate the flow of organic salt into the conveyor system, maintaining a consistent feed rate. Control panels and automation systems provide real-time monitoring and adjustment of the system's parameters, enhancing operational efficiency and safety. Additionally, the system may include dust suppression and filtration systems to mitigate the environmental impact of organic salt handling, particularly in applications where dust generation is a concern.
Implementing an organic salt material handling system offers numerous advantages for industrial operations. Firstly, the system enhances productivity by ensuring a continuous and uninterrupted flow of materials, reducing downtime and increasing throughput. Secondly, it improves safety by minimizing manual handling of organic salt, which can be hazardous due to its physical properties or chemical interactions. Thirdly, the system contributes to cost savings through reduced labor requirements and lower maintenance costs, as the automated design reduces the need for frequent manual adjustments. Furthermore, the system's adaptability allows it to be integrated with existing industrial infrastructure, making it a cost-effective solution for upgrading or expanding material handling capabilities. The robust construction and advanced technology also ensure long-term reliability, providing a stable and efficient solution for organic salt handling needs.
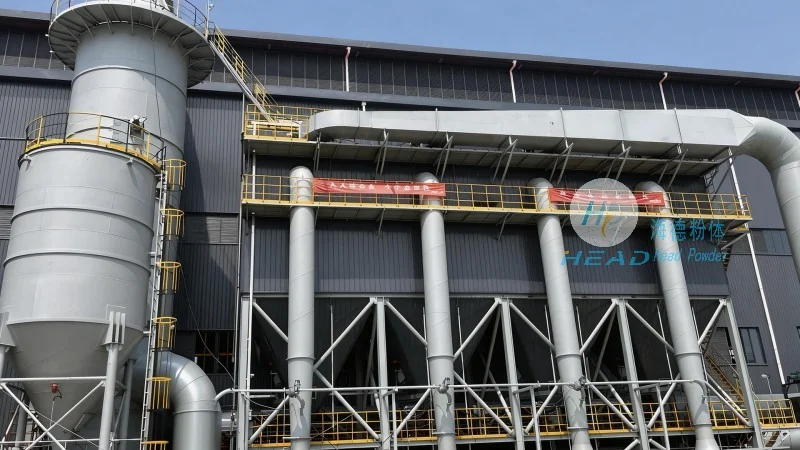
Real-world applications of the organic salt material handling system illustrate its effectiveness in various industrial contexts. For example, in a chemical plant producing organic salts for pharmaceutical use, the system was implemented to transport raw organic salt from storage silos to the production line. The system's ability to maintain a consistent flow rate and control dust emissions ensured compliance with environmental regulations and improved product quality. In another case, a food processing facility used the system to handle organic salt for seasoning production, where the sanitary design and hygienic materials prevented contamination, meeting stringent food safety standards. These examples highlight the system's versatility and adaptability, demonstrating its suitability for a wide range of organic salt applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top