

Working Principle and Features of Capsule Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems. Among their product lineup is the capsule pneumatic conveying equipment, which has gained recognition for its efficiency and adaptability in material handling applications. This article delves into the working principle and key features of this innovative equipment, providing a comprehensive overview for industry professionals seeking reliable solutions for bulk material transport.
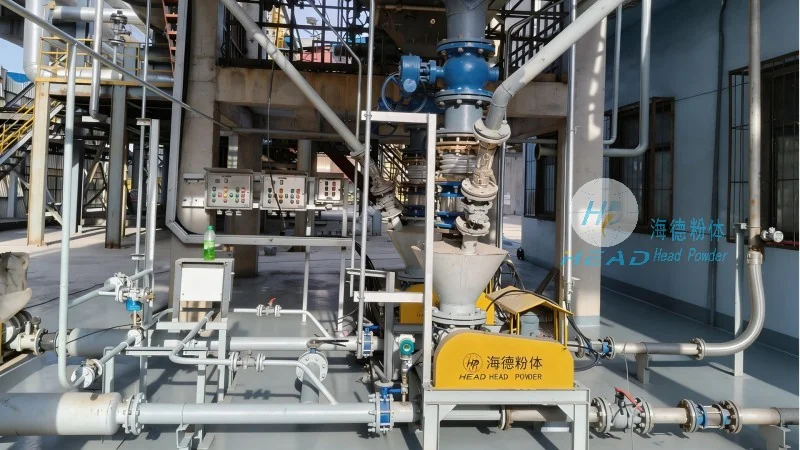
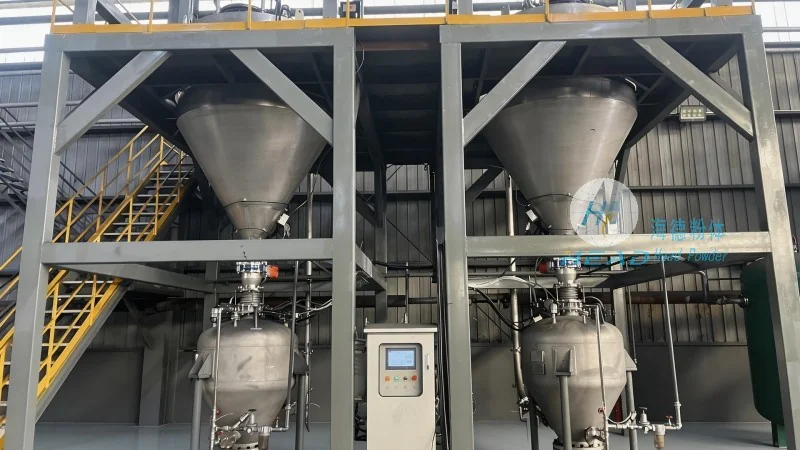
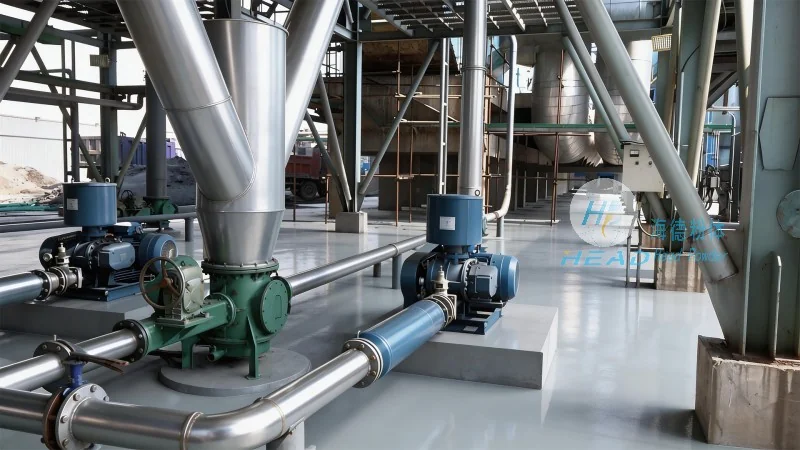
Understanding the Working Principle of Capsule Pneumatic Conveying Equipment
The capsule pneumatic conveying system operates on the principle of air-driven material transport, utilizing a series of interconnected capsules or segments to move bulk materials from one location to another. The process begins with the material being loaded into the inlet hopper, where it is then fed into the first capsule. As the system generates a pressure differential, air is introduced to create a flow that propels the material through the connected capsules. Each capsule acts as a flexible container, allowing the equipment to navigate changes in direction and elevation with minimal resistance. The continuous movement of air and material ensures a smooth and consistent transfer, minimizing product degradation and operational disruptions.
Key Features of Capsule Pneumatic Conveying Equipment
HeadPowder's capsule pneumatic conveying equipment is distinguished by several notable features that enhance its performance and usability. Firstly, the flexible, segmented design enables the system to handle a wide range of materials, including powders, granules, and even bulk solids with varying particle sizes and flow characteristics. This adaptability is crucial for industries such as pharmaceuticals, food processing, and chemical manufacturing, where material compatibility is paramount. Secondly, the equipment offers superior energy efficiency compared to traditional pneumatic conveying methods. By optimizing air usage and reducing pressure losses, the system minimizes operational costs while maintaining high throughput rates. Additionally, the modular construction allows for easy installation and maintenance, with individual capsules being replaceable without disrupting the entire system. This flexibility in maintenance reduces downtime and extends the equipment's service life. Another significant feature is the system's ability to handle long-distance and high-elevation transfers. The interconnected capsules can be arranged in a linear or zigzag configuration to cover large distances and overcome vertical obstacles, making it suitable for complex production layouts. Furthermore, the equipment is designed with safety and hygiene in mind, featuring sealed components that prevent contamination and ensure compliance with industry standards. This is particularly important in industries where product purity is critical, such as food and pharmaceuticals. The system also incorporates advanced control mechanisms, allowing for precise regulation of air pressure and flow rates. This enables operators to adjust the conveying speed and pressure in real-time, optimizing performance based on the specific material being handled. The result is a more controlled and efficient transfer process, reducing the risk of material spillage or blockages. In summary, the capsule pneumatic conveying equipment from HeadPowder combines innovative design with practical features to deliver reliable and efficient material handling solutions. Its ability to handle diverse materials, maintain energy efficiency, and adapt to complex layouts makes it a valuable asset for businesses seeking to improve their production processes. With a focus on quality and performance, HeadPowder continues to lead the industry in providing advanced pneumatic conveying systems that meet the evolving needs of modern manufacturing.