

Working Principle and Features of Aggregate Pneumatic Conveying Systems
Aggregate pneumatic conveying systems are essential in modern material handling, offering efficient and flexible solutions for transporting bulk materials like aggregates. These systems utilize air as the primary medium to move materials from one location to another, eliminating the need for traditional mechanical conveyors and reducing operational costs.
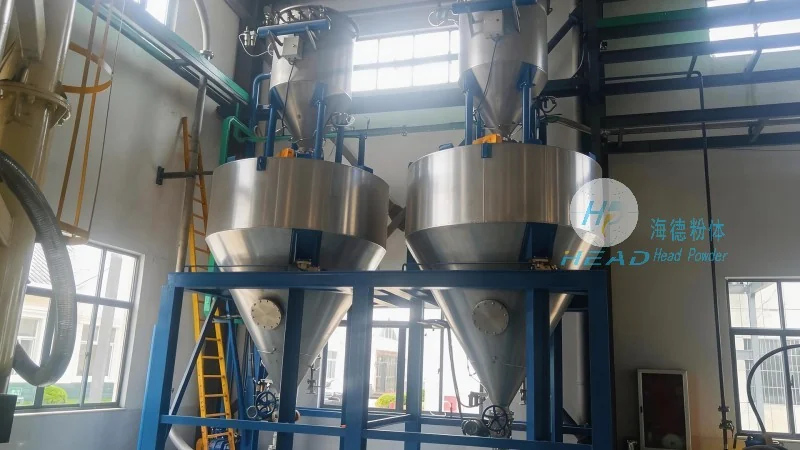
Working Principle of Aggregate Pneumatic Conveying Systems
The core working principle of aggregate pneumatic conveying systems revolves around the use of compressed air to create a flow that propels the material through a pipeline. The process typically involves several key components: a material hopper for storage, a feeder to control the flow rate, a compressor to generate the necessary air pressure, and a pipeline network to transport the material. When the feeder releases the aggregate into the pipeline, the compressed air creates a low-pressure zone that draws the material along with the air stream. This combination of air and material forms a dense phase or dilute phase flow, depending on the system design and operational parameters. The system can operate in either positive pressure or negative pressure modes, with positive pressure being more common for long-distance or high-capacity applications. The air pressure is carefully regulated to ensure optimal material transport without causing excessive wear on components or excessive energy consumption.
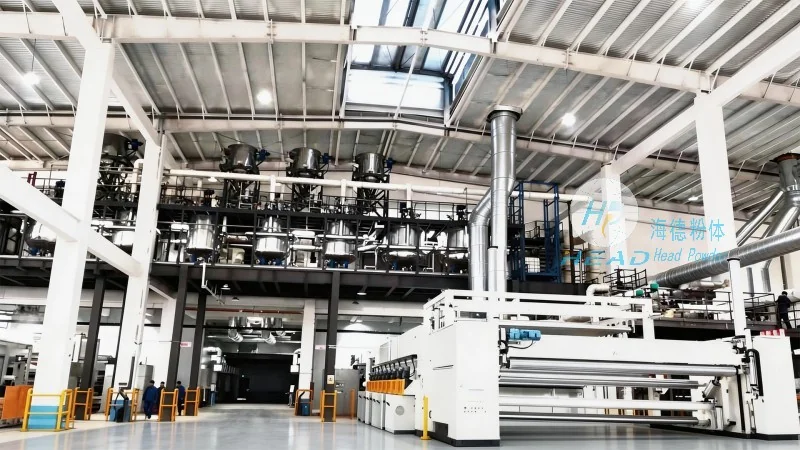
Key Features of Aggregate Pneumatic Conveying Systems
Aggregate pneumatic conveying systems offer several distinct advantages that make them ideal for various industrial applications. One of the primary features is their ability to handle a wide range of materials, including fine powders, granules, and larger aggregate particles, with minimal degradation or segregation. The flexible pipeline layout allows for easy integration into existing production lines or facility layouts, enabling complex material flow paths without the need for extensive civil engineering modifications. Another significant feature is the hygienic and dust-free operation, which is crucial in industries such as food processing, pharmaceuticals, and chemical manufacturing where contamination control is paramount. The systems also provide excellent dust suppression, reducing the risk of airborne particulates and improving workplace safety. Additionally, pneumatic conveying systems are highly efficient in terms of energy consumption compared to traditional belt or screw conveyors, especially for long-distance transport. They offer low maintenance requirements due to the absence of moving parts in the pipeline, and the ability to operate in both horizontal and vertical orientations provides design flexibility. The systems can be equipped with advanced control systems that monitor pressure, flow rate, and material level, ensuring consistent performance and reducing downtime.
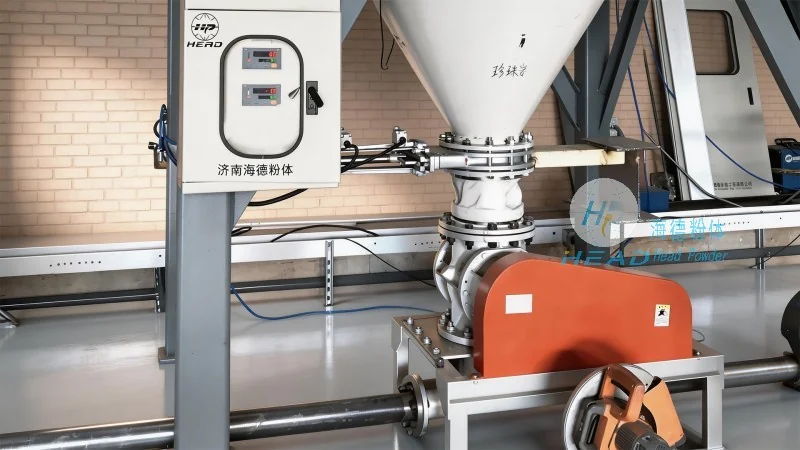
Applications and Benefits in Industrial Settings
Aggregate pneumatic conveying systems are widely used across multiple industries, including construction, mining, and manufacturing. In the construction industry, they are used to transport sand, gravel, and cement from storage silos to mixing plants or job sites, improving material handling efficiency and reducing labor costs. In mining operations, these systems are employed to move ore and other bulk materials from processing facilities to storage or transport vehicles, enhancing operational throughput. The benefits of these systems extend beyond material transport efficiency, as they contribute to improved safety by minimizing manual handling of heavy or dusty materials and reducing the risk of workplace accidents. The hygienic design of the systems also makes them suitable for food and pharmaceutical applications, where product purity and operator safety are critical. The ability to handle different material types and flow configurations makes aggregate pneumatic conveying systems a versatile solution for various industrial needs.
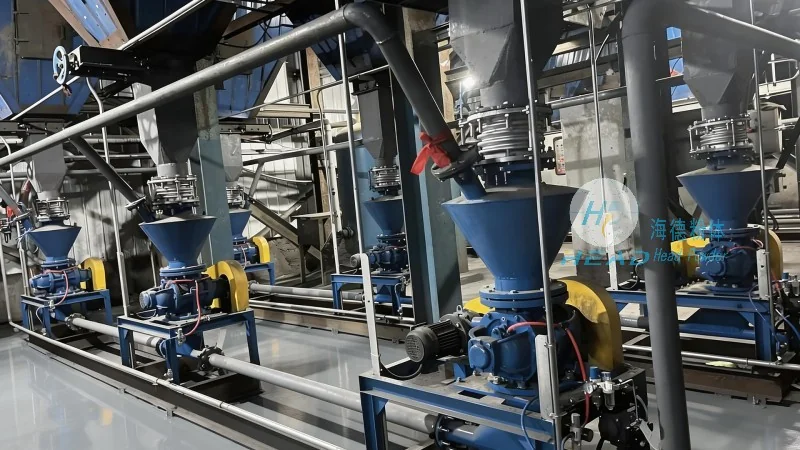
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a leading manufacturer and supplier of aggregate pneumatic conveying systems. With a strong focus on innovation and quality, the company has established itself as a trusted partner in the material handling industry. HeadPowder specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the specific needs of clients, ensuring optimal performance and reliability. The company's products are engineered to meet international standards and are backed by comprehensive technical support and after-sales service. HeadPowder's commitment to customer satisfaction and technological advancement has made it a preferred choice for businesses seeking efficient and reliable material transport solutions. Located in Shandong, China, HeadPowder leverages its local expertise and manufacturing capabilities to deliver high-quality products that meet the demands of modern industrial applications.