With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Ammonium bicarbonate, a widely used chemical in industrial applications, requires efficient and reliable powder conveying systems to ensure safe and effective material handling. The operation process and working principle of such a system, particularly for headpowder's advanced solutions, involve a series of integrated components and controlled processes designed to maintain product integrity and operational efficiency.
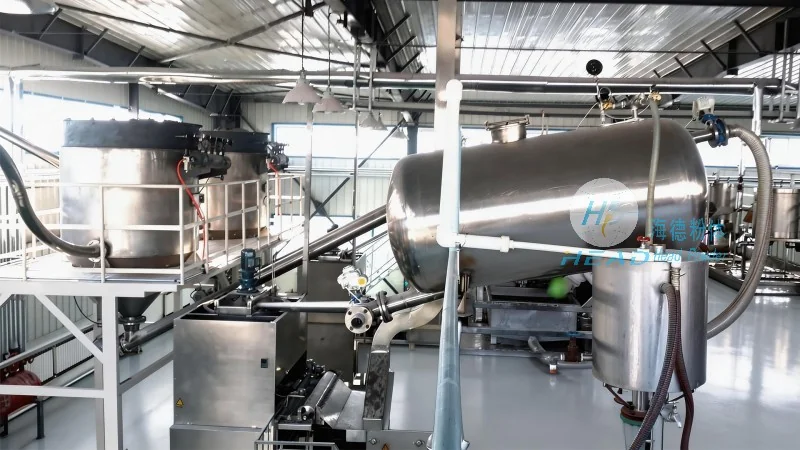
The Ammonium Bicarbonate Powder Conveying System by Shandong HeadPowder Engineering Co., Ltd. is engineered to handle the unique properties of ammonium bicarbonate, including its hygroscopic nature and potential for dust generation. The system typically consists of several key components: a hopper for material storage, a feeder to regulate the flow rate, a conveying mechanism (such as pneumatic or mechanical), and a control system for monitoring and adjustment. Each component is carefully selected and integrated to ensure seamless operation and minimal product degradation.
At the initial stage of the conveying process, ammonium bicarbonate is stored in a large hopper equipped with a level indicator and a discharge valve. The hopper is designed to prevent moisture accumulation and ensure uniform material flow. The feeder, often a rotary valve or a screw feeder, controls the amount of material released into the conveying line. This step is critical as ammonium bicarbonate is hygroscopic, meaning it can absorb moisture from the air, which may affect its performance and handling characteristics. The feeder's speed is adjusted based on the required output rate, ensuring consistent material delivery to the next stage.
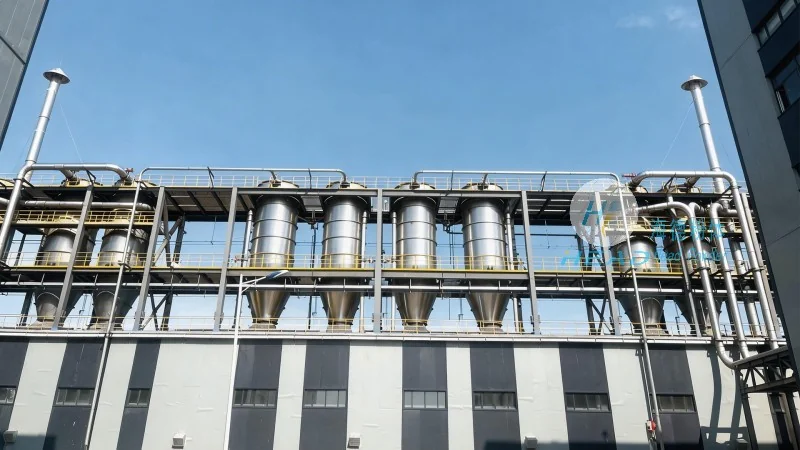
The conveying mechanism is the heart of the system, responsible for transporting the ammonium bicarbonate powder from the storage hopper to the destination point. Shandong HeadPowder Engineering Co., Ltd. offers both pneumatic and mechanical conveying options, with the choice depending on the specific application requirements. For example, pneumatic conveying uses compressed air to move the powder through a pipeline, while mechanical conveying employs screw conveyors or belt systems. The working principle involves creating a pressure differential or mechanical force to move the material along the conveying path. In pneumatic systems, the air velocity is maintained above the material's terminal velocity to prevent particle deposition and ensure smooth transport. The system also includes filters and cyclones to separate any entrained air or dust, maintaining product purity.
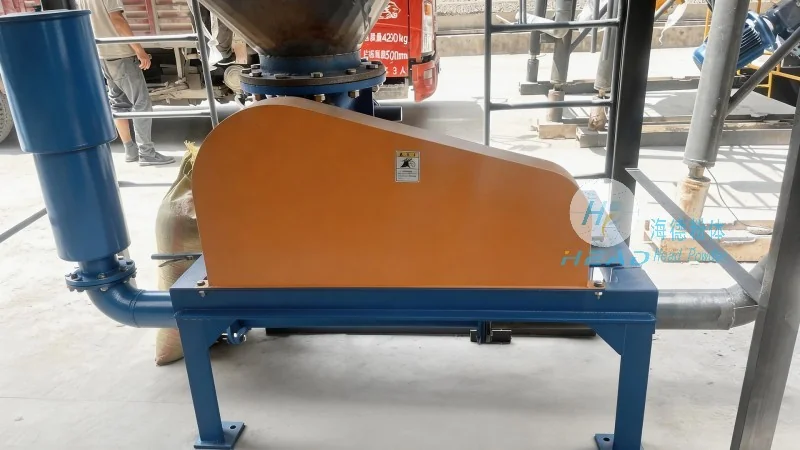
Efficient operation of the ammonium bicarbonate powder conveying system relies on advanced control and monitoring systems. These systems include sensors for material level, flow rate, and pressure, as well as a programmable logic controller (PLC) that coordinates the operation of all components. The PLC continuously monitors the system parameters and adjusts the feeder speed or air pressure as needed to maintain the desired output. Additionally, the system may include alarms and safety interlocks to prevent overfilling or equipment failure, ensuring safe and reliable operation. The control panel is typically located in a central position, allowing operators to easily monitor and adjust the system settings.
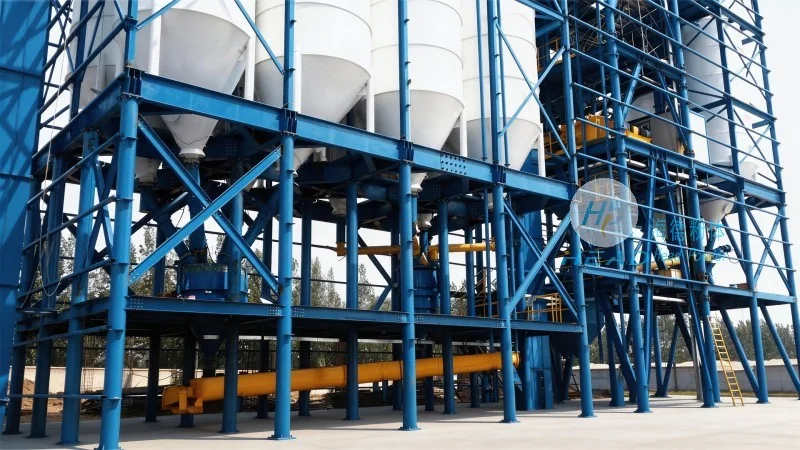
To ensure long-term performance and reliability of the ammonium bicarbonate powder conveying system, regular maintenance is essential. This includes cleaning the hopper and conveying lines to prevent buildup of moisture or dust, inspecting the feeder and conveying mechanism for wear and tear, and checking the air compressor or motor for proper operation. The system is designed with easy access points for maintenance, reducing downtime and maintenance costs. Additionally, operators should follow the manufacturer's guidelines for material handling, including proper storage conditions and handling procedures to prevent product degradation. By adhering to these operational considerations, the system can maintain its efficiency and ensure consistent product quality.
The operation process and working principle of the Ammonium Bicarbonate Powder Conveying System by Shandong HeadPowder Engineering Co., Ltd. demonstrate a comprehensive approach to handling this critical chemical. The system's design, incorporating advanced components and control systems, ensures safe, efficient, and reliable material transport. With its ability to handle the unique properties of ammonium bicarbonate, this system is suitable for various industrial applications, including fertilizer production, food processing, and chemical manufacturing. Shandong HeadPowder Engineering Co., Ltd. continues to innovate and improve its conveying solutions to meet the evolving needs of the industry, providing customers with high-quality and reliable equipment for their ammonium bicarbonate handling requirements.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top