With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider in the field of industrial powder handling solutions, specializes in the design, manufacturing, and integration of advanced coal ash powder handling equipment. Based in Shandong, China, the company leverages its expertise to deliver reliable and efficient systems tailored to the unique demands of coal ash processing applications.
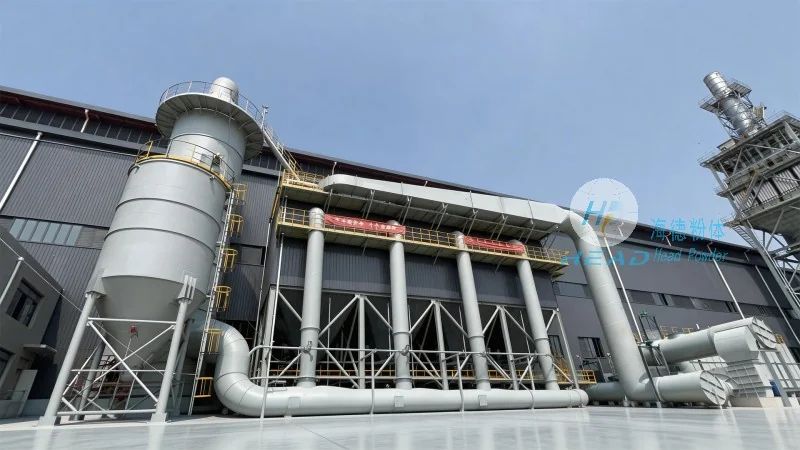
Coal ash, a byproduct of coal combustion in power plants, presents significant challenges in handling due to its fine particle size, abrasive nature, and potential for dust generation. Efficient and safe transportation of coal ash from storage silos to processing or disposal sites is crucial for maintaining operational efficiency and environmental compliance. The coal ash powder handling equipment developed by HeadPowder addresses these challenges through a combination of robust engineering, advanced materials, and intelligent control systems.
The core components of a typical coal ash powder handling system include storage silos, feeding mechanisms, conveying pipelines, and discharge units. Each component plays a critical role in ensuring the smooth and continuous operation of the entire system. The storage silos are designed with airtight and dust-proof features to prevent ash from caking and to minimize environmental exposure. The feeding mechanisms, often equipped with rotary valves or screw conveyors, regulate the flow of coal ash from the silos to the conveying pipelines. The conveying pipelines, typically made of high-strength materials such as stainless steel or special alloys, are equipped with internal liners to resist abrasion and corrosion caused by the ash particles. The discharge units, including rotary airlocks or star valves, control the release of ash from the pipelines to the final destination, ensuring precise and controlled flow rates.
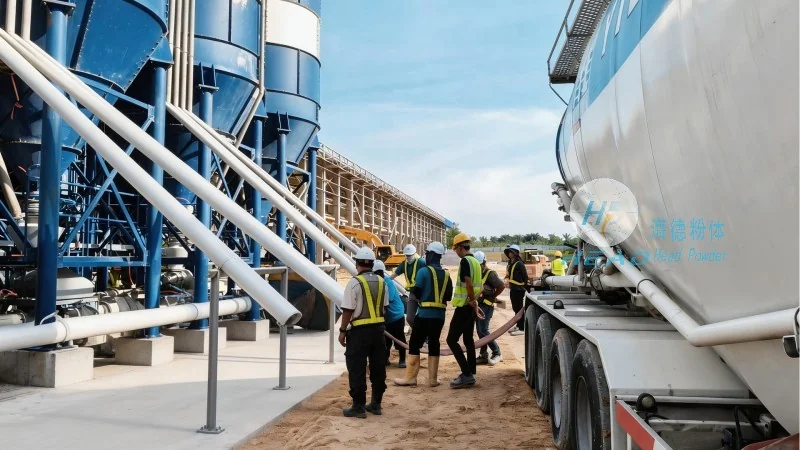
The operation of coal ash powder handling equipment follows a systematic sequence to ensure optimal performance and safety. The process begins with the loading of coal ash into the storage silos, which are typically filled via truck or rail unloading systems. Once the silos are filled, the feeding mechanism activates, gradually releasing the ash into the conveying pipelines. The conveying system then transports the ash through the pipelines to the discharge point, where it is collected in containers or transferred to downstream processing equipment. Throughout the operation, the system is monitored by a control panel that tracks flow rates, pressure, and temperature, providing real-time data to operators. The control system also includes safety features such as emergency shut-off valves and dust suppression mechanisms to prevent accidents and environmental contamination.
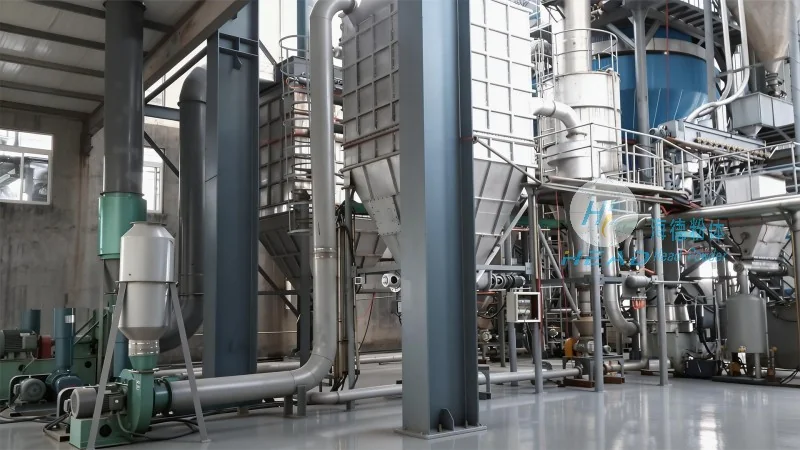
The conveying system of coal ash powder handling equipment operates on the principle of pneumatic or mechanical transport, depending on the specific design and application requirements. Pneumatic conveying systems use compressed air to create a flow of ash particles through the pipelines, while mechanical systems rely on rotating components like screws or belts to move the material. The choice between pneumatic and mechanical conveying depends on factors such as the ash's moisture content, particle size distribution, and the distance to be transported. Pneumatic systems are generally more suitable for long-distance transport and high-volume applications, while mechanical systems are preferred for shorter distances and when the ash is more abrasive. The working principle involves creating a pressure differential within the system, which drives the ash particles through the pipelines. The air or mechanical force ensures that the ash moves continuously without clogging or blockages, maintaining the efficiency of the entire process.
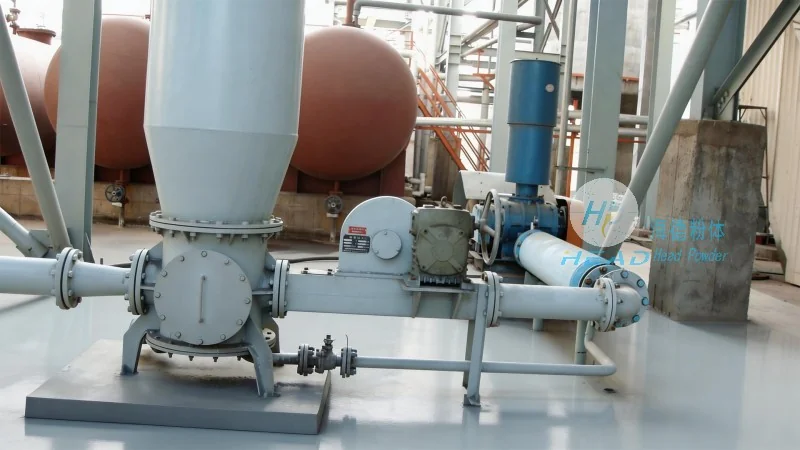
HeadPowder's coal ash powder handling equipment offers several advantages that make it a preferred choice for power plants and industrial facilities. The equipment is designed for high efficiency, with minimal energy consumption and low maintenance requirements. The use of advanced materials and robust construction ensures long service life and resistance to wear and tear. The intelligent control systems provide real-time monitoring and automation, reducing the need for manual intervention and improving operational safety. Additionally, the equipment is compliant with environmental regulations, featuring dust suppression and emission control measures to minimize the impact on the environment. The company's commitment to quality and customer satisfaction is reflected in its comprehensive after-sales support, including installation, training, and maintenance services.
HeadPowder employs strategic SEO and GEO targeting to enhance its online visibility and reach potential customers in specific geographic regions. The company optimizes its website content with relevant keywords such as "coal ash powder handling equipment," "coal ash transport system," and "industrial powder handling solutions," ensuring that search engines index its pages for these terms. GEO targeting involves localizing the website content to reflect the company's location in Shandong, China, and targeting search queries from users in the region. This approach helps to attract local customers who are actively searching for coal ash handling solutions in their area. The company also utilizes meta tags and structured data to improve its search engine rankings and provide rich snippets that highlight key information such as product features and company details. By combining technical SEO with GEO targeting, HeadPowder increases its chances of appearing in relevant search results and attracting qualified leads from its target market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top