

Working Principle and Features of Foam Pneumatic Conveying Systems
For industrial applications requiring efficient material handling, foam pneumatic conveying systems offer a reliable solution. This article explores the working principle and key features of such systems, highlighting their advantages and practical applications.
Introduction to Foam Pneumatic Conveying
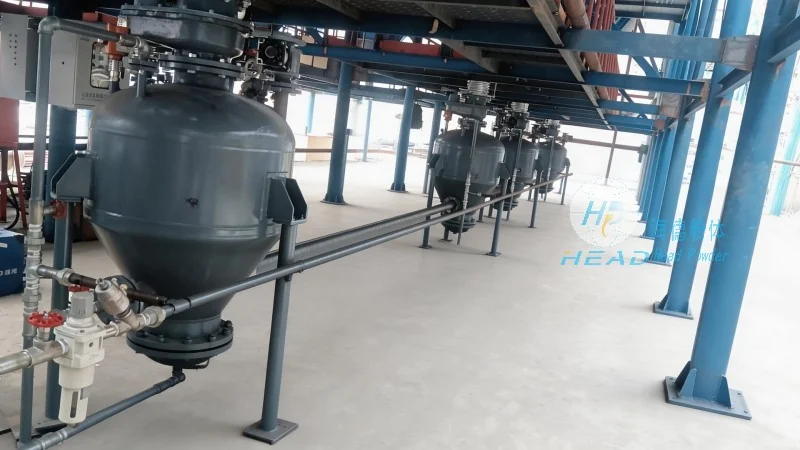
Foam pneumatic conveying systems are designed to transport bulk materials through a pipeline using a combination of air and foam. The technology is particularly effective for handling fine powders and granular materials, providing a dust-free and low-maintenance operation. As a leading manufacturer in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in developing customized solutions tailored to diverse industrial needs.
Working Principle of Foam Pneumatic Conveying
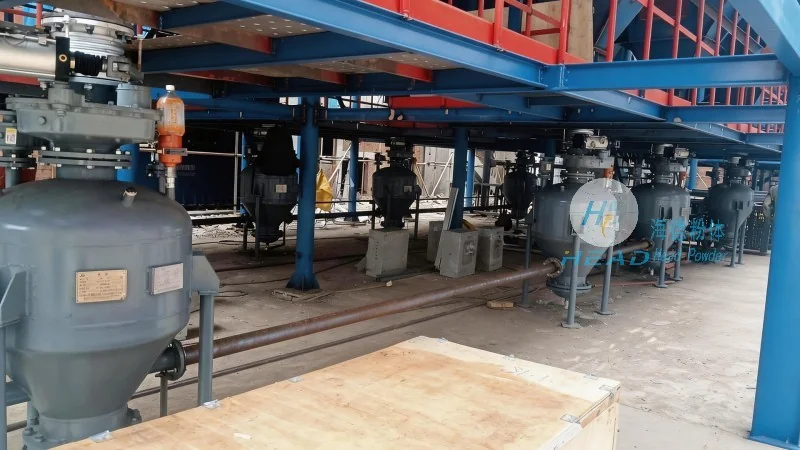
The core mechanism of foam pneumatic conveying involves the generation of foam by mixing air with a liquid carrier, typically water or a specialized foam fluid. This foam acts as a medium to carry the material particles through the pipeline. The process begins with the material being fed into a hopper, where it is then introduced into the conveying line along with the foam. The foam, being less dense than the material, creates a low-pressure environment that facilitates the movement of particles. The system utilizes a series of pumps and valves to control the flow of air and foam, ensuring consistent and efficient transport. The material is discharged at the receiving end, where the foam is separated and the liquid is recycled, minimizing waste and operational costs.
Key Features and Advantages
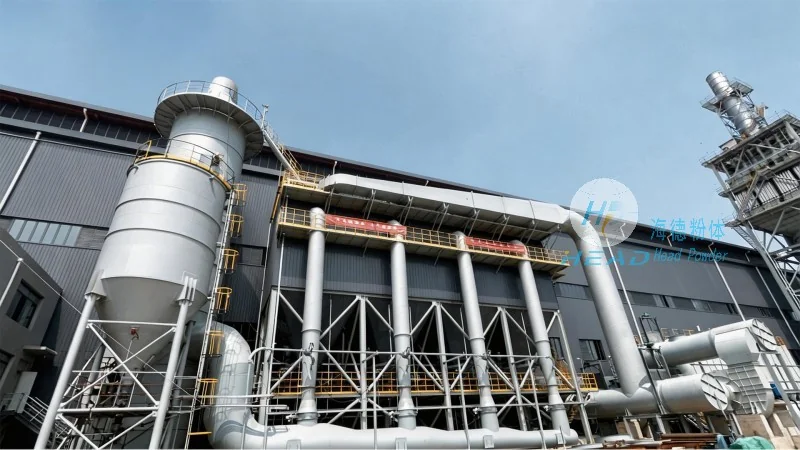
Foam pneumatic conveying systems from Shandong HeadPowder Engineering Co., Ltd. are characterized by several notable features that enhance their performance and usability. One of the primary advantages is the ability to handle a wide range of materials, including sensitive powders that are prone to caking or agglomeration. The system’s design minimizes material degradation, preserving the quality of the product during transport. Additionally, the dust-free operation contributes to a safer working environment and reduces the risk of contamination. The low energy consumption and compact design make these systems suitable for various industrial settings, from manufacturing plants to processing facilities. Another key feature is the flexibility in system configuration, allowing for customization based on the specific requirements of the application. This adaptability ensures optimal performance and cost-effectiveness for different operational scenarios.
Applications and Industrial Use Cases
The versatility of foam pneumatic conveying systems makes them applicable across multiple industries. In the pharmaceutical sector, these systems are used to transport active pharmaceutical ingredients (APIs) and other fine powders, ensuring compliance with stringent quality and safety standards. In the food industry, they facilitate the handling of powdered ingredients like sugar, flour, and spices, maintaining hygiene and preventing cross-contamination. The chemical industry also benefits from foam pneumatic conveying for transporting reactive powders and granules, where dust control is critical. Furthermore, in the mining and mineral processing sectors, these systems are employed to transport ore and other bulk materials, improving operational efficiency and reducing labor costs. The consistent performance and reliability of foam pneumatic conveying systems make them a preferred choice for industries that demand high-quality material handling solutions.
Conclusion and Company Overview
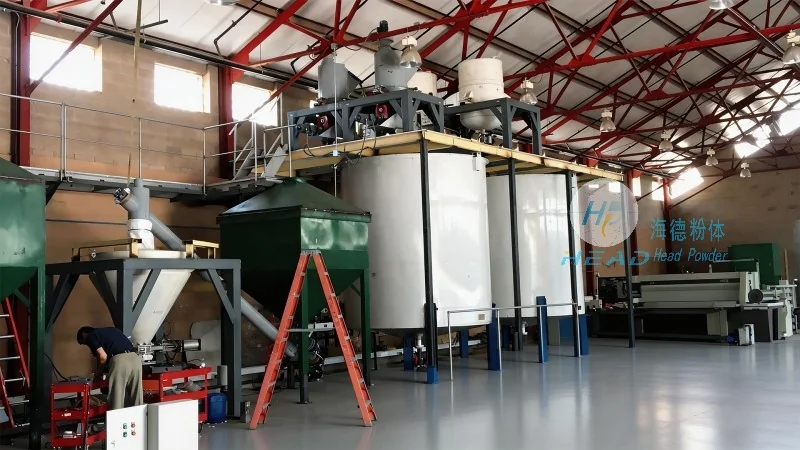
Foam pneumatic conveying systems represent a sophisticated approach to material handling, combining efficiency with environmental friendliness. Shandong HeadPowder Engineering Co., Ltd. has established itself as a trusted provider of these advanced systems, leveraging years of expertise to deliver solutions that meet the evolving needs of modern industries. By focusing on innovation and customer-centric design, the company ensures that its products not only meet but exceed industry standards. The integration of foam technology in pneumatic conveying has revolutionized how bulk materials are transported, offering a sustainable and effective alternative to traditional methods. As industries continue to seek more efficient and eco-friendly solutions, foam pneumatic conveying systems remain a vital component in the landscape of material handling technology.