

What is a Bin Pump Powder Pneumatic Conveying System? And What Are Its Design Principles?
A bin pump powder pneumatic conveying system is a specialized industrial equipment designed for the efficient and reliable transportation of bulk powder materials over long distances or through complex layouts. This system utilizes a combination of mechanical and pneumatic components to achieve the transport of powders, such as cement, flour, or other fine particulate materials, from a storage bin or hopper to a destination like a silo, processing unit, or packaging station. The core of this system is the bin pump, which acts as the primary transport device, working in conjunction with a compressed air system to create the necessary pressure and flow for material movement.
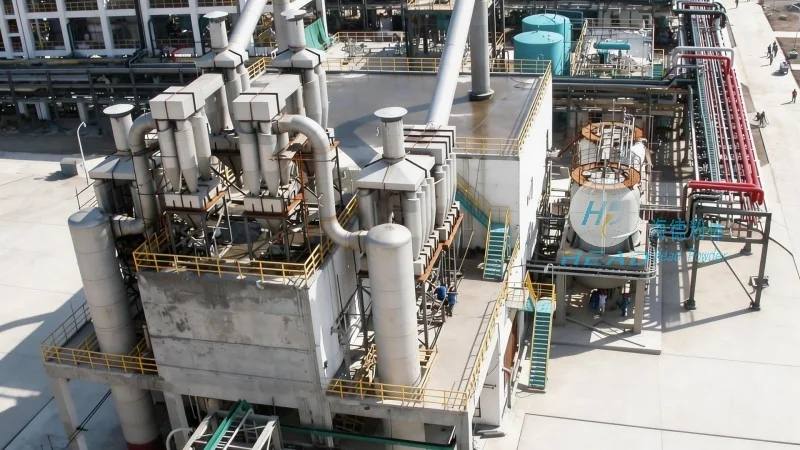
Key Components of the Bin Pump System
The bin pump powder pneumatic conveying system consists of several critical components that work together to ensure smooth operation. The main components include the storage bin or hopper, where the powder is initially stored; the bin pump itself, which is responsible for the actual transport of the material; a compressed air system that provides the necessary pressure to drive the powder; a filter system to capture any dust or particles that may be released during operation; and a control system that monitors and regulates the entire process. Each component plays a vital role in the overall efficiency and safety of the system.
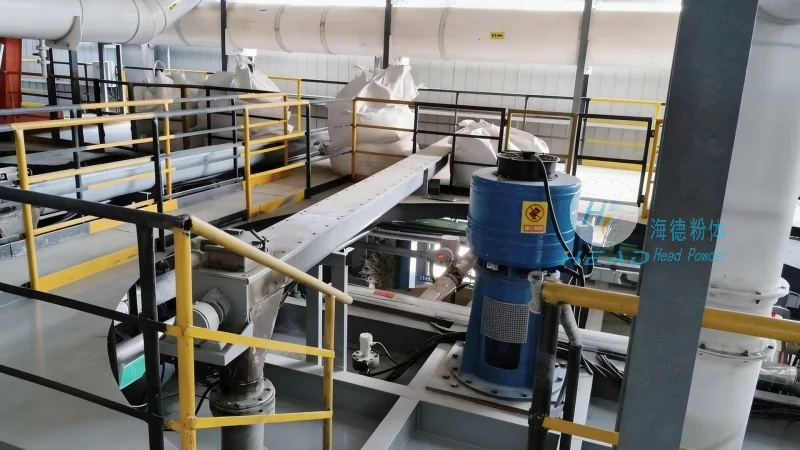
Design Principles of the Bin Pump System
The design principles of a bin pump powder pneumatic conveying system are centered on achieving optimal performance, reliability, and energy efficiency. The system is engineered to handle a wide range of powder characteristics, including different particle sizes, densities, and flow properties. The bin pump is typically designed as a positive displacement device, meaning it uses a piston or diaphragm to create a vacuum or pressure to draw and discharge the powder. This design allows for consistent and controlled material flow, reducing the risk of clogging or blockages that can occur in other types of pneumatic conveying systems. Additionally, the system is designed with safety features to prevent dust explosions and ensure compliance with industrial safety standards.
Operational Process and Efficiency
The operational process of a bin pump powder pneumatic conveying system involves several steps. First, the powder is fed into the storage bin from a hopper or other storage vessel. The bin pump then draws the powder into its chamber using the vacuum created by the compressed air system. Once the chamber is filled, the pump's mechanism (such as a piston) moves to compress the air and powder mixture, forcing the material through the conveying line to the destination. The compressed air then returns to the bin pump to create the next vacuum cycle, repeating the process continuously. This cycle ensures a steady and reliable flow of powder, minimizing downtime and maximizing productivity. The efficiency of the system is enhanced by the use of high-quality materials and components, such as stainless steel or corrosion-resistant materials, which are chosen to withstand the abrasive nature of the powder and the effects of moisture or other environmental factors.
Applications and Benefits
Bin pump powder pneumatic conveying systems are widely used in various industries, including cement production, food processing, pharmaceuticals, and chemical manufacturing. The primary benefits of this system include its ability to transport powders over long distances without the need for intermediate storage or manual handling, which reduces labor costs and improves safety. Additionally, the system is highly flexible, allowing for changes in the layout or destination of the conveying line without major modifications. The design also minimizes the risk of product contamination, as the system is enclosed and sealed, preventing exposure to external elements. Furthermore, the system is energy-efficient, as it uses compressed air in a controlled manner, reducing energy consumption compared to other transport methods.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of industrial powder handling equipment. With a focus on innovation and quality, the company specializes in the design, manufacturing, and installation of bin pump powder pneumatic conveying systems and other related equipment. Headpowder is committed to providing reliable and efficient solutions for the transportation of bulk powders, helping clients improve their operational efficiency and reduce costs. The company's products are manufactured using high-quality materials and advanced technology, ensuring durability and long-term performance. Headpowder serves clients in various industries, providing customized solutions to meet their specific needs. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility and research and development center.