With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced pneumatic conveying systems tailored for the efficient transportation of calcium carbonate limestone powder over long distances. This article provides a detailed overview of such systems, highlighting their technical features, operational advantages, and practical applications in industrial settings.
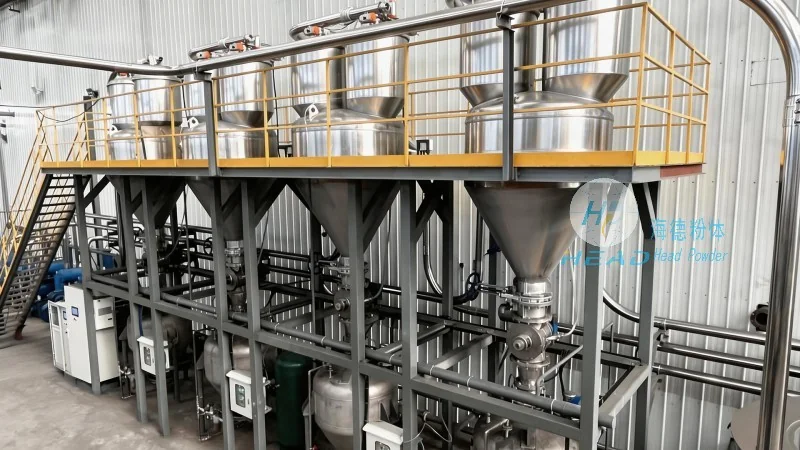
Long-distance pneumatic conveying systems represent a sophisticated solution for transporting bulk materials like calcium carbonate limestone powder from source to destination without the need for mechanical components such as belts or buckets. These systems utilize compressed air or other gases to move material through a network of pipes, offering a flexible and efficient method for material handling in various industrial processes. The system's design is critical to ensuring optimal performance, especially when dealing with materials that may have specific flow characteristics or require minimal degradation during transport.
The core components of a long-distance pneumatic conveying system for calcium carbonate limestone powder typically include a material feeder, a compressor or air supply unit, a pipeline network, and a receiver or discharge unit. The material feeder is responsible for accurately metering the limestone powder into the conveying line, ensuring consistent flow rates. The compressor generates the necessary air pressure to propel the material through the pipes, with pressure levels often ranging from low to high, depending on the distance and material properties. The pipeline network consists of straight sections, bends, and possibly expansion joints to accommodate the system's layout and environmental conditions. The receiver is designed to safely collect the conveyed material, often equipped with dust collection or filtration systems to maintain air quality and prevent material loss.
Compared to traditional mechanical conveying methods, pneumatic systems offer several advantages when handling calcium carbonate limestone powder. Firstly, they provide a dust-free and enclosed environment, which is crucial for maintaining product quality and ensuring workplace safety. The lack of moving parts reduces maintenance requirements and downtime, leading to lower operational costs over time. Additionally, pneumatic conveying systems can handle materials with varying particle sizes and moisture content, making them versatile for different production scenarios. The flexibility of the system allows for easy integration with existing industrial processes and the ability to transport materials over significant distances without intermediate storage or handling steps.
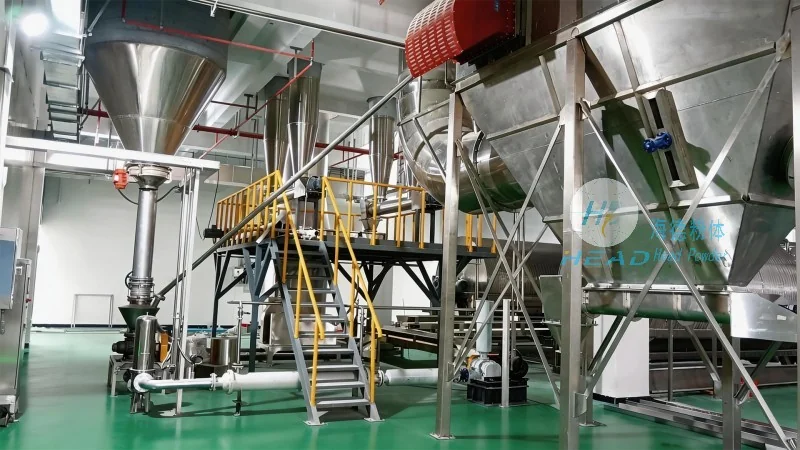
Efficiency in long-distance pneumatic conveying systems is evaluated based on several key performance indicators, including conveying capacity, pressure drop, and energy consumption. The conveying capacity refers to the volume of limestone powder that can be transported per unit time, which is influenced by factors such as air velocity, pipe diameter, and material density. Pressure drop along the pipeline is a critical parameter, as excessive pressure loss can reduce system efficiency and increase energy costs. Modern systems employ advanced control technologies to optimize air flow and pressure, ensuring consistent performance even under varying load conditions. Energy consumption is another important metric, with efficient compressors and system designs helping to minimize operational expenses while maintaining high throughput.
Long-distance pneumatic conveying systems for calcium carbonate limestone powder are widely used in various industries, including chemical manufacturing, pharmaceuticals, and food processing. In the chemical industry, these systems are employed to transport limestone powder to reactors or storage facilities, where it serves as a raw material for producing calcium compounds or other chemical products. In pharmaceutical applications, the enclosed and dust-free nature of the system is essential for maintaining product purity and meeting stringent regulatory standards. The food industry also benefits from these systems when handling limestone powder used as a food additive or in the production of calcium supplements. Each application requires careful consideration of material properties, such as particle size distribution and moisture content, to ensure the system operates effectively and safely.
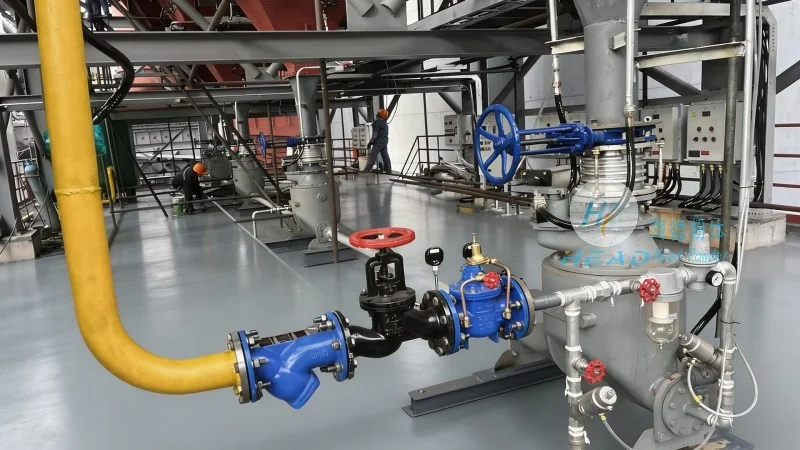
HeadPowder Engineering Co., Ltd., based in Shandong, China, offers customized pneumatic conveying solutions tailored to the specific needs of clients. The company's engineering team works closely with customers to assess their material handling requirements, system layout, and operational constraints to design a system that maximizes efficiency and minimizes costs. Customization may involve selecting appropriate pipe materials, adjusting air pressure levels, or incorporating additional features such as dust filtration or material recycling systems. HeadPowder's expertise in material flow dynamics and pneumatic system design ensures that the final solution is optimized for the unique characteristics of calcium carbonate limestone powder, providing reliable and long-lasting performance.
Proper maintenance is essential to ensure the long-term reliability and efficiency of long-distance pneumatic conveying systems. Regular inspections of components such as the compressor, pipeline, and material feeder help identify potential issues before they lead to system failures. Cleaning and maintenance of the pipeline and receiver are also critical to prevent material buildup and ensure consistent air flow. HeadPowder provides comprehensive maintenance services and technical support to clients, helping to extend the lifespan of the system and reduce downtime. By adhering to recommended maintenance schedules and using high-quality replacement parts, users can maintain optimal performance and minimize operational disruptions.
Long-distance pneumatic conveying systems for calcium carbonate limestone powder represent a highly effective and efficient solution for material handling in industrial applications. With their enclosed and dust-free operation, low maintenance requirements, and flexibility in system design, these systems offer significant advantages over traditional mechanical conveying methods. HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design and implementation of such systems, providing customized solutions that meet the specific needs of clients. By leveraging advanced engineering and technical expertise, HeadPowder ensures that its pneumatic conveying systems deliver reliable performance and contribute to the overall efficiency of industrial processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top