

What is a Negative Pressure Suction Type Powder Pneumatic Conveying Equipment? What are its Design P
Understanding the fundamental concepts and design principles of negative pressure suction type powder pneumatic conveying equipment is crucial for industries dealing with bulk powder handling. This equipment is engineered to efficiently transport dry powders and granular materials through a pipeline system using air as the conveying medium. The negative pressure suction method offers distinct advantages in certain applications, such as minimizing product contamination and enabling safe handling of sensitive materials. By creating a vacuum within the conveying line, these systems draw powder from the source into the pipeline, ensuring reliable and consistent material transport. The design of negative pressure suction equipment is tailored to meet the specific requirements of various industries, including pharmaceuticals, food processing, and chemical manufacturing.
Design Principles of Negative Pressure Suction Type Powder Pneumatic Conveying Systems
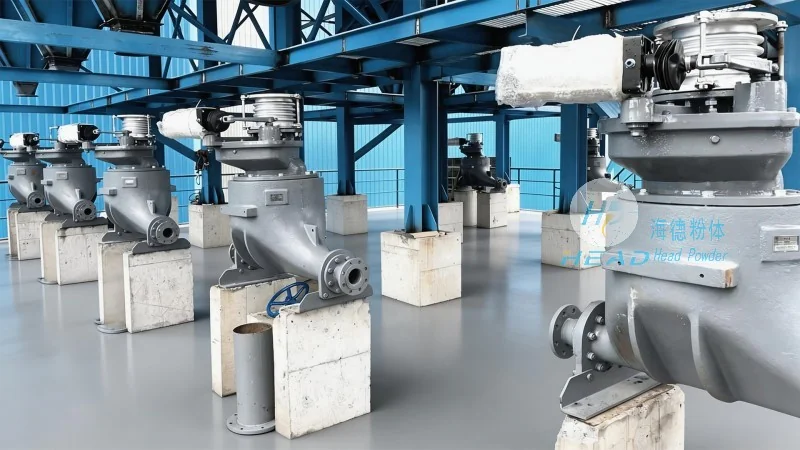
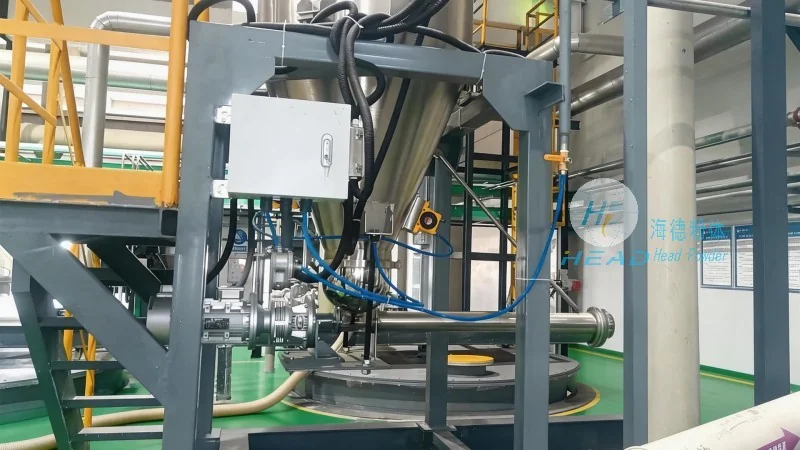
The core design principle of negative pressure suction conveying systems is the creation of a vacuum within the conveying line. This vacuum is generated by a suction fan or blower, which draws air and the powder mixture into the system. The equipment typically consists of a hopper for material storage, a suction nozzle or inlet where the material is introduced, a pipeline network, and a filter or separator to separate the powder from the air at the discharge end. The design emphasizes maintaining consistent air flow rates and pressure differentials to ensure reliable and efficient material transport. Key components include the suction fan, which provides the necessary negative pressure, and the material feed system, which controls the rate of powder introduction into the pipeline. The system is engineered to minimize pressure losses and ensure that the powder remains in suspension throughout the conveying process, preventing blockages and ensuring smooth operation.
How Negative Pressure Suction Conveying Works
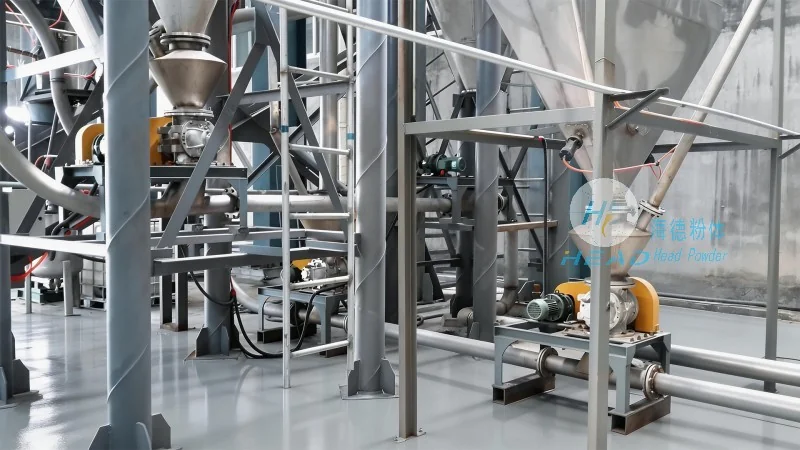
In operation, the suction fan creates a lower pressure inside the conveying line compared to the ambient environment. This pressure differential draws the powder from the source (such as a hopper or storage bin) into the pipeline along with the air. The mixture travels through the pipeline to the discharge point, where a separator or filter captures the powder and returns the air to the system or releases it to the atmosphere. The design ensures that the air flow is sufficient to maintain the powder in suspension, preventing agglomeration and ensuring efficient transport. The negative pressure system is particularly effective for applications requiring low contamination levels, as it prevents external air from entering the system and contaminating the product. This makes it ideal for handling materials that are hygroscopic or sensitive to moisture, as well as for processes where product purity is paramount.
About Shandong HeadPowder Engineering Co., Ltd.
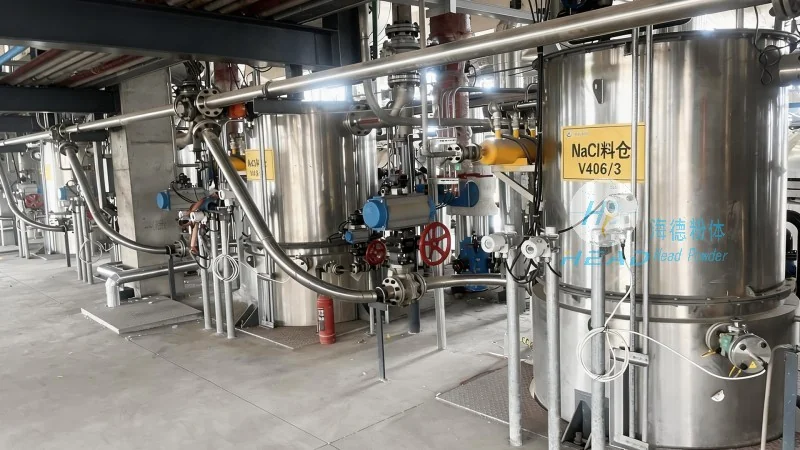
HeadPowder, the brand under Shandong HeadPowder Engineering Co., Ltd., specializes in the design, manufacturing, and supply of advanced powder handling equipment. With a focus on innovative solutions for bulk material transport, HeadPowder leverages decades of industry experience to deliver high-quality negative pressure suction type powder pneumatic conveying systems. The company's facilities are located in Shandong, China, where it combines cutting-edge technology with rigorous quality control to meet the diverse needs of global clients across various industries, including pharmaceuticals, food processing, and chemical manufacturing. HeadPowder's commitment to excellence ensures that each equipment is tailored to the specific operational requirements of the client, providing reliable and efficient powder handling solutions that enhance productivity and product quality.