What is a Ton Bag Unloading Station Material Handling System? What are the Design Principles?
Release time:2026-09-15 00:03:24
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
A ton bag unloading station material handling system is a specialized industrial setup designed to efficiently receive, store, and transfer bulk materials from large, heavy-duty bags, commonly known as ton bags or super sacks. These systems are integral to various industries, including chemical, food processing, and mining, where handling large volumes of raw materials is essential for operational efficiency. The core function of such a system is to automate the process of unloading ton bags, reducing manual labor, minimizing material loss, and enhancing overall workflow safety and productivity.
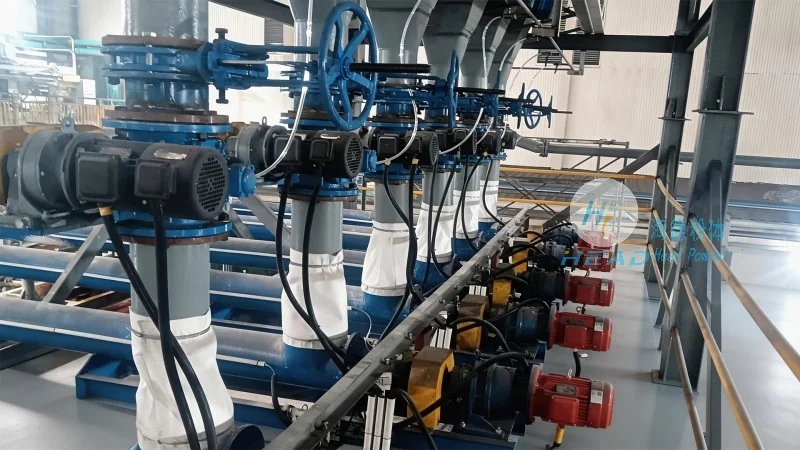
Key Components of a Ton Bag Unloading Station
The design of a ton bag unloading station material handling system typically involves several critical components that work in tandem to achieve seamless material transfer. The primary components include:
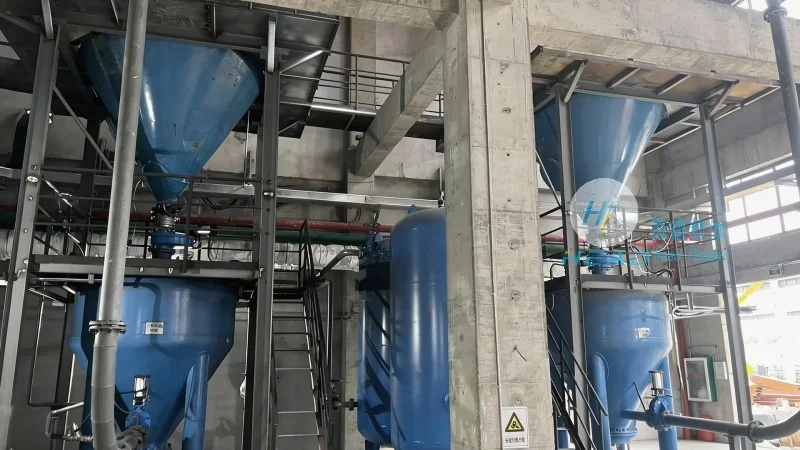
- Ton Bag Hoist or Lift: This equipment is responsible for lifting the heavy ton bag from the ground or a loading vehicle to a higher elevation, allowing for easier access to the bag's opening. The hoist is usually equipped with a robust lifting mechanism, such as a chain or hydraulic system, capable of handling the significant weight of a full ton bag.
- Unloading Spout or Discharge Valve: Once the ton bag is elevated, the unloading spout or discharge valve is used to open the bag and allow the material to flow out. This component is often designed with a flexible or adjustable nozzle to direct the material into the next stage of the handling process, such as a conveyor or storage hopper.
- Conveyor System: After the material is discharged from the ton bag, a conveyor system is used to transport the material to a storage silo, processing unit, or other destination. The conveyor may be a belt conveyor, screw conveyor, or pneumatic conveyor, depending on the material characteristics and application requirements.
- Storage Hopper or Silo: The material is often transferred into a storage hopper or silo, which serves as a buffer to regulate the flow of material and prevent overloading downstream equipment. The hopper is typically designed with a sloped bottom to facilitate smooth material discharge.
- Control System: An automated control system is integrated into the ton bag unloading station to manage the operation of all components. This system may include sensors, programmable logic controllers (PLCs), and human-machine interfaces (HMIs) to monitor the process, adjust parameters, and ensure safe and efficient operation.
Design Principles for Efficient Material Handling
The design of a ton bag unloading station material handling system follows several key principles to ensure optimal performance, safety, and cost-effectiveness. These principles are tailored to the specific requirements of the material being handled and the operational environment. The primary design principles include:
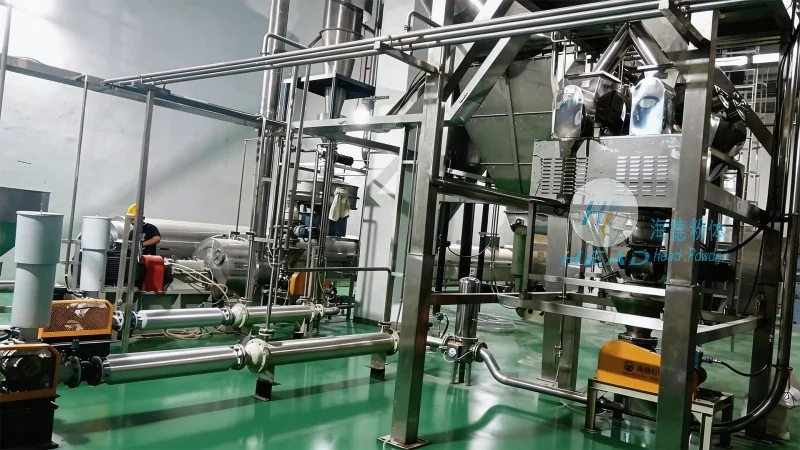
- Material Compatibility: The system is designed to handle a wide range of bulk materials, from free-flowing powders to cohesive or abrasive substances. The choice of materials for components such as the hoist, conveyor, and discharge valve is critical to prevent wear and tear and ensure long-term reliability.
- Load Capacity and Durability: The entire system is engineered to withstand the heavy loads associated with ton bags, which can weigh several hundred kilograms. The components are constructed from high-strength materials, such as steel or reinforced polymers, to ensure durability and longevity.
- Automation and Safety: Automation is a key design principle, as it reduces the risk of human error and improves operational safety. The control system is designed with safety features, such as emergency stop buttons, overload protection, and material detection sensors, to prevent accidents and protect personnel.
- Space Efficiency: The system is designed to fit within the available space in the industrial facility, optimizing the use of floor area and minimizing the need for additional infrastructure.
- Integration with Existing Infrastructure: The ton bag unloading station is designed to integrate seamlessly with existing material handling equipment, such as conveyors, storage silos, and processing units, to create a cohesive and efficient material flow system.
Applications and Benefits of Ton Bag Unloading Stations
Ton bag unloading stations are widely used in various industries to handle bulk materials efficiently. Some common applications include:
- Chemical Industry: Handling chemicals, fertilizers, and other industrial powders in large quantities.
- Food Processing: Processing and storing food ingredients, such as flour, sugar, and grains.
- Mining and Minerals: Unloading and transferring ore, minerals, and other raw materials from mining operations.
- Pharmaceutical Industry: Handling pharmaceutical powders and raw materials in a controlled environment.
The benefits of using a ton bag unloading station material handling system include:
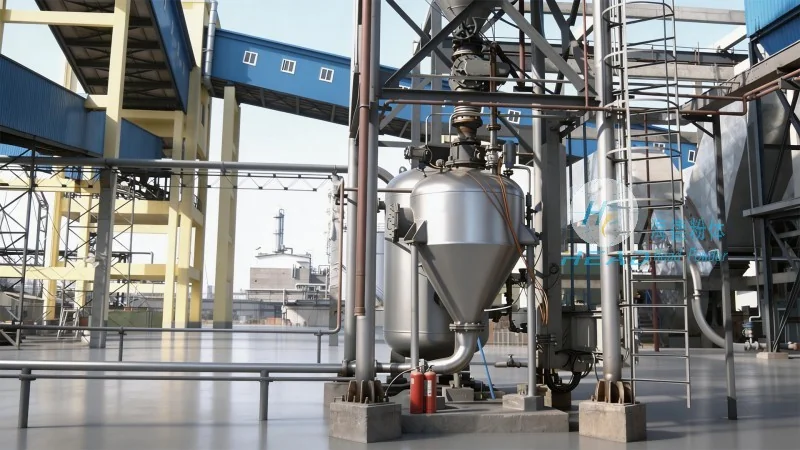
- Increased Productivity: Automation reduces the time required to unload ton bags, allowing for faster material processing and higher throughput.
- Reduced Labor Costs: The system minimizes the need for manual labor, reducing labor costs and the risk of workplace injuries.
- Improved Material Handling Efficiency: The system ensures consistent and controlled material flow, reducing material loss and improving overall operational efficiency.
- Enhanced Safety: Automation and safety features reduce the risk of accidents and improve workplace safety.
- Scalability: The system can be scaled to handle increasing volumes of material as the business grows.
Conclusion and Company Overview
A ton bag unloading station material handling system is a critical component of modern industrial operations, designed to efficiently handle large volumes of bulk materials. The system's design, incorporating robust components and automated controls, ensures optimal performance, safety, and cost-effectiveness. Shandong HeadPowder Engineering Co., Ltd., a leading engineering company based in China, specializes in designing and manufacturing such systems tailored to the specific needs of various industries. With a focus on quality, innovation, and customer satisfaction, HeadPowder provides comprehensive solutions for material handling challenges, helping businesses improve their operational efficiency and productivity.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China
