

What is a Tonne Bag Dust-Free Feeding Station Material Pneumatic Conveying Line? What are its Design
For industrial facilities dealing with bulk materials, efficient and safe material handling is crucial. A tonne bag dust-free feeding station with a material pneumatic conveying line represents a sophisticated solution designed to address these challenges. This system integrates several key components to ensure seamless, dust-free transfer of bulk materials from storage to processing areas.
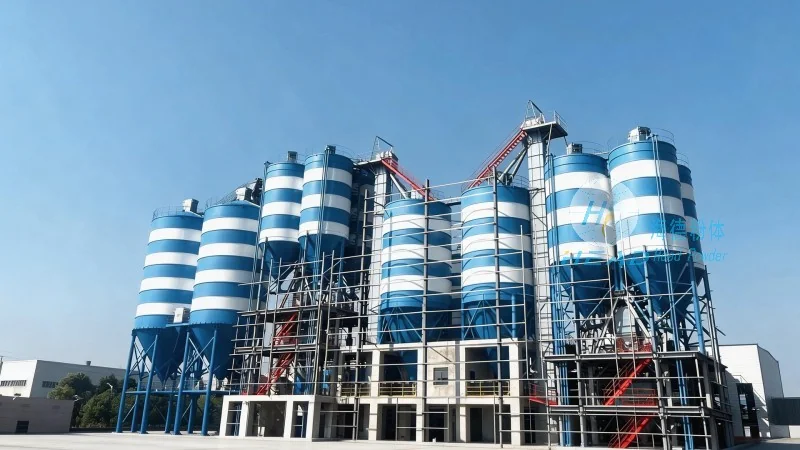
Understanding the Tonne Bag Dust-Free Feeding Station
The tonne bag dust-free feeding station is a critical component of the material handling system. It is specifically designed to handle large bulk bags (tonne bags) and transfer their contents into the pneumatic conveying line without generating dust or contamination. The station typically includes a hopper or receiving bin that opens the tonne bag and feeds the material into the conveying system. This design ensures that the material is transferred in a controlled manner, minimizing dust exposure and maintaining product integrity.
Pneumatic Conveying Line Design Principles
The pneumatic conveying line is the core of the material transport mechanism. It uses air pressure to move bulk materials through a pipeline system. The design principles of this line involve several key factors to ensure efficient operation. First, the selection of the right type of pneumatic conveying system—such as positive pressure or negative pressure—depends on the material characteristics, such as particle size, moisture content, and flowability. Positive pressure systems are commonly used for long-distance or high-capacity transport, while negative pressure systems are suitable for short distances or when dust control is a priority.
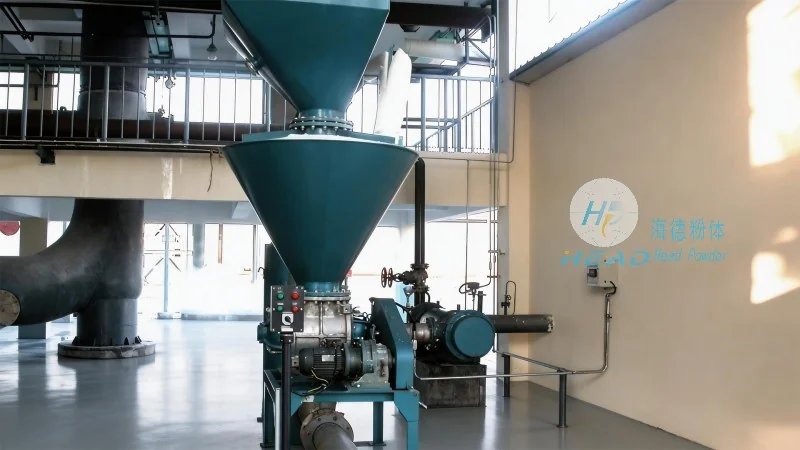
Key Components and Their Functions
Several key components make up the tonne bag dust-free feeding station and pneumatic conveying line. The receiving hopper or bin is the first component, which opens the tonne bag and feeds the material into the system. Next is the feeder, which controls the flow rate of the material into the conveying line. The conveying line itself consists of pipes, valves, and a blower or vacuum pump that generates the air pressure needed for material transport. The system may also include filters and dust collectors to ensure that any airborne particles are captured and returned to the material stream or disposed of properly.
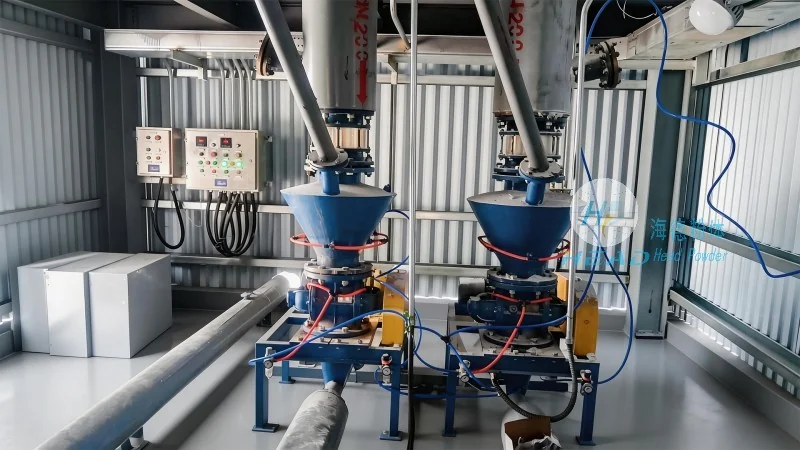
Benefits of the System
Implementing a tonne bag dust-free feeding station with a pneumatic conveying line offers numerous benefits for industrial operations. Firstly, it significantly reduces dust generation, improving workplace safety and compliance with environmental regulations. Secondly, it enhances material handling efficiency by automating the transfer process, reducing manual labor and the risk of material loss or contamination. Thirdly, the system maintains product quality by preventing cross-contamination and ensuring consistent material flow. Additionally, it can be integrated with other processing equipment, such as mixers or reactors, to form a complete material handling system.
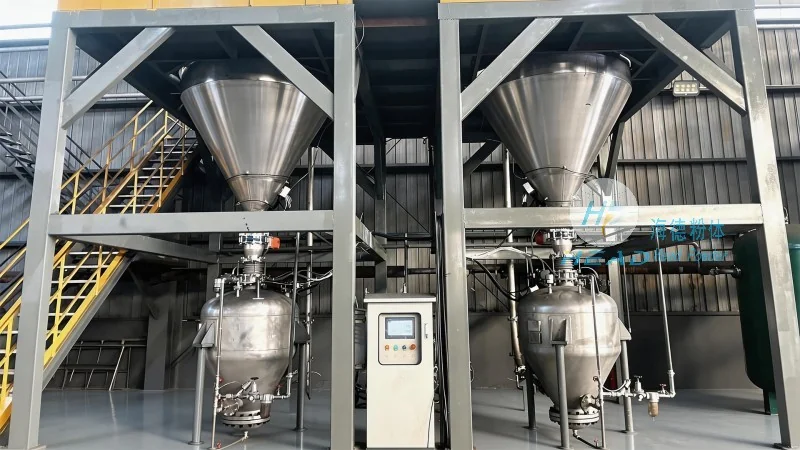
Application in Different Industries
This type of system is widely used in various industries, including pharmaceuticals, food processing, chemicals, and minerals. In the pharmaceutical industry, for example, the dust-free design is essential to maintain sterile conditions and prevent contamination of sensitive products. In the food industry, it ensures that bulk ingredients are handled hygienically and without cross-contamination. In the chemical industry, it allows for the safe transfer of hazardous materials while minimizing exposure risks. The versatility of the system makes it suitable for a wide range of applications where bulk material handling is required.
Conclusion
The tonne bag dust-free feeding station with a material pneumatic conveying line is a highly effective solution for industrial bulk material handling. By combining dust-free feeding technology with pneumatic conveying, it offers a reliable and efficient method to transport materials while maintaining safety and product quality. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing such systems to meet the specific needs of various industries. With their expertise and commitment to quality, they ensure that clients receive tailored solutions that enhance operational efficiency and compliance with industry standards.