With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Long-distance powder conveying systems are essential in various industrial applications, enabling the efficient transport of bulk powders over significant distances. These systems are designed to handle materials like cement, flour, and other fine particulates, ensuring reliable and consistent material flow. The core of such systems lies in their ability to maintain material integrity while minimizing degradation or segregation during transport. Understanding the components and design principles behind these systems is crucial for optimizing industrial processes and enhancing operational efficiency.
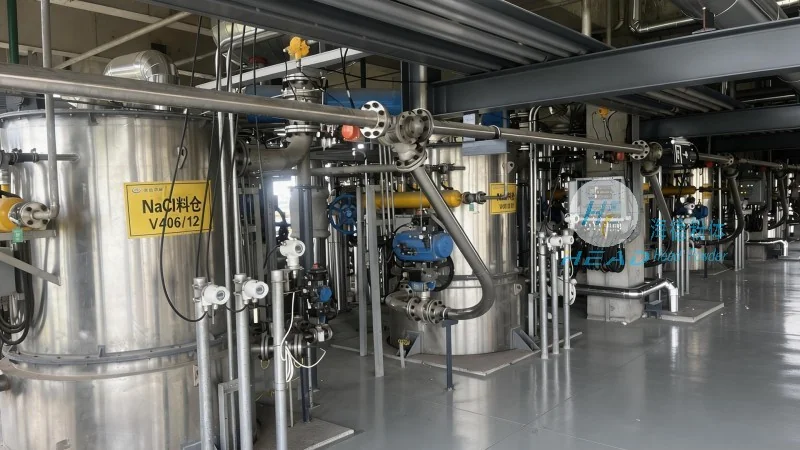
Long-distance powder conveying systems are engineered to transport bulk powders from a source to a destination over considerable distances, often ranging from several hundred meters to several kilometers. These systems are widely used in industries such as cement production, food processing, chemical manufacturing, and mining. The primary goal is to achieve a continuous, controlled, and efficient transfer of material without compromising its quality or properties. The design of these systems must consider factors like material characteristics, distance, and operational requirements to ensure optimal performance.
The long-distance powder conveying system typically consists of several critical components that work in tandem to facilitate material transport. These components include the feed hopper, which stores and feeds the powder into the system; the conveyor itself, which can be either pneumatic or mechanical; the control valves and regulators that manage the flow rate and pressure; and the discharge hopper or silo at the receiving end. Each component plays a vital role in maintaining the integrity of the powder and ensuring smooth operation.
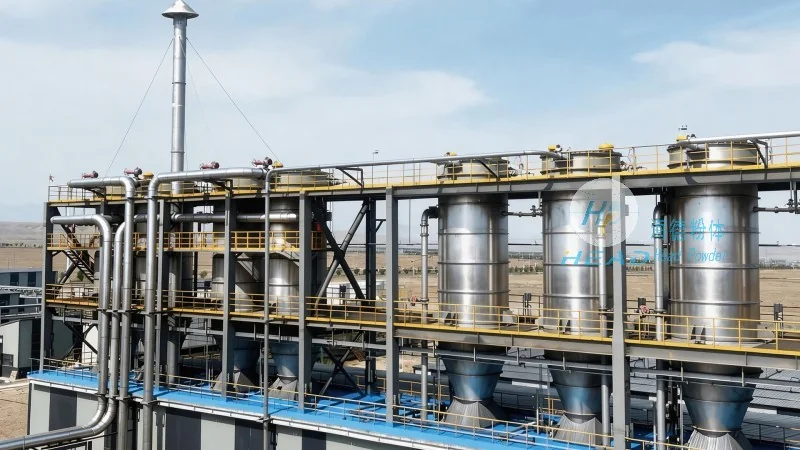
The design principles of long-distance powder conveying systems are centered on several key factors to ensure reliability and efficiency. First, the system must be capable of handling the specific characteristics of the powder, such as particle size, density, and moisture content. This involves selecting appropriate materials for the conveyor components to prevent wear and tear. Second, the system must maintain consistent pressure and flow rates to avoid material degradation or blockages. This is achieved through the use of advanced control systems and pressure sensors. Third, the design must consider the distance and elevation changes to ensure that the system can handle the required head and flow rates without excessive energy consumption. Proper sealing and maintenance are also critical to prevent dust emissions and ensure long-term operation.
Long-distance powder conveying systems find applications in a wide range of industries, each benefiting from the system's ability to transport bulk materials efficiently. In the cement industry, these systems are used to transport raw materials and finished products over long distances, improving production line efficiency. In the food industry, they are employed to convey flour, sugar, and other ingredients, ensuring hygienic and consistent material handling. In chemical manufacturing, they help transport powders like pigments and additives, maintaining product quality. The benefits of these systems include reduced labor costs, minimized material loss, improved safety by eliminating manual handling, and enhanced overall operational efficiency.
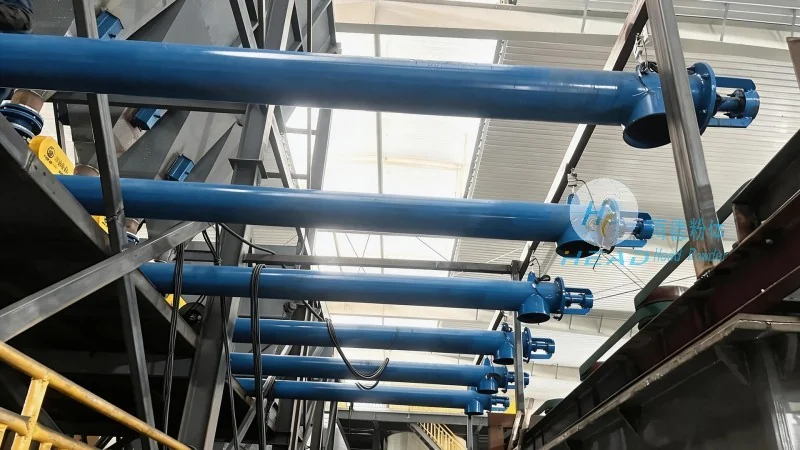
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of long-distance powder conveying systems and related equipment. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner in the industrial sector. The company is headquartered in Shandong, China, and specializes in designing, manufacturing, and installing customized powder conveying solutions tailored to the specific needs of its clients. HeadPowder's commitment to excellence is reflected in its adherence to international standards and its use of advanced technology in product development. The company's team of experienced engineers and technicians ensures that each system is designed to meet the highest performance and reliability standards, providing clients with durable and efficient solutions for their powder handling needs.
Long-distance powder conveying systems are indispensable in modern industrial operations, offering a reliable and efficient means of transporting bulk powders over significant distances. The design principles and components of these systems are carefully engineered to ensure optimal performance, material integrity, and operational efficiency. Companies like Shandong HeadPowder Engineering Co., Ltd. play a crucial role in providing advanced solutions that meet the evolving needs of various industries. By understanding the design and functionality of these systems, businesses can enhance their production processes, reduce costs, and improve overall operational performance.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top