With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Efficient and reliable powder handling is a critical aspect of modern industrial operations, particularly in sectors such as cement, chemical, and food processing. The gray warehouse powder conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution designed to address the challenges of transporting bulk powders with precision and efficiency. This article provides an overview of the system's structure and operational principles, highlighting its key components and the engineering advancements that make it a preferred choice in the industry.
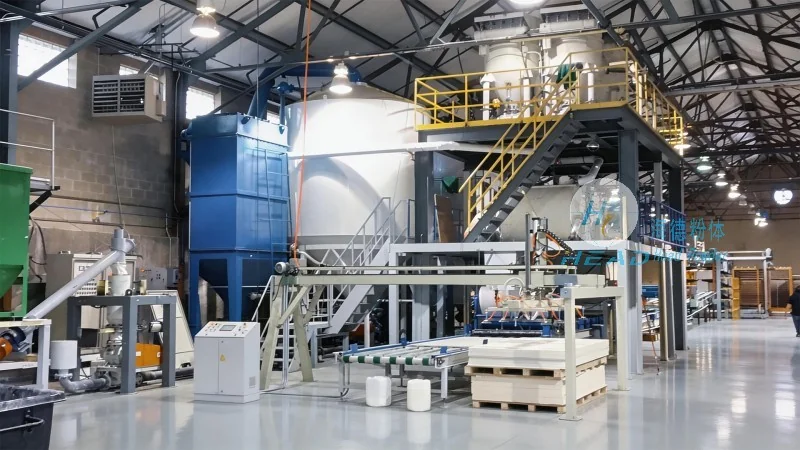
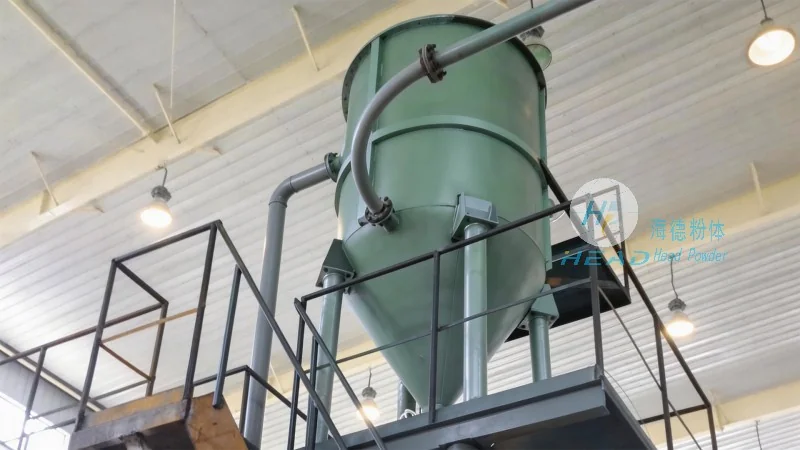
The gray warehouse powder conveying system is a comprehensive setup that integrates multiple functional units to ensure seamless powder movement from storage to processing areas. At its heart, the system comprises several key components, each playing a vital role in the overall operation. The primary components include the storage silo, which serves as the initial holding tank for bulk powders; the conveying equipment, such as screw conveyors or pneumatic systems, responsible for transporting the material; and the control panel, which manages the entire process through automated controls. Additionally, the system may incorporate accessories like feeders, valves, and dust collection units to enhance safety and operational efficiency.
The structural design of the gray warehouse powder conveying system is engineered to maximize space utilization and minimize material loss. The storage silo is typically constructed from durable materials like steel or reinforced concrete, ensuring resistance to corrosion and wear from abrasive powders. The conveying components are strategically positioned to create a continuous flow path, reducing the need for manual intervention and enhancing operational consistency. The operational principle revolves around the controlled release of powder from the silo, followed by the transfer through the conveying equipment to the desired destination. This process is often automated, with sensors and control systems monitoring flow rates, pressure, and other critical parameters to maintain optimal performance. The system's design also emphasizes safety, incorporating features like explosion-proof mechanisms and dust suppression systems to mitigate risks associated with powder handling.
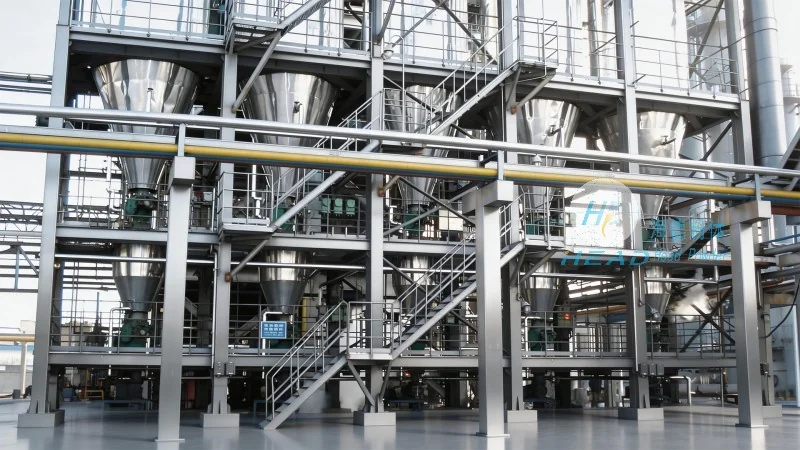
Shandong HeadPowder Engineering Co., Ltd. leverages advanced engineering techniques to enhance the performance of the gray warehouse powder conveying system. The company focuses on customizing solutions to meet the specific needs of each client, considering factors such as powder characteristics, processing requirements, and facility layout. For instance, the system can be adapted to handle various types of powders, including fine, coarse, or hygroscopic materials, by adjusting the conveying speed and equipment configuration. The integration of modern technologies, such as variable frequency drives (VFDs) and intelligent control systems, allows for precise control over the conveying process, improving energy efficiency and reducing operational costs. Furthermore, the system's modular design enables easy maintenance and upgrades, ensuring long-term reliability and minimal downtime.
The gray warehouse powder conveying system finds extensive applications across multiple industries, where efficient bulk powder handling is essential. In the cement industry, it facilitates the transport of raw materials and finished products, improving production throughput and reducing material handling time. In the chemical sector, the system ensures safe and controlled transfer of reactive powders, minimizing the risk of accidents and environmental contamination. The food processing industry also benefits from this technology, as it enables the hygienic handling of food-grade powders while maintaining compliance with regulatory standards. By optimizing powder flow and reducing operational inefficiencies, the system contributes to increased productivity and cost savings for businesses in these sectors.
Shandong HeadPowder Engineering Co., Ltd. stands as a leading provider of advanced powder handling solutions, with the gray warehouse powder conveying system being a prime example of their engineering expertise. The company's commitment to innovation, quality, and customer satisfaction has established it as a trusted partner in the industry. By combining robust structural design with intelligent operational principles, the system offers a reliable and efficient means of managing bulk powders, addressing the evolving needs of modern industrial operations. As businesses continue to seek more effective and sustainable solutions for powder handling, the gray warehouse powder conveying system remains a key technology in enhancing operational performance and ensuring safety in various industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top