With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Mineral sand, a vital raw material in industries like mining, construction, and chemical processing, demands efficient and reliable powder conveying solutions to manage its bulk transportation. Traditional methods, such as manual handling or basic mechanical conveyors, often result in inefficiencies, material loss, or safety risks. HeadPowder, a leading provider in the field, specializes in advanced powder conveying systems tailored to the unique characteristics of mineral sand, ensuring seamless and safe operation.
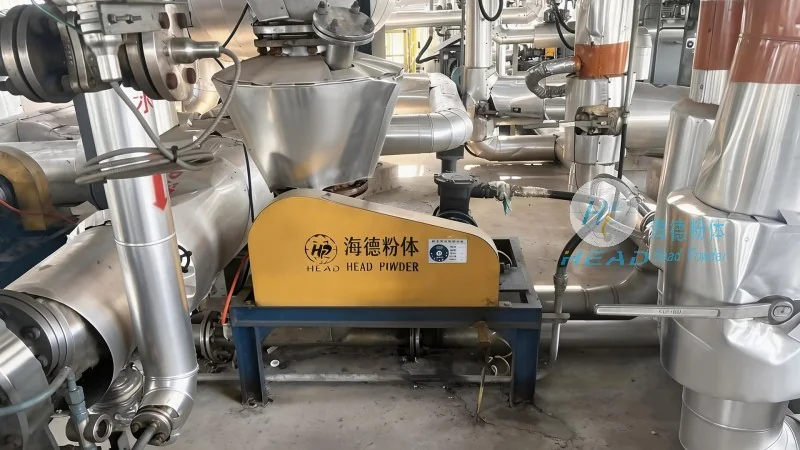
The core of a mineral sand powder conveying system consists of integrated components that work in unison to achieve optimal performance. Key elements include the feed hopper, which stores and regulates the flow of mineral sand; the conveying medium (e.g., air or mechanical force), which propels the powder through the system; and the discharge unit, which delivers the material to the target location. The working principle typically involves the feed hopper releasing the sand into the conveying path, where the medium creates a pressure differential to move the particles. This process ensures consistent and controlled movement, minimizing segregation and degradation of the material.
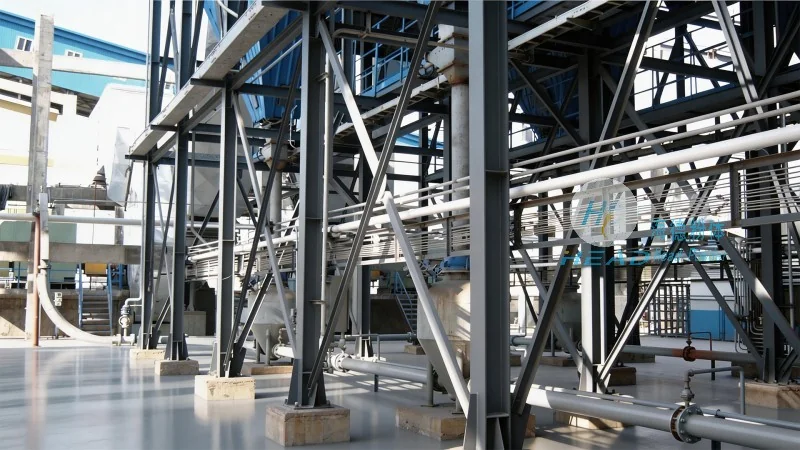
The operation process of a mineral sand powder conveying system follows a systematic sequence to maintain efficiency and reliability. Initially, the feed hopper is filled with mineral sand, and the system is activated to start the conveying cycle. The material is then drawn into the conveying line by the moving medium, traveling through pipes or ducts to the discharge point. During transit, the system continuously monitors flow rates and pressure, adjusting parameters as needed to prevent blockages or overloading. At the discharge end, the sand is released into a collection bin or processing unit, completing the cycle. This process is typically automated, with control panels allowing operators to adjust settings for different sand types or operational conditions.
HeadPowder's mineral sand powder conveying systems offer technical advantages that enhance performance and adaptability. These include high conveying efficiency, with minimal material loss and degradation, due to gentle handling and optimized flow dynamics. The systems are highly adaptable, capable of handling a wide range of particle sizes and moisture contents common in mineral sands. Additionally, they provide excellent dust control, reducing environmental impact and improving workplace safety. Applications span multiple sectors, including mining operations for transporting ore concentrates, construction material plants for handling sand and gravel, and chemical facilities for processing mineral-based powders.
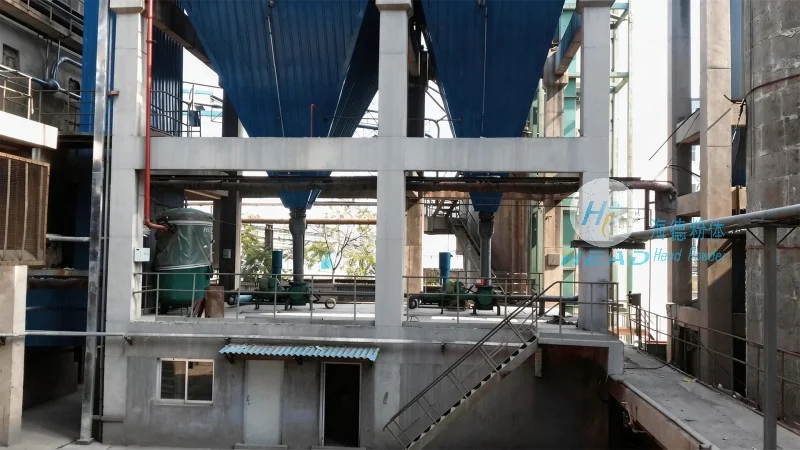
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a reputable enterprise based in Shandong, China. The company specializes in the design, manufacturing, and installation of advanced powder handling and conveying systems, with a focus on mineral sand and other bulk materials. HeadPowder leverages years of industry experience and cutting-edge technology to deliver customized solutions that meet the specific needs of clients. The company's commitment to quality and customer satisfaction has established it as a trusted partner in the bulk material handling sector, serving clients both domestically and internationally.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top