With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. This article provides a comprehensive overview of a dolomite pneumatic conveying system, highlighting its key components, operational principles, and practical applications.
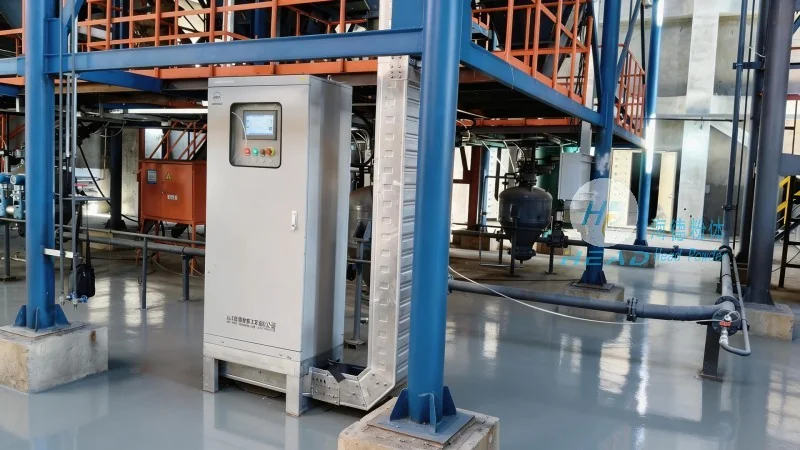
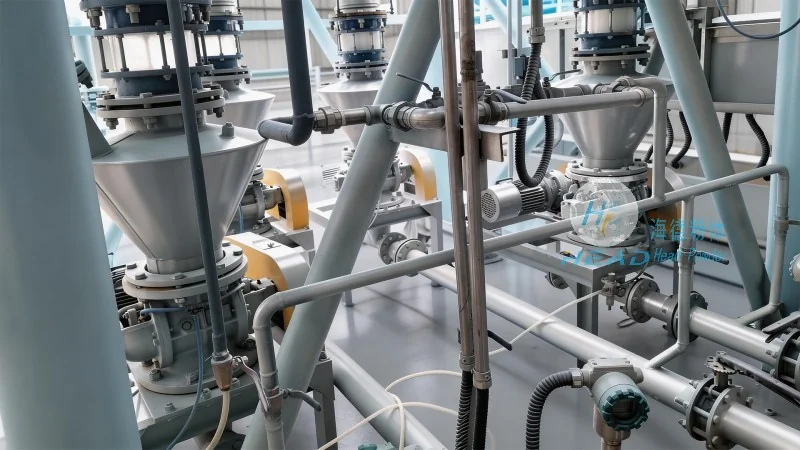
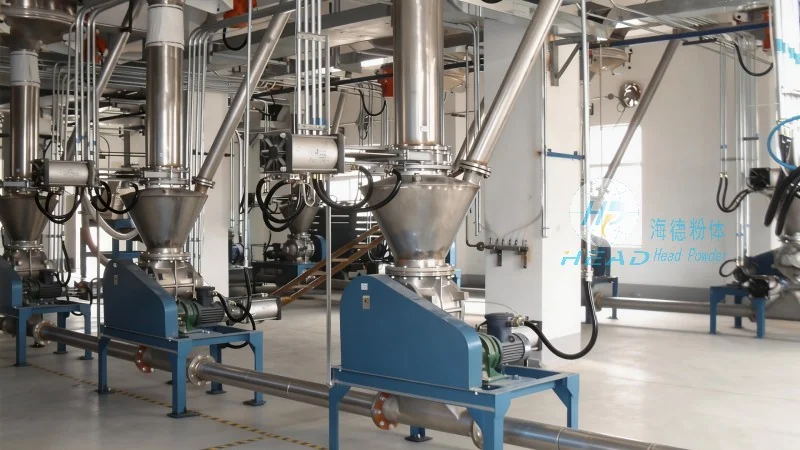
The dolomite pneumatic conveying system is engineered with precision to ensure efficient material handling. The core components include a hopper for material storage, a rotary airlock valve for controlled discharge, a positive displacement blower or a high-pressure air compressor to generate the necessary airflow, and a pipeline network that transports the material. Additionally, the system may incorporate a filter unit to capture any fine particles and a dust collector to maintain air quality. Each component is selected based on the specific characteristics of dolomite, such as its particle size, density, and flowability, ensuring optimal performance.
The operation of the dolomite pneumatic conveying system follows a systematic process. Initially, dolomite is fed into the hopper from a storage silo or a bulk container. The rotary airlock valve regulates the flow of material into the pipeline, preventing backflow and maintaining consistent material feed. The positive displacement blower then generates a high-pressure airflow, which is directed into the pipeline. As the air flows through the system, it entrains the dolomite particles, creating a slurry-like mixture that moves through the pipeline to the destination point. At the receiving end, a cyclone separator or a rotary valve separates the material from the air, allowing the dolomite to be discharged into a storage bin or a processing unit. The air, now filtered to remove any residual particles, is then released back into the environment or recirculated if necessary.
Implementing a pneumatic conveying system for dolomite offers several advantages over traditional methods like belt conveyors or bucket elevators. Firstly, it eliminates the need for mechanical contact with the material, reducing wear and tear on equipment and minimizing the risk of contamination. Secondly, the system provides a dust-free and hygienic environment, which is crucial for industries where product purity is essential, such as food processing or pharmaceutical manufacturing. Thirdly, the system is highly flexible, allowing for changes in material flow rates and destinations without significant modifications to the infrastructure. Additionally, the compact design of the system saves space, making it suitable for facilities with limited floor area. The energy efficiency of modern pneumatic conveying systems also contributes to lower operational costs over time.
Dolomite, a calcium magnesium carbonate mineral, is widely used in various industries due to its chemical properties and physical characteristics. The pneumatic conveying system is particularly beneficial in applications where dolomite needs to be transported over long distances or through complex layouts. Industries that commonly utilize dolomite pneumatic conveying systems include cement production, where dolomite is used as a raw material for clinker; steel manufacturing, where it serves as a flux to control the chemical composition of the melt; and chemical processing, where it is used as a filler or a reagent in various products. The system's ability to handle large volumes of material efficiently makes it an ideal solution for these applications.
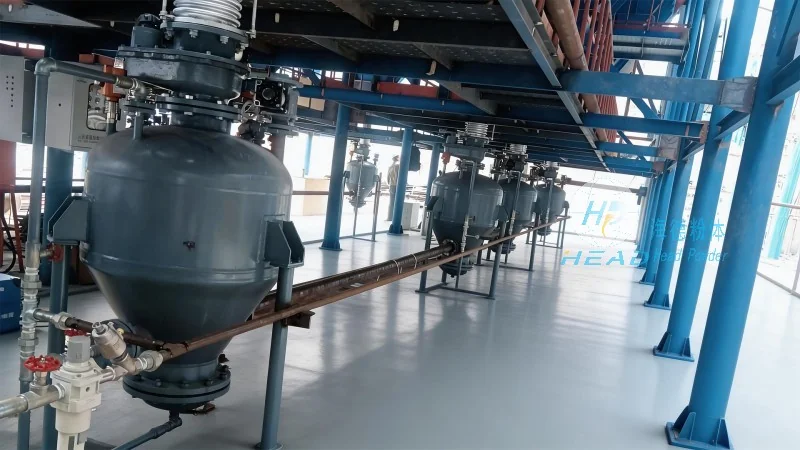
Proper installation and regular maintenance are critical to the longevity and performance of the dolomite pneumatic conveying system. During installation, the system must be aligned correctly to ensure smooth airflow and prevent blockages. The pipeline should be properly supported to avoid sagging, which could lead to air leaks or material buildup. The rotary airlock valves and the blower must be properly sized to handle the specific flow rate and pressure requirements of the dolomite. Regular maintenance involves checking the condition of the filter and dust collector, cleaning or replacing filters as needed, inspecting the blower for wear and tear, and lubricating moving parts. Additionally, periodic inspections of the pipeline for any signs of corrosion or damage are necessary to prevent system failures. By adhering to a regular maintenance schedule, the system can operate efficiently and reliably for many years.
In conclusion, the dolomite pneumatic conveying system is a sophisticated and efficient solution for handling dolomite in various industrial applications. HeadPowder, with its expertise in engineering and manufacturing, provides high-quality systems that meet the specific needs of clients. By understanding the key components, operational principles, and maintenance requirements, industries can leverage the benefits of pneumatic conveying to improve their material handling processes, reduce costs, and enhance overall productivity. The system's flexibility, efficiency, and reliability make it a preferred choice for many businesses dealing with dolomite and other similar materials.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top