With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the working principle and characteristics of bicarbonate powder pneumatic conveying is crucial for industries that rely on efficient and reliable material handling solutions. This article delves into the technical aspects, operational benefits, and key features of this process, providing a comprehensive overview for professionals in the field.
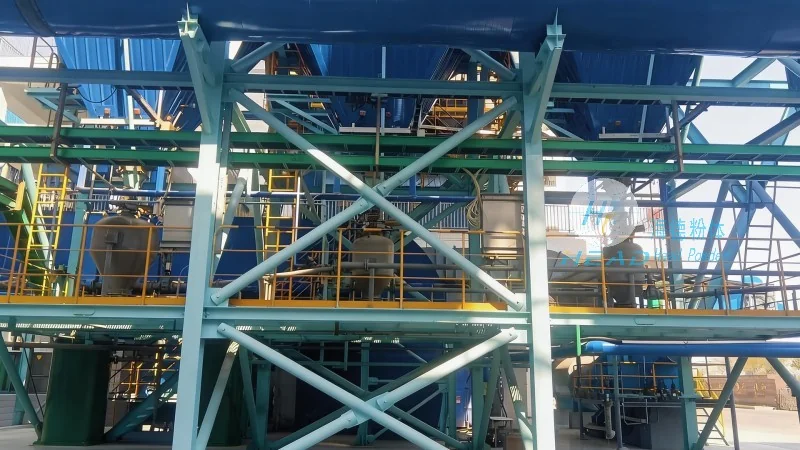
Bicarbonate powder, commonly known as sodium bicarbonate, is a widely used chemical in various industrial applications, including food processing, pharmaceuticals, and manufacturing. Pneumatic conveying is a method used to transport dry powders like bicarbonate through a pipeline using air or gas as the conveying medium. This technology offers several advantages over traditional mechanical conveying systems, such as reduced equipment wear, improved safety, and enhanced process control.
The core mechanism of bicarbonate powder pneumatic conveying involves the use of a blower or compressor to generate airflow within a sealed pipeline. The powder is introduced into the system at the feed point, where it is entrained by the moving air and transported to the discharge point. There are two primary types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems operate at higher velocities, typically 20-30 meters per second, and are suitable for short distances and low to medium particle sizes. Dense-phase systems, on the other hand, use lower velocities (5-15 meters per second) and higher pressure to achieve more controlled and gentle material transport, minimizing particle degradation and product loss.
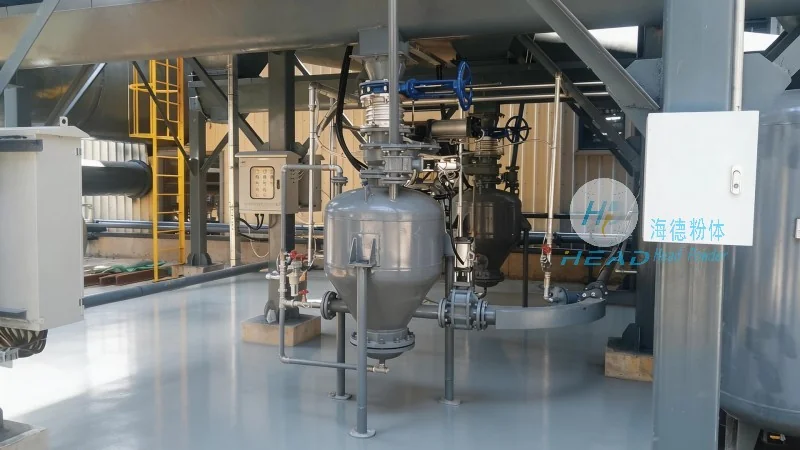
Several distinct characteristics define the performance of bicarbonate powder pneumatic conveying systems. First, the system's efficiency in terms of energy consumption and material throughput is a critical factor. Modern designs optimize airflow and pressure to minimize energy use while maintaining high conveying rates. Second, the system's ability to handle varying particle sizes and moisture content is essential for consistent performance. Bicarbonate powders can have different particle distributions, and the conveying system must be configured to accommodate these variations without clogging or degradation. Third, the system's safety features are paramount, as handling powders can pose dust explosion risks. Proper ventilation, explosion-proof components, and material selection are integral to ensuring safe operation. Additionally, the system's flexibility in terms of layout and integration with other process equipment is a significant advantage, allowing for customized solutions tailored to specific industrial needs.
Implementing bicarbonate powder pneumatic conveying offers numerous benefits for industrial operations. One of the most notable advantages is the reduction in equipment wear and maintenance compared to mechanical systems. Since there are no moving parts in direct contact with the powder, the risk of wear and tear is significantly lower. This leads to lower maintenance costs and longer equipment lifespan. Another advantage is the improved product quality and integrity. The gentle handling of the powder minimizes particle breakage and agglomeration, preserving the physical and chemical properties of the bicarbonate. This is particularly important in applications where the powder's purity and particle size distribution are critical, such as in food and pharmaceutical industries. Furthermore, the system's ability to handle dusty environments and prevent cross-contamination is a key benefit. By containing the powder within a sealed pipeline, the risk of dust exposure and contamination is minimized, enhancing workplace safety and compliance with regulatory standards.
Bicarbonate powder pneumatic conveying is widely adopted across various industries due to its versatility and efficiency. In the food industry, it is used for transporting baking soda in baking and food processing plants. The gentle handling ensures that the powder remains in optimal condition for use in products like bread, cookies, and other baked goods. In the pharmaceutical sector, the system is employed to convey raw materials and finished products, maintaining strict hygiene and contamination control. The sealed pipeline and controlled airflow prevent cross-contamination, which is essential for pharmaceutical manufacturing. Additionally, in the chemical and manufacturing industries, bicarbonate powder is used in processes such as coating, cleaning, and chemical reactions. The ability to transport the powder to specific locations within a plant without the need for manual handling enhances operational efficiency and safety.
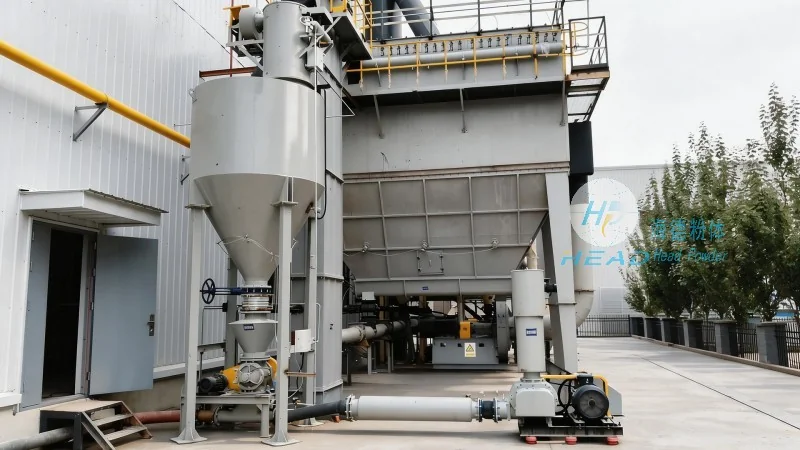
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized engineering solutions for powder handling and conveying systems. With a focus on innovation and customer-centric approaches, the company has established itself as a trusted partner in the industry. Headpowder specializes in designing, manufacturing, and installing pneumatic conveying systems tailored to the unique needs of clients, including those handling bicarbonate powders. The company's expertise lies in understanding the specific challenges of powder handling, such as particle size variations, moisture content, and material properties, and developing customized solutions that address these challenges effectively. Headpowder's commitment to quality and reliability ensures that its systems meet the highest standards of performance and safety, providing long-term value to its clients.
In summary, bicarbonate powder pneumatic conveying is a sophisticated and efficient method for transporting dry powders, offering numerous advantages over traditional conveying systems. The working principle, which involves the use of air to entrain and transport the powder, combined with its key characteristics such as efficiency, safety, and flexibility, makes it an ideal solution for various industrial applications. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing advanced pneumatic conveying systems that meet the evolving needs of industries, ensuring reliable and safe material handling. As the demand for efficient and sustainable powder handling solutions continues to grow, pneumatic conveying technology will remain a cornerstone in the industry, driving innovation and operational excellence.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top