With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced negative pressure dilute phase material handling equipment. This technology is widely used in various industries for efficient and safe material transport. The following sections will explore the working principle and key features of this equipment, providing a comprehensive understanding of its applications and benefits.
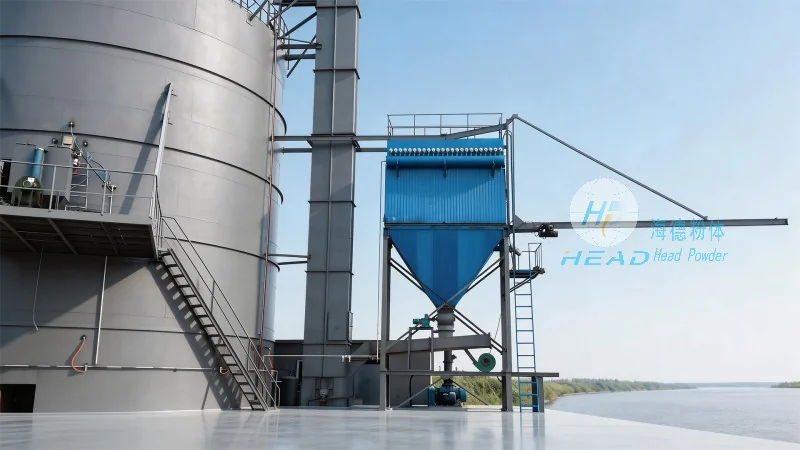
The core of negative pressure dilute phase material handling equipment lies in its ability to create a negative pressure environment within the conveying system. This is achieved through a series of components that work in tandem to draw material from the source and transport it to the destination. The process typically begins with a material feed hopper, where bulk materials are introduced. A fan or blower then generates a low-pressure air stream, which pulls the material particles into the conveying line. The material is suspended in the air stream as a dilute phase, meaning the material particles are dispersed in the air rather than forming a dense flow. This dilute phase allows for high-velocity transport with minimal pressure drop, making it suitable for long-distance and high-capacity applications. The equipment includes key components such as a vacuum pump, airlock valves, and a receiver tank. The vacuum pump maintains the negative pressure, while the airlock valves control the flow of material into and out of the system. The receiver tank collects the conveyed material and can be equipped with a discharge mechanism for further processing. The entire system operates under a controlled negative pressure, ensuring that dust and particles are contained within the system, preventing environmental contamination and maintaining operational safety.
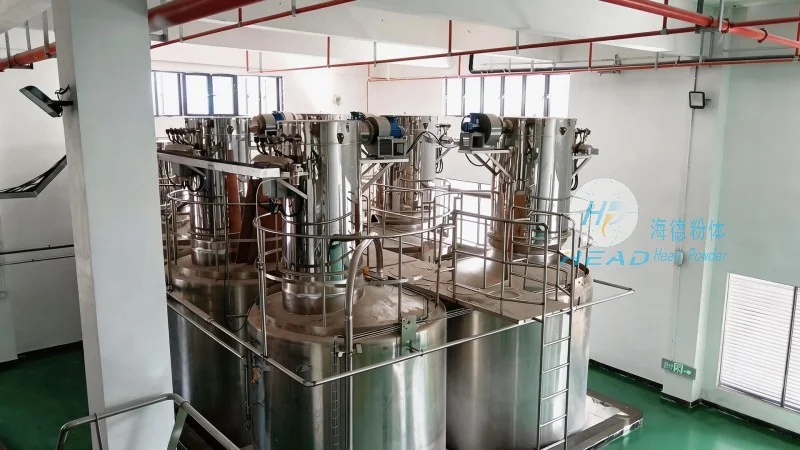
HeadPowder's negative pressure dilute phase material handling equipment offers several distinct advantages that make it a preferred choice in industrial applications. One of the primary features is its high efficiency in material transport. By operating in a dilute phase, the equipment can handle large volumes of material with minimal energy consumption. The low-pressure operation reduces wear and tear on components, leading to lower maintenance costs and longer equipment lifespan. Another significant feature is the ability to handle a wide range of materials, including powders, granules, and fine particles. The negative pressure system effectively captures and transports even the finest particles, ensuring complete material recovery and preventing loss. The equipment also provides excellent dust control, as the entire system operates under a negative pressure, preventing dust emissions into the environment. This feature is crucial for compliance with environmental regulations and maintaining a safe working environment. Additionally, the modular design of the equipment allows for easy integration into existing production lines, with flexible configurations to suit different material types and transport distances. The system's compact footprint and efficient operation make it suitable for both new installations and retrofit applications in various industries, including chemical, pharmaceutical, food processing, and mining.
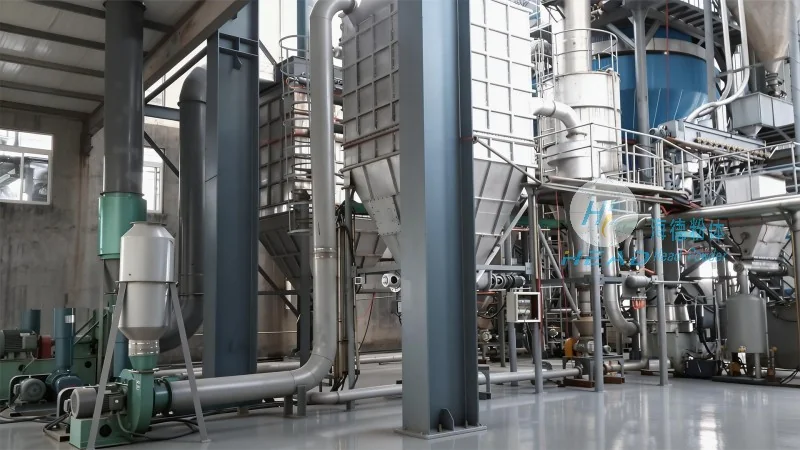
The negative pressure dilute phase material handling equipment from HeadPowder is widely applied in various industrial sectors due to its versatility and efficiency. In the chemical industry, it is used for transporting raw materials and finished products, ensuring a clean and controlled process. The pharmaceutical industry benefits from the equipment's ability to handle sensitive materials with minimal contamination, maintaining product quality and safety standards. The food processing industry utilizes the system for transporting bulk food ingredients, such as flour, sugar, and grains, while adhering to strict hygiene and safety regulations. In the mining sector, the equipment is employed to transport ore and minerals from processing plants to storage facilities, improving operational efficiency and reducing handling time. The benefits of this technology extend beyond material transport, as it also contributes to environmental sustainability by minimizing dust emissions and reducing the need for manual handling, which enhances workplace safety. The equipment's reliability and low maintenance requirements make it a cost-effective solution for long-term industrial operations, providing consistent performance and reduced downtime.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top