With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design, manufacturing, and integration of advanced powder conveying systems. This article provides an in-depth exploration of the principle and working scenario characteristics of calcium hydroxide powder conveying systems, highlighting the technical aspects and practical applications of such systems.
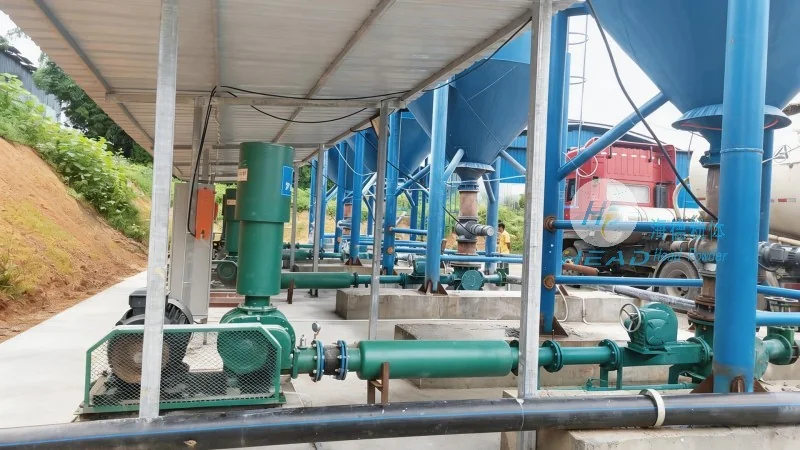
Calcium hydroxide, commonly known as slaked lime, is a widely used chemical in various industrial applications, including construction, water treatment, and agricultural sectors. The efficient and reliable transportation of calcium hydroxide powder is crucial for maintaining production efficiency and ensuring product quality. HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, has developed sophisticated powder conveying systems tailored to handle the unique properties of calcium hydroxide, such as its fine particle size, hygroscopic nature, and potential for dust generation.
The core principle of the calcium hydroxide powder conveying system is to utilize a combination of mechanical and pneumatic components to transport the powder from a storage silo or hopper to the processing equipment. The system typically consists of several key components, including a feeder, a conveying line (often using flexible hoses or rigid pipes), and a control system. The feeder, usually a rotary valve or a screw feeder, regulates the flow rate of the powder into the conveying line. The conveying line may employ positive displacement or pneumatic methods to move the powder. Positive displacement systems use a pump or a rotary lobe to push the powder through the line, while pneumatic systems use compressed air to create a flow of powder in a sealed tube. The control system monitors and adjusts the flow rate, pressure, and other parameters to ensure stable and efficient operation.
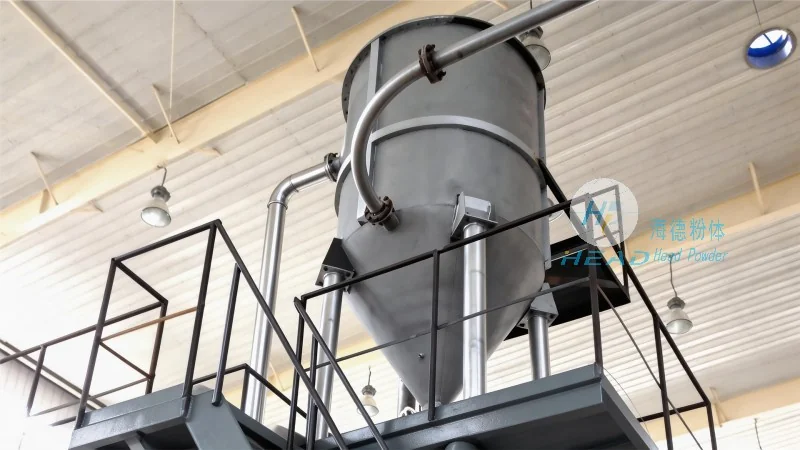
The working scenario characteristics of the calcium hydroxide powder conveying system are influenced by several factors, including the material properties of calcium hydroxide, the operational environment, and the specific application requirements. The fine particle size of calcium hydroxide makes it prone to caking and bridging in storage silos, which can affect the flow rate and uniformity of the powder. Therefore, the system is designed with features such as agitators or vibrators to prevent caking and ensure consistent material flow. The hygroscopic nature of calcium hydroxide means that it can absorb moisture from the air, leading to clumping and reduced flowability. The conveying system incorporates moisture-proof measures, such as sealed containers and dry air supply, to maintain the material's quality and prevent degradation. Additionally, the system is equipped with dust suppression mechanisms, such as cyclone separators and dust filters, to comply with environmental regulations and ensure operator safety. The working scenario also considers the need for flexibility in different production settings, allowing the system to adapt to varying production rates and material volumes.
HeadPowder's calcium hydroxide powder conveying systems offer several technical advantages that enhance performance and reliability. The use of high-quality materials and precision engineering ensures durability and long service life. The system's ability to handle high flow rates and maintain consistent material quality reduces downtime and improves overall production efficiency. The integration of advanced control technologies allows for real-time monitoring and adjustment of operational parameters, optimizing the conveying process. Furthermore, the system's design minimizes material loss and contamination, ensuring that the transported calcium hydroxide remains pure and suitable for its intended applications. The working scenario characteristics are tailored to meet the specific needs of different industries, providing customized solutions that enhance operational effectiveness.
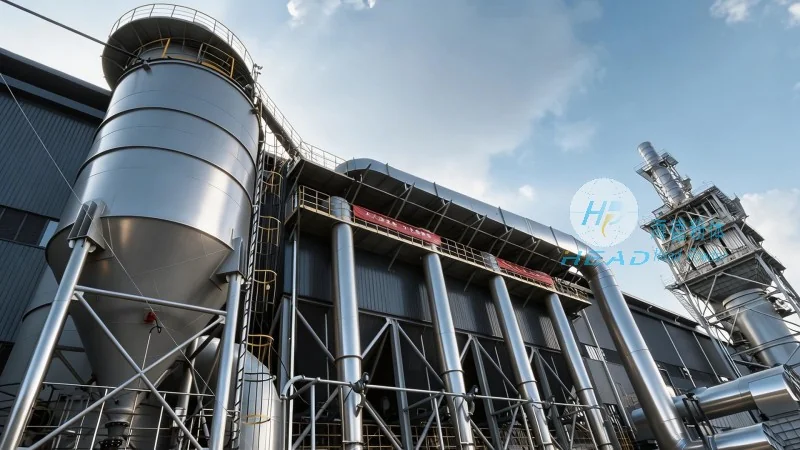
The calcium hydroxide powder conveying systems developed by HeadPowder Engineering Co., Ltd. have been successfully implemented in various industrial applications. In the construction industry, the system is used to transport calcium hydroxide for mortar and concrete production, ensuring uniform mixing and consistent product quality. In water treatment facilities, the system efficiently delivers calcium hydroxide for pH adjustment and coagulation processes, improving water treatment efficiency and compliance with environmental standards. In the agricultural sector, the system is utilized to distribute calcium hydroxide for soil amendment and pest control, enhancing crop yields and soil health. The working scenario characteristics of the system have contributed to increased productivity and reduced operational costs in these industries, demonstrating the effectiveness of HeadPowder's technology.
In conclusion, the calcium hydroxide powder conveying system developed by HeadPowder Engineering Co., Ltd. is a sophisticated and reliable solution for the efficient transportation of calcium hydroxide powder. By understanding the principle of operation and the working scenario characteristics, industries can leverage this technology to enhance production efficiency, maintain product quality, and comply with environmental regulations. HeadPowder's commitment to innovation and quality ensures that their powder conveying systems remain at the forefront of the industry, providing customized solutions that meet the evolving needs of various applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top