With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Wheat flour material handling systems are critical components in the food processing industry, particularly for facilities that handle large volumes of wheat flour. These systems are designed to efficiently transport, store, and manage wheat flour from raw material reception to final product packaging. Understanding the working principle and key features of such systems is essential for optimizing operational efficiency and maintaining product quality.
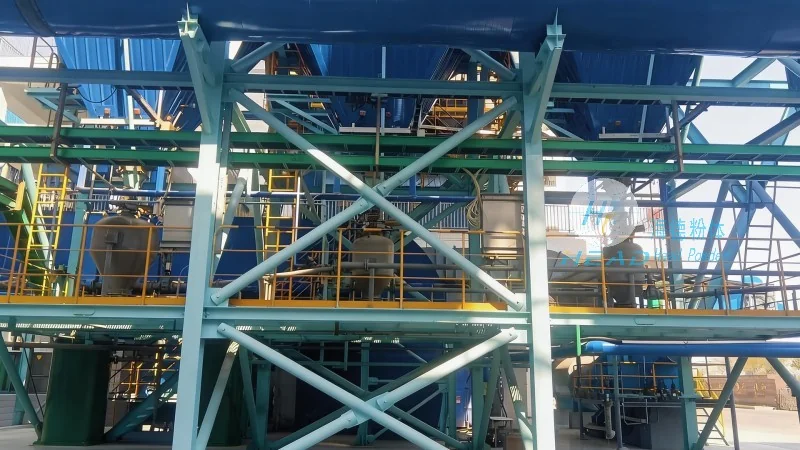
Wheat flour material handling systems are specialized equipment and processes used to move wheat flour through various stages of production. These systems typically include components like conveyors, hoppers, storage silos, and pneumatic systems. The primary goal is to ensure smooth and continuous flow of the product while minimizing dust, contamination, and energy consumption. In modern food processing plants, these systems are often integrated with automation and control technologies to enhance precision and reliability.
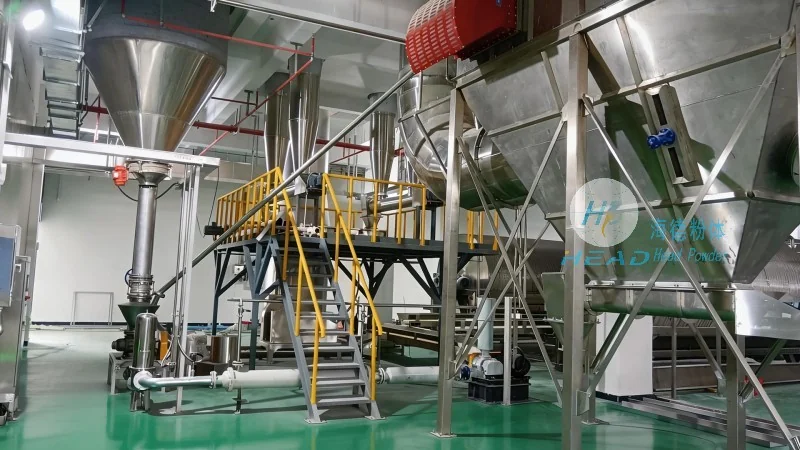
The working principle of a typical wheat flour material handling system involves several key steps. First, raw wheat is received and stored in bulk storage silos. From there, the flour is conveyed to a milling or processing area using pneumatic or mechanical conveyors. Pneumatic systems use air pressure to move flour through pipes, while mechanical systems employ belts, screws, or buckets to transport the material. The system also includes dust collection and filtration units to maintain a clean environment and prevent product loss. Additionally, the system may incorporate level sensors and control panels to monitor and regulate the flow of flour, ensuring that the process runs smoothly without interruptions.
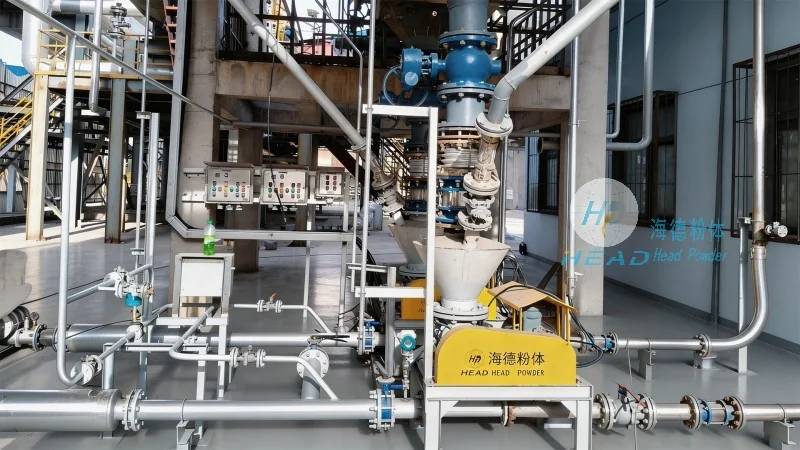
Wheat flour material handling systems are characterized by several important features that contribute to their effectiveness. One of the most notable features is the use of enclosed and sealed systems to prevent contamination from external sources. This is crucial in food processing, where product purity is paramount. Another key feature is the integration of energy-efficient technologies, such as variable frequency drives (VFDs) for conveyors, which adjust motor speed based on the load, reducing energy waste. The systems also often include advanced control systems that allow for remote monitoring and troubleshooting, improving operational flexibility. Additionally, the design of these systems prioritizes ease of maintenance, with accessible components and modular construction that simplifies repairs and upgrades. Safety features, such as emergency stop buttons and interlocked access panels, are also standard to protect operators and ensure compliance with safety regulations.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in the design and supply of wheat flour material handling systems. With a strong focus on innovation and customer satisfaction, HeadPowder has established itself as a trusted partner in the food processing industry. The company's expertise lies in creating customized solutions tailored to the specific needs of each client, whether it's a small-scale bakery or a large industrial mill. HeadPowder's systems are engineered to meet international standards for hygiene, safety, and efficiency, ensuring that they deliver optimal performance in real-world applications. The company's commitment to quality is reflected in its use of high-grade materials and rigorous testing procedures, which guarantee the durability and reliability of its products. Furthermore, HeadPowder provides comprehensive after-sales support, including installation, training, and maintenance services, to ensure that clients can maximize the value of their investment.
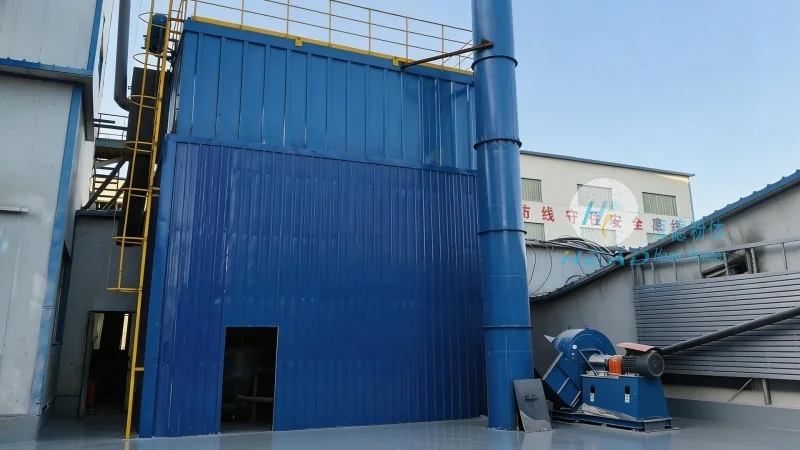
In conclusion, wheat flour material handling systems play a vital role in the food processing industry by ensuring the efficient and safe transport of wheat flour. The working principle of these systems, which combines mechanical and pneumatic technologies with advanced control systems, enables seamless operation and minimal product loss. Key features such as enclosed design, energy efficiency, and safety measures further enhance their effectiveness. For businesses looking to optimize their wheat flour handling processes, partnering with a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd. is essential. By investing in high-quality material handling systems, companies can improve operational efficiency, maintain product quality, and ultimately enhance their competitiveness in the market. The expertise and dedication of HeadPowder in this field make them a reliable choice for any organization seeking to upgrade or expand its wheat flour handling capabilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top