With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, specializes in the design, manufacturing, and application of advanced pneumatic conveying systems. Based in Shandong, China, the company leverages decades of industry experience to deliver efficient and reliable solutions for transporting bulk powders. This article provides an in-depth look at the operation process and working principles of positive pressure dilute phase powder pneumatic conveying, a technology widely used in various industrial sectors for its ability to handle fine and dry powders with minimal product degradation.
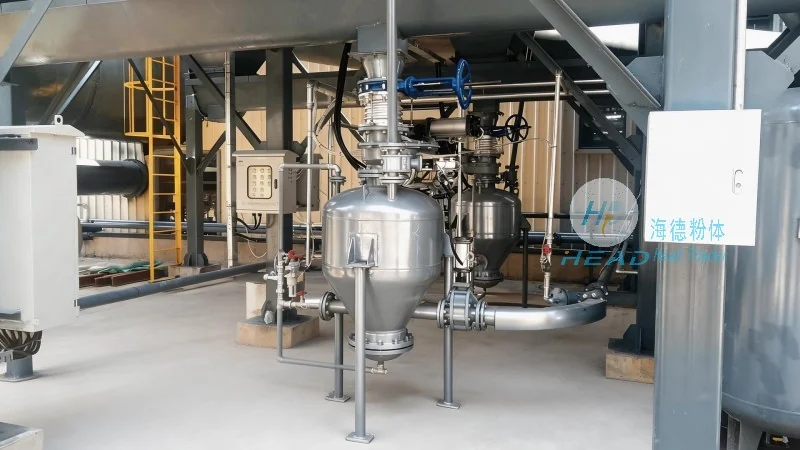
The core components of a positive pressure dilute phase system include a high-pressure blower or fan, a material feed hopper, a conveying pipeline network, a dust separator (often a cyclone or bag filter), and a product collection bin. The blower generates the necessary airflow and pressure to transport the powder particles through the pipeline. The feed hopper ensures a consistent supply of material, while the pipeline transports the suspended particles. The dust separator then separates the powder from the air stream, allowing the product to be collected and the air to be discharged or recirculated.
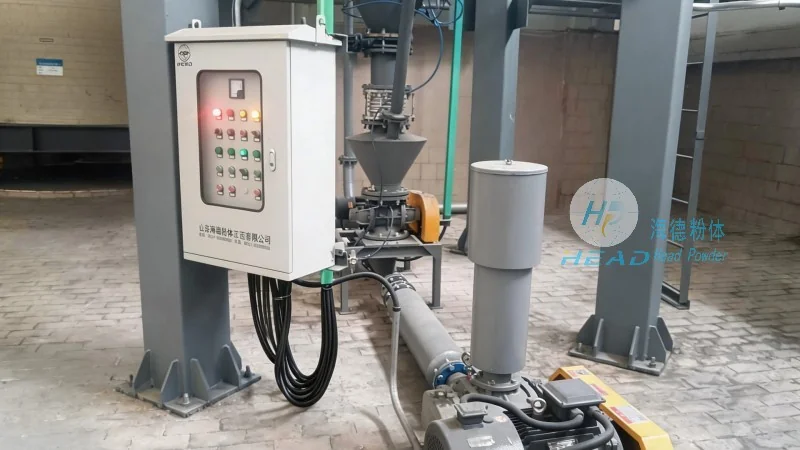
In a positive pressure system, the air is pressurized and forced through the pipeline, carrying the powder particles in a dilute suspension. The particles are kept in suspension by the high velocity of the air, which overcomes the gravitational forces acting on the particles. The key principle is that the air velocity is maintained above the minimum fluidization velocity of the powder, ensuring that the particles do not settle out of the air stream. This method is particularly effective for fine powders with low bulk density, as it minimizes the risk of clogging and ensures a uniform flow.
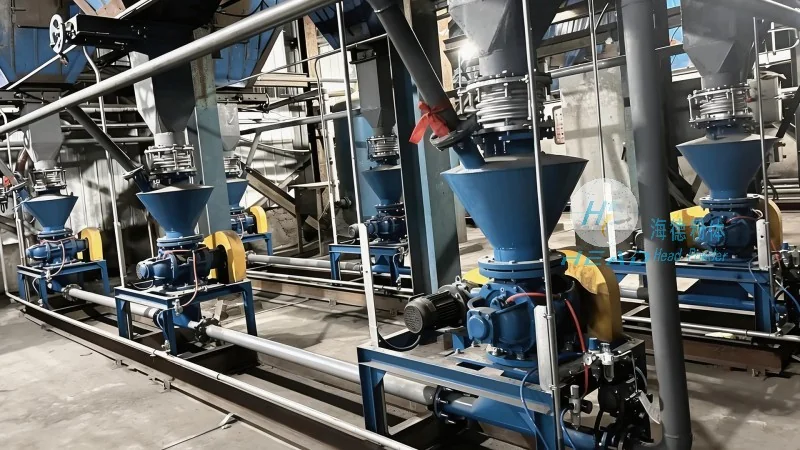
The operation process of a positive pressure dilute phase system begins with the loading of the material into the feed hopper. A feeder, such as a rotary valve or a screw feeder, controls the flow rate of the powder into the pipeline. The blower then starts, and the pressurized air is introduced into the pipeline, creating a positive pressure environment. As the air flows through the pipeline, it picks up the powder from the hopper and transports it to the destination point. At the receiving end, a dust separator is used to separate the powder from the air. The separated powder is collected in a bin, while the air is either filtered and discharged or recirculated back to the blower for energy efficiency. The system is typically equipped with control valves and sensors to monitor pressure, flow rate, and material level, ensuring stable and safe operation.
Positive pressure dilute phase conveying offers several advantages over other powder handling methods. It is capable of transporting powders over long distances with minimal product degradation, as the particles are kept in a suspended state, reducing friction and impact. The system is also relatively simple in design, with fewer moving parts compared to other conveying methods, leading to lower maintenance costs. Additionally, it can handle a wide range of powder types, including fine, cohesive, and abrasive materials, making it versatile for various industrial applications. The positive pressure design also provides better safety by preventing dust explosions, as the system operates under pressurized conditions, reducing the risk of ignition sources.
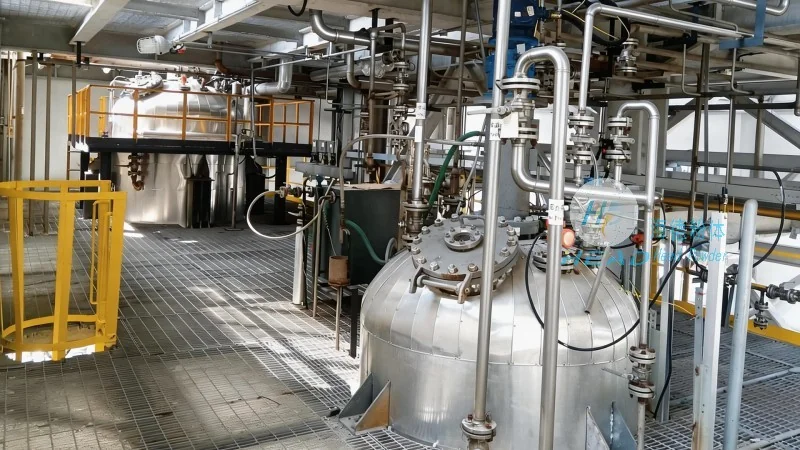
Shandong HeadPowder Engineering Co., Ltd. has successfully applied positive pressure dilute phase pneumatic conveying systems in numerous industries. In the pharmaceutical sector, the technology is used to transport active pharmaceutical ingredients (APIs) and excipients with high precision and minimal contamination. In the food industry, it handles dry powders like flour, sugar, and spices, ensuring product integrity and hygiene. The chemical industry utilizes these systems for transporting raw materials and intermediates, while the cement and construction industries use them for transporting bulk cement and other powders. The versatility of the system makes it suitable for a wide range of applications where efficient and reliable powder handling is critical.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top