With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Understanding the working principle and features of a vacuum suction type powder conveying system is crucial for industries dealing with bulk powder materials. This system utilizes a vacuum pump to create a negative pressure environment, enabling the efficient and safe transportation of powders over long distances.
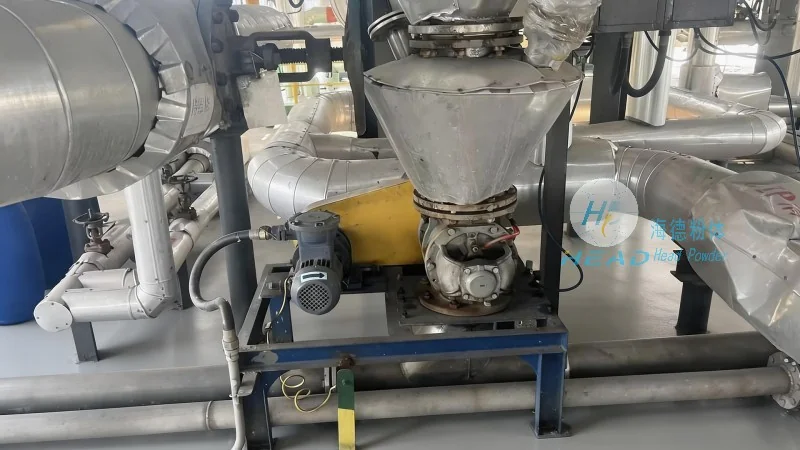
The operation of a vacuum suction type powder conveying system begins with the activation of the vacuum pump. Once the pump starts, it draws air from the conveying line, creating a negative pressure inside the pipeline. This pressure differential causes the powder material to be drawn into the system through the inlet hopper or suction port. The powder is then carried along the pipeline by the airflow generated by the vacuum pump. The system typically includes components such as a vacuum pump, filter, and control valves to regulate the flow and ensure proper operation. The entire process is designed to move powders from the source to the destination without the need for positive pressure, which reduces energy consumption and operational complexity.
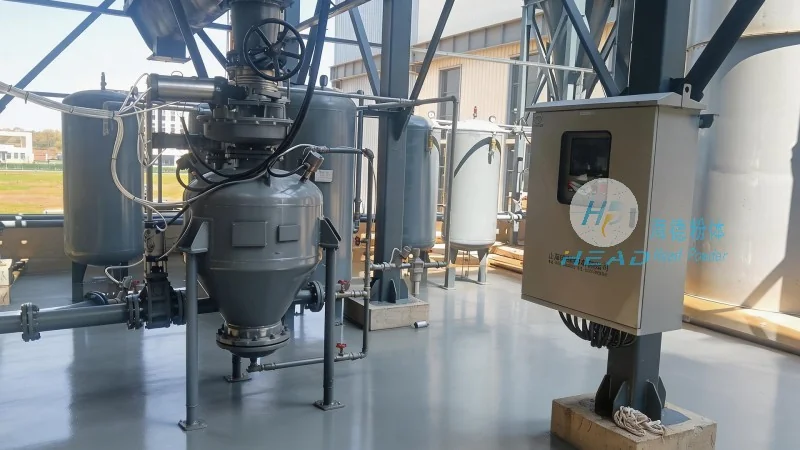
One of the primary advantages of this system is its ability to handle fine and abrasive powders without causing dust contamination or product degradation. The negative pressure environment minimizes the risk of dust emissions, making it suitable for applications where air quality and safety are critical. Additionally, the system offers flexibility in pipeline layout, allowing for horizontal, vertical, or complex path configurations to accommodate various plant layouts. Another notable feature is its energy efficiency, as the vacuum pump operates at lower pressures compared to positive pressure systems, resulting in reduced energy costs. The system also provides consistent flow rates, ensuring reliable material transfer even with varying powder properties. Furthermore, maintenance requirements are relatively low due to the simple design and fewer moving parts compared to other conveying methods.
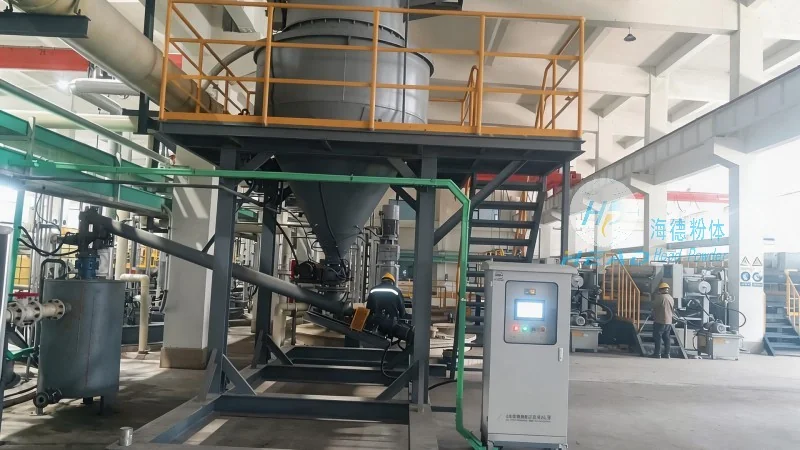
Vacuum suction type powder conveying systems are widely used in various industries, including pharmaceuticals, food processing, chemical manufacturing, and cement production. In the pharmaceutical industry, the system ensures that powders are transferred in a sterile and dust-free environment, meeting stringent regulatory requirements. In food processing, it maintains product purity and safety by preventing cross-contamination. Chemical manufacturers benefit from the system's ability to handle abrasive and corrosive powders without damaging the equipment. Cement and construction industries use it for transporting raw materials and finished products efficiently. The versatility of the system makes it a preferred choice for applications requiring long-distance, low-pressure, and safe powder transfer.
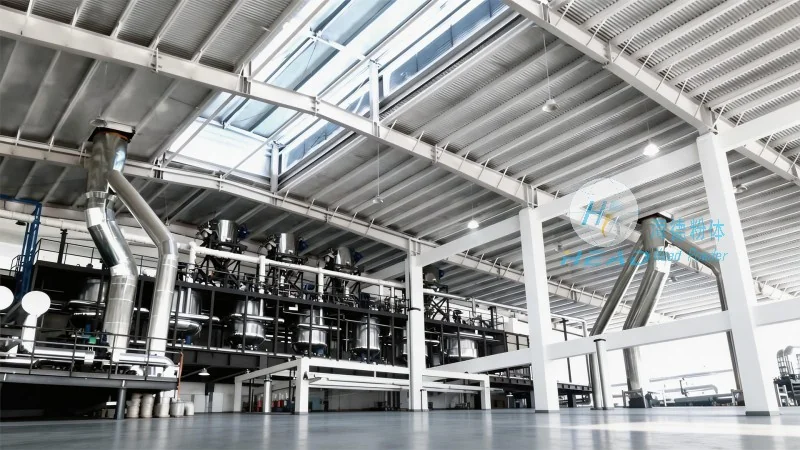
HeadPowder, a division of Shandong HeadPowder Engineering Co., Ltd., is a renowned manufacturer specializing in the design, development, and supply of advanced powder conveying systems. With a strong presence in China, particularly in Shandong, the company has built a reputation for delivering high-quality, reliable, and energy-efficient solutions tailored to the specific needs of various industries. HeadPowder's expertise lies in customizing vacuum suction type systems to meet the unique requirements of clients, ensuring optimal performance and compliance with industry standards. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking efficient and sustainable powder handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top