With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider of powder handling solutions, specializes in advanced technologies for efficient material transport. Based in Shandong, China, the company has established itself as a trusted partner in the industry, offering innovative systems that meet the demanding needs of various sectors. This article explores the working principle and key features of the negative pressure suction type powder conveying system, a technology that has revolutionized the way powders are transported in industrial applications.
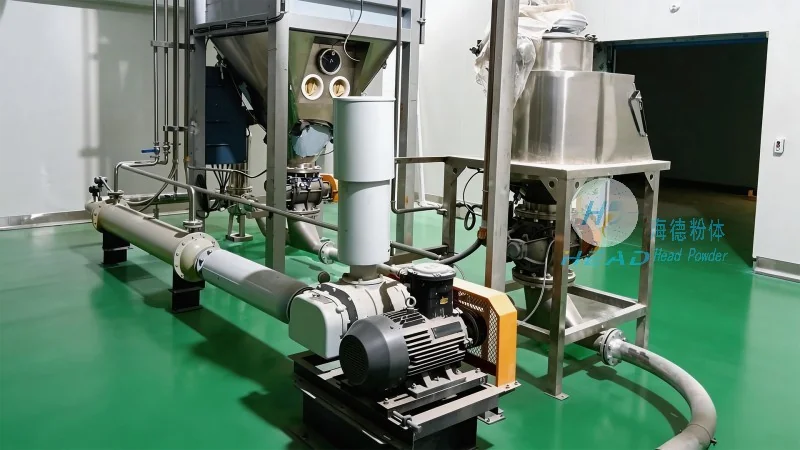
The negative pressure suction type powder conveying system operates on the principle of creating a low-pressure environment at the material intake point. This is achieved by using a vacuum pump or a fan that draws air and the powder mixture into the conveying line. The system typically consists of several components, including a hopper for material storage, a vacuum pump to generate the suction force, a conveying pipe network, and a dust collector or filter to separate the powder from the air at the discharge end. As the vacuum pump runs, it creates a pressure differential between the intake and discharge points. The material is drawn from the hopper into the conveying line due to the negative pressure, and the air-powder mixture is then transported through the pipes to the collection point. The dust collector then separates the powder from the air, allowing the clean air to be released back into the environment or recirculated if necessary. This process ensures that the powder is transported efficiently and with minimal loss, while maintaining a clean and safe working environment.
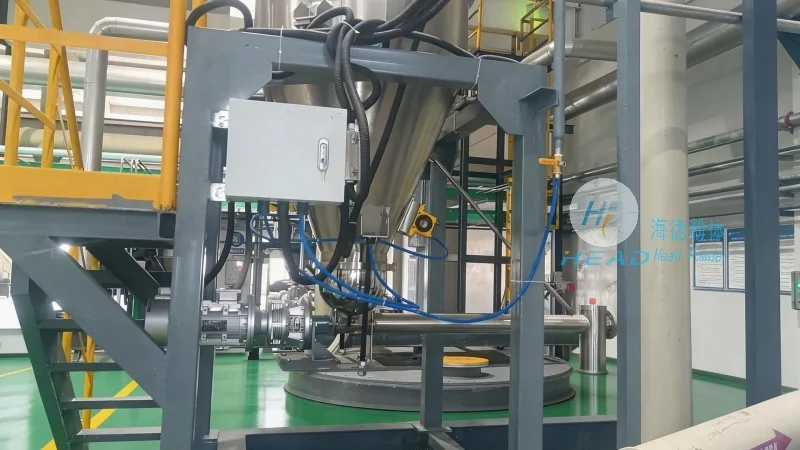
One of the primary advantages of the negative pressure suction type powder conveying system is its ability to handle fine and abrasive powders without causing excessive wear or damage to the equipment. The system is designed to minimize particle breakage and maintain the integrity of the material being transported. This is particularly important for sensitive powders that require careful handling to preserve their properties. Additionally, the system offers excellent dust control, which is crucial for maintaining a safe and healthy workplace. The negative pressure environment helps to prevent dust from escaping into the air, reducing the risk of respiratory issues and other health hazards. Another key feature is the flexibility of the system, which allows for the conveyance of powders over long distances and through complex pipe networks. The modular design of the system enables easy installation and integration into existing production lines, making it a versatile solution for various industrial applications.
The negative pressure suction type powder conveying system is widely used in a variety of industries, including pharmaceuticals, food processing, chemicals, and mining. In the pharmaceutical industry, for example, the system is used to transport active pharmaceutical ingredients (APIs) and other sensitive powders with high precision and minimal contamination. The food processing industry benefits from the system's ability to handle food-grade powders while maintaining strict hygiene standards. In the chemical industry, the system is used to transport abrasive and corrosive powders, protecting the equipment from wear and ensuring the safety of the operators. The mining industry utilizes the system for transporting bulk materials such as coal and ore, improving efficiency and reducing labor costs. The benefits of this technology extend beyond just material transport; it also contributes to improved productivity, reduced downtime, and lower maintenance costs. By minimizing material loss and preventing equipment damage, the system helps companies to achieve higher yields and better overall performance.
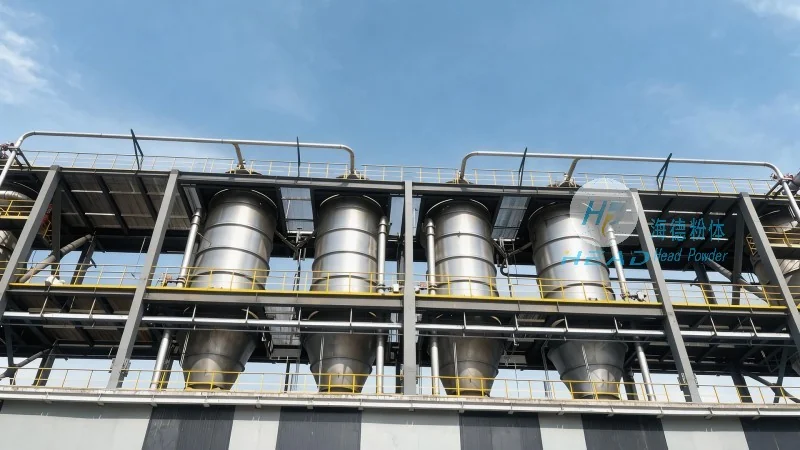
HeadPowder's negative pressure suction type powder conveying system represents a significant advancement in powder handling technology. By combining efficient suction mechanisms with robust design, the system offers a reliable and effective solution for transporting a wide range of powders. The company's expertise in engineering and manufacturing ensures that each system is tailored to meet the specific needs of its clients, providing customized solutions that enhance operational efficiency and safety. As industries continue to demand more efficient and sustainable material transport solutions, the negative pressure suction type powder conveying system remains a top choice for businesses looking to optimize their processes and improve their bottom line.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top