With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Desulfurization sodium bicarbonate, commonly used in flue gas desulfurization processes, is often transported via pneumatic conveying systems. The working principle of this method involves the use of a gas stream, typically air or a mixture of air and other gases, to transport solid particles of sodium bicarbonate through a pipeline. This process relies on the interaction between the gas and the solid particles, creating a two-phase flow system. In a typical setup, a blower or compressor generates the necessary pressure to move the particles. The sodium bicarbonate is fed into the conveying line, where it is entrained by the moving gas. The gas flow carries the particles along the pipeline, often with the assistance of special devices like cyclones or separators at the receiving end to separate the solid material from the gas stream. The entire system operates by maintaining a consistent gas velocity to ensure that the particles remain suspended and transported efficiently without clogging the pipeline.

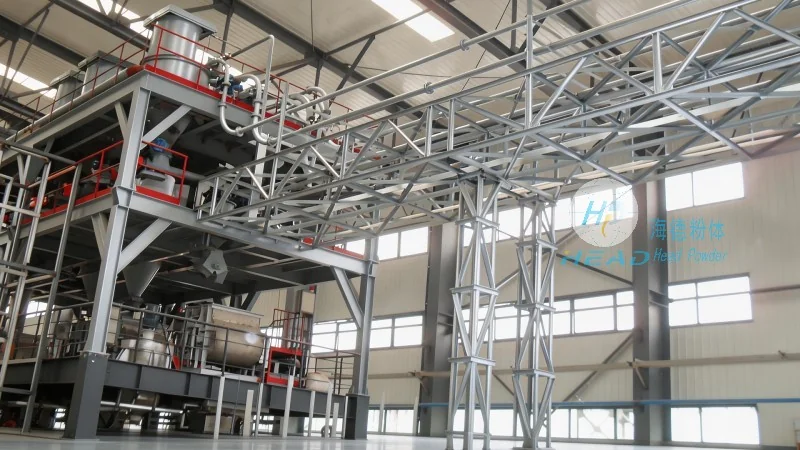
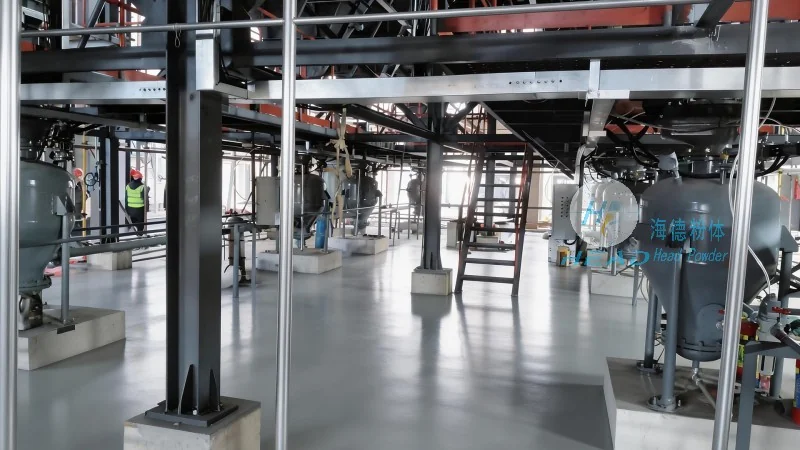
The pneumatic conveying of desulfurization sodium bicarbonate exhibits several notable characteristics that make it an effective method for material handling in industrial applications. First, it offers a high degree of flexibility in terms of system layout, as the conveying lines can be arranged in various configurations to suit the plant layout. This adaptability is crucial for integrating the system with existing infrastructure in power plants or industrial facilities. Second, the process is relatively clean and dust-free compared to traditional methods like bucket elevators or belt conveyors, which helps in maintaining a better working environment and reduces the risk of dust-related health issues. Third, the system can achieve high transport capacities, allowing for the efficient movement of large volumes of sodium bicarbonate, which is essential for continuous operation in desulfurization plants. Additionally, the pneumatic conveying system can be designed to operate under different pressure conditions, such as pressure or vacuum systems, depending on the specific requirements of the plant. The vacuum system, for instance, is often used for short-distance or low-volume transport, while pressure systems are suitable for longer distances and higher capacities. Another important characteristic is the ability to handle abrasive materials like sodium bicarbonate without significant wear on the conveying components, as the gas flow helps to reduce particle impact on the pipeline walls. This reduces maintenance costs and extends the service life of the equipment. Furthermore, the system can be integrated with other process equipment, such as storage silos or reactors, to form a complete material handling solution. The characteristics of this method also include its ability to transport the material in a controlled manner, ensuring that the particles are not exposed to excessive temperatures or moisture, which could affect their performance in the desulfurization process. Overall, the pneumatic conveying of desulfurization sodium bicarbonate combines efficiency, flexibility, and environmental benefits, making it a preferred choice for many industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top