

What is a White Sugar Powder Pneumatic Conveying System? And What Are Its Design Principles?
White sugar, a fundamental ingredient in the food and beverage industry, demands efficient and reliable handling systems to maintain smooth production workflows. Among the various methods for transporting bulk powders like white sugar, pneumatic conveying systems have become a preferred choice due to their ability to handle fine powders with minimal dust and contamination. This article delves into the concept of a white sugar powder pneumatic conveying system, detailing its design principles and the key factors that make it an effective solution for sugar processing facilities.
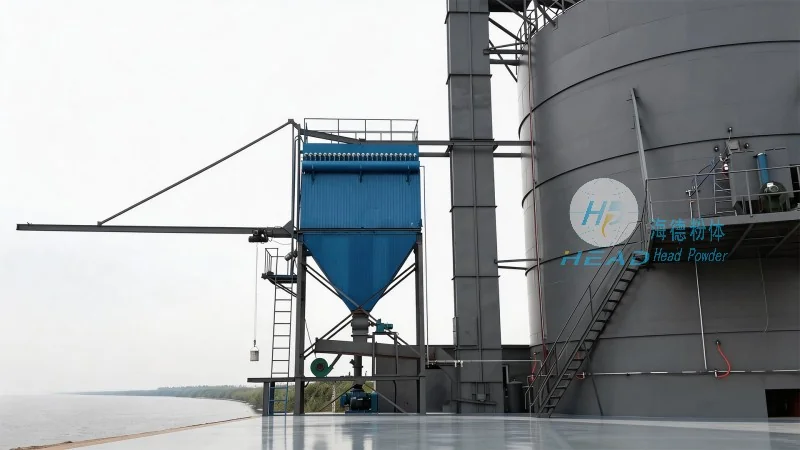
Pneumatic Conveying Systems: An Overview
Pneumatic conveying systems utilize air or gas to transport solid materials, such as white sugar, through a pipeline. This method offers several advantages over traditional mechanical conveying, including reduced risk of product contamination, lower maintenance requirements, and the capacity to handle materials with high moisture content or sensitive properties. The core components of a pneumatic conveying system typically include a material feed hopper, a conveyor line, a control system, and a dust collection or filtration unit. The system operates by creating a pressure differential between the inlet and outlet of the conveyor line, which propels the white sugar particles through the pipeline using compressed air.
Design Principles for White Sugar Powder Pneumatic Conveying
The design of a white sugar powder pneumatic conveying system involves several critical principles to ensure optimal performance and efficiency. First, the system must be customized to the specific characteristics of white sugar, including its particle size, density, and flowability. These properties influence the selection of the conveying velocity, which is typically determined by the material's terminal velocity and the required conveying distance. For white sugar, a conveying velocity of 10-20 meters per second is common, as it balances the need for efficient transport with energy efficiency. Second, the system must incorporate proper material handling equipment to prevent blockages and ensure consistent flow. This includes using a hopper with a suitable discharge mechanism, such as a rotary valve or a star feeder, to control the flow rate of the white sugar into the conveyor line. Additionally, the pipeline design is crucial, as it must be sized appropriately to accommodate the particle size distribution of the white sugar and minimize pressure drop. The use of smooth, corrosion-resistant materials, such as stainless steel or PTFE-coated pipes, is essential to prevent product buildup and maintain hygiene standards.
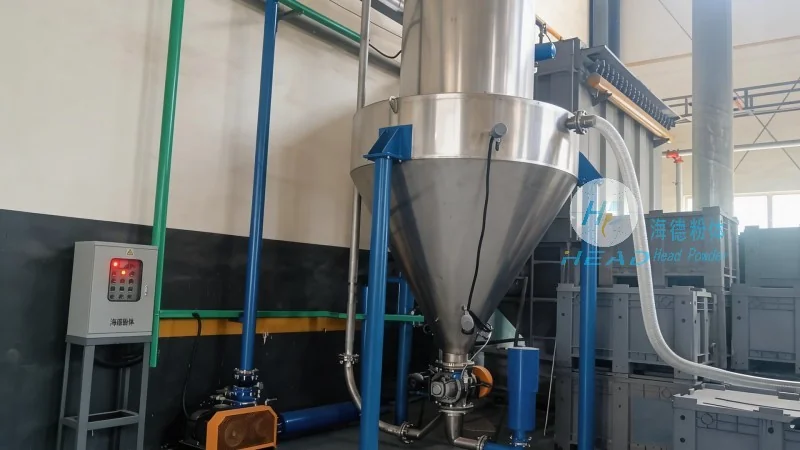
Key Components and Their Functionality
Several key components make up a white sugar powder pneumatic conveying system, each playing a vital role in the overall operation. The material feed hopper is the starting point of the system, where white sugar is stored and fed into the conveyor line. It is typically equipped with a level indicator and a discharge valve to regulate the flow of material. The conveyor line itself is the main pathway for transporting the white sugar, and its design must account for the material's properties to ensure smooth flow. The control system, which may include sensors and a programmable logic controller (PLC), monitors the system's performance and adjusts parameters as needed to maintain optimal operation. The dust collection or filtration unit is another critical component, as it captures any airborne particles and prevents them from escaping into the environment. This unit typically uses a baghouse or cyclone separator to filter the air and return clean air to the system or release it to the atmosphere.
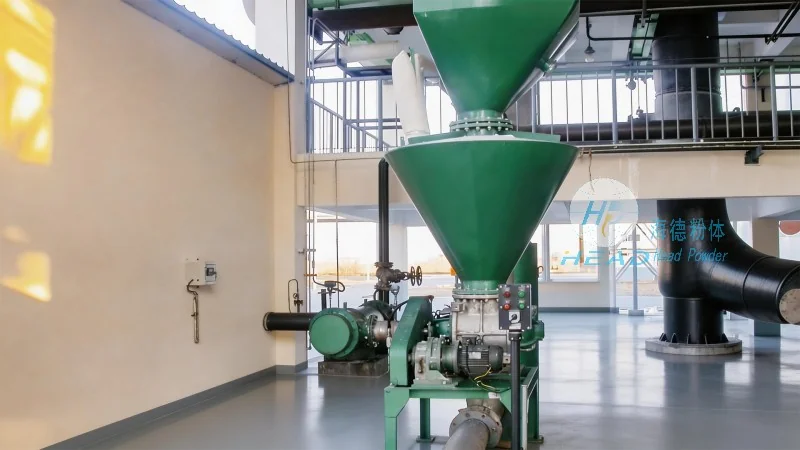
Benefits of Using a Pneumatic Conveying System for White Sugar
Implementing a pneumatic conveying system for white sugar processing offers numerous benefits that enhance operational efficiency and product quality. One of the primary advantages is the reduction in product contamination, as the system operates in a closed environment, minimizing exposure to external contaminants. This is particularly important for white sugar, which is used in food applications where purity is paramount. Additionally, pneumatic conveying systems reduce labor costs by automating the material handling process, as they eliminate the need for manual loading and unloading of sugar. The system also improves safety in the workplace by eliminating the need for workers to handle large quantities of bulk material, reducing the risk of accidents and injuries. Furthermore, the energy efficiency of pneumatic conveying systems is higher compared to mechanical systems, as they use compressed air to transport the material, which can be more cost-effective in the long run.
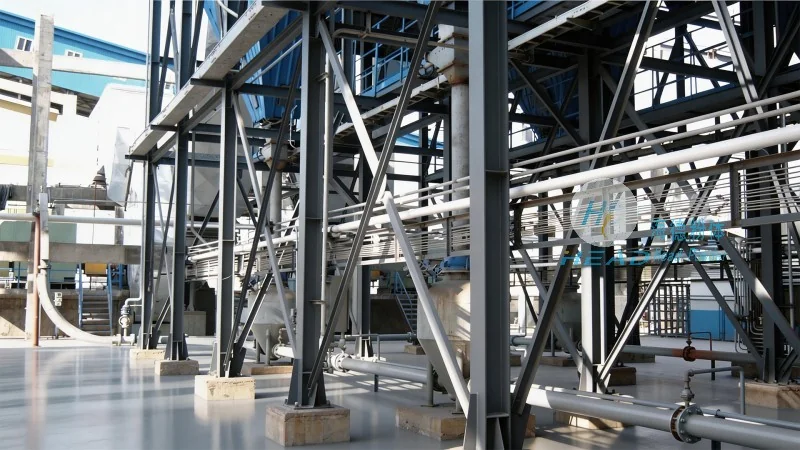
Application in Sugar Processing Facilities
White sugar powder pneumatic conveying systems are widely used in sugar processing facilities, from raw sugar storage and handling to final product packaging. In these facilities, the system is often integrated with other processing equipment, such as crushers, classifiers, and packaging machines, to form a seamless production line. The system's ability to handle fine powders with high accuracy and low loss makes it ideal for applications where precision is critical, such as in the production of refined white sugar. Additionally, the system's flexibility allows it to be adapted to different production scales, from small-scale operations to large industrial facilities. This adaptability makes it a versatile solution for sugar processing plants, as they can scale their operations without significant changes to the conveying system.
Conclusion
A white sugar powder pneumatic conveying system is a sophisticated and efficient solution for transporting bulk white sugar in processing facilities. By leveraging the principles of pneumatic conveying, this system offers numerous benefits, including reduced contamination, improved safety, and enhanced operational efficiency. The design of the system must be tailored to the specific characteristics of white sugar, ensuring optimal performance and reliability. As a leading provider of engineering solutions for bulk material handling, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying systems that meet the unique needs of sugar processing facilities. With a focus on quality and innovation, HeadPowder provides comprehensive solutions that enhance the productivity and profitability of sugar processing operations.