

What is a Corn Cob Pneumatic Conveying System? And What Are Its Design Principles?
For industries dealing with corn cob material handling, the choice of a reliable and efficient conveying system is crucial. A corn cob pneumatic conveying system is a specialized solution designed to transport corn cobs and related byproducts through a network of pipes using air pressure. This system offers advantages such as reduced labor costs, minimized material damage, and enhanced safety compared to traditional methods like manual handling or mechanical conveyors.
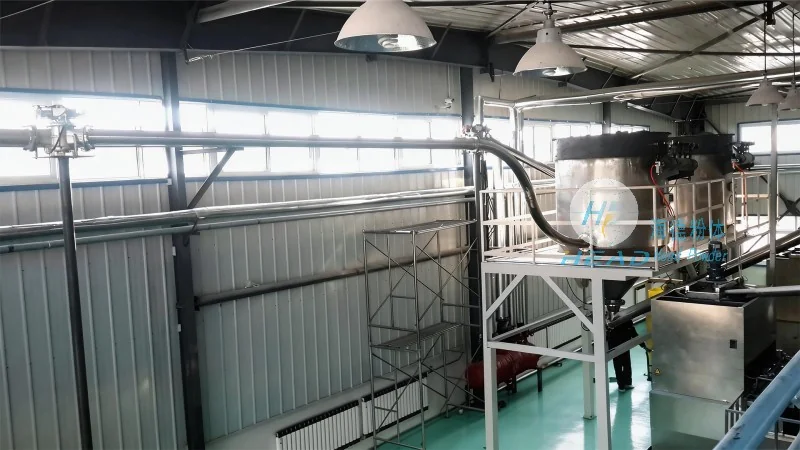
Design Principles of Corn Cob Pneumatic Conveying Systems
The core design principle of a corn cob pneumatic conveying system revolves around the use of air as the primary transport medium. The system typically consists of a hopper for material storage, a blower or compressor to generate air pressure, and a series of pipes to guide the material from the source to the destination. The design must consider factors like material characteristics (density, moisture content, abrasiveness), system capacity requirements, and the distance over which material needs to be conveyed. Engineers at Shandong HeadPowder Engineering Co., Ltd. specialize in tailoring these systems to meet specific operational needs, ensuring optimal performance and efficiency.
Key Components of the System
Several critical components make up a corn cob pneumatic conveying system. The first is the material hopper, which holds the corn cobs and allows for controlled feeding into the system. Next is the air supply unit, which can be a positive displacement blower or a centrifugal fan, depending on the system's requirements. The piping network connects the hopper to the discharge point and includes features like bends, elbows, and expansion joints to accommodate changes in direction and pressure. Additionally, the system may include filters and cyclones to separate the conveyed material from the air, ensuring clean air discharge and preventing material buildup in the pipes. The design of each component is crucial for the overall effectiveness of the system.
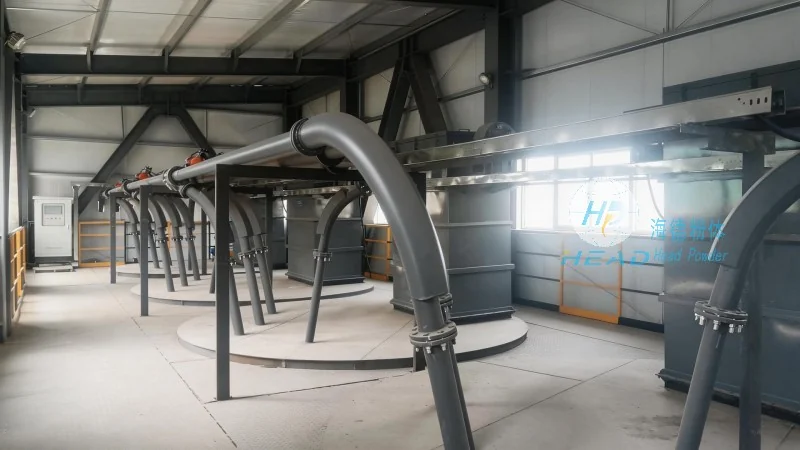
Applications in Corn Processing Industries
Corn cob pneumatic conveying systems are widely used in various stages of corn processing. In feed mills, they efficiently transport corn cobs from storage silos to processing equipment. In biofuel production facilities, the system moves corn cobs to boilers or reactors for energy generation. The system's ability to handle large volumes of material with minimal maintenance makes it ideal for continuous production lines. Shandong HeadPowder Engineering Co., Ltd. has implemented such systems in numerous corn processing plants across China, demonstrating their reliability and cost-effectiveness.
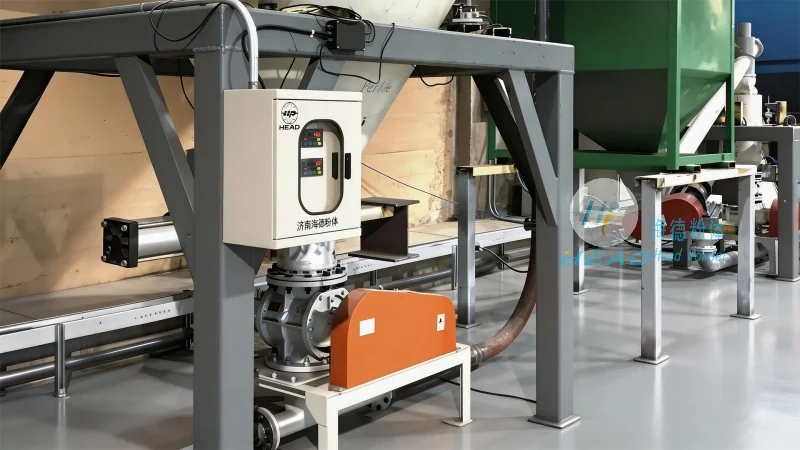
Advantages of Using a Pneumatic Conveying System for Corn Cob Transport
Compared to traditional conveying methods, a corn cob pneumatic conveying system offers several advantages. One of the most significant is the reduction in material handling time and labor costs. The system can transport large quantities of corn cobs over long distances without the need for manual labor or mechanical equipment. Additionally, the enclosed system minimizes dust and debris, improving workplace safety and reducing environmental impact. The design also allows for easy integration with other processing equipment, streamlining the overall production process. Furthermore, the system's flexibility allows for adjustments in conveying speed and direction, adapting to changing production demands.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading manufacturer and supplier of industrial conveying systems. With years of experience in the industry, the company specializes in designing and manufacturing corn cob pneumatic conveying systems tailored to the specific needs of corn processing facilities. Their team of engineers and technicians work closely with clients to understand their operational requirements and provide customized solutions that enhance efficiency and productivity. The company's commitment to quality and customer satisfaction has made it a trusted partner for many corn processing companies in China and beyond.