With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Coal ash particle pneumatic conveying is a specialized method of material handling that involves transporting coal ash particles through a pipeline using air or gas as the conveying medium. This technology is crucial in industrial settings where efficient and safe movement of bulk materials like coal ash is required. The process typically uses a blower or compressor to generate the necessary air pressure, which propels the particles through the system. Understanding the principles and applications of this technology is essential for optimizing material handling operations in various industries.
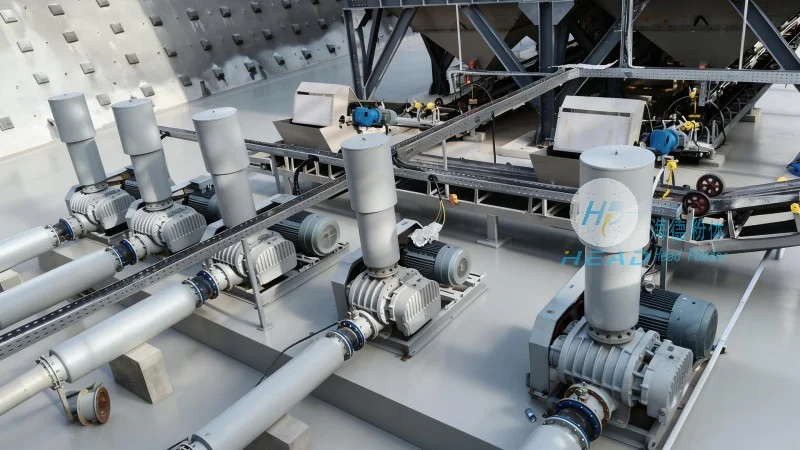
Pneumatic conveying systems are widely used in industries such as power generation, construction, and waste management due to their ability to transport dry bulk materials over long distances without the need for mechanical components like belts or buckets. These systems are particularly effective for handling materials that are dusty, abrasive, or have a tendency to clump together. The core components of a pneumatic conveying system include a material feed hopper, a conveying line, a separation or collection unit, and a dust collection system. The choice of system design—whether it's a positive pressure, negative pressure, or a combination of both—depends on factors like the material characteristics, distance to be conveyed, and the required throughput.
Coal ash, the residue left after coal is burned in power plants, presents unique challenges for pneumatic conveying. It is typically a fine, powdery material with a high moisture content and abrasive properties. These characteristics can lead to issues such as caking, blockages, and increased wear on system components. To address these challenges, specialized equipment and system designs are employed. For instance, using a positive pressure system with a high-pressure blower can help maintain consistent air flow and prevent particle accumulation. Additionally, incorporating features like cyclone separators and filter bags can improve the efficiency of particle separation and reduce dust emissions.
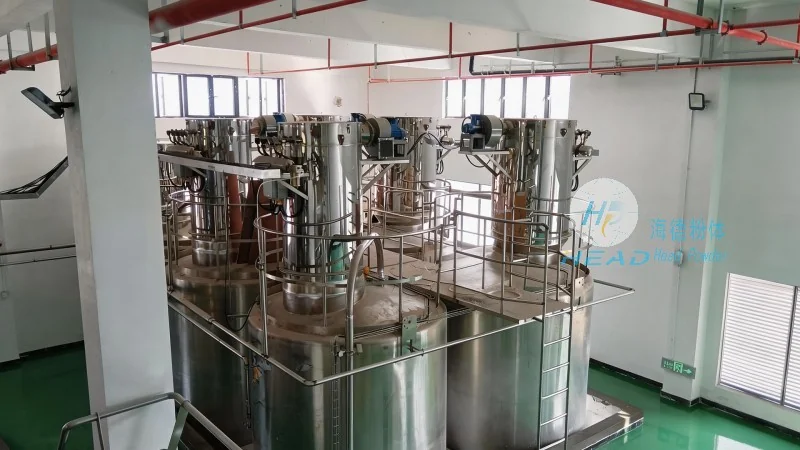
Pneumatic conveying systems are generally classified into two main categories: positive pressure and negative pressure systems. Positive pressure systems use a blower to force air and material through the pipeline, making them suitable for conveying materials over longer distances and at higher capacities. Negative pressure systems, on the other hand, use a vacuum to draw material into the system, which is often used for shorter distances or when the material needs to be collected from multiple sources. Within these categories, there are further subtypes such as dilute phase and dense phase systems. Dilute phase systems operate at higher velocities, with particles suspended in the air stream, while dense phase systems operate at lower velocities, with particles moving in a more concentrated stream. The selection of the appropriate system type depends on the specific requirements of the application, including the material's properties, the distance to be conveyed, and the desired system efficiency.
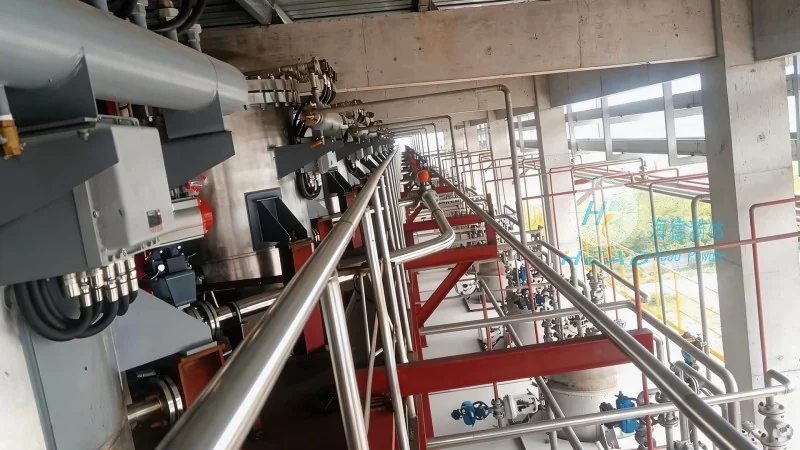
The applications of pneumatic conveying in coal ash handling are diverse and critical to the efficient operation of power plants and related facilities. One common application is the transport of coal ash from the boiler to storage silos or disposal sites. This process requires a reliable system that can handle the volume and characteristics of the ash while minimizing downtime and maintenance. Another application is the transfer of ash from storage silos to processing equipment, such as ash utilization plants or landfill sites. Pneumatic conveying systems are also used in the recycling of coal ash, where the ash is processed into valuable byproducts like cement additives or construction materials. In each of these applications, the efficiency and reliability of the pneumatic conveying system directly impact the overall productivity and cost-effectiveness of the operation.
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for material handling, specializes in the design, installation, and maintenance of pneumatic conveying systems tailored to the needs of coal ash and other bulk materials. With a deep understanding of the challenges associated with coal ash particle conveying, HeadPowder offers customized solutions that address the unique characteristics of each application. The company's team of experienced engineers and technicians work closely with clients to assess their specific requirements and develop systems that meet or exceed industry standards. HeadPowder's commitment to quality and innovation has made it a trusted partner for many power plants and industrial facilities in China and beyond. The company's headquarters is located in Shandong, China, where it continues to advance its technology and provide top-tier services to its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top