With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries dealing with corn cob processing, efficient and reliable powder conveying systems are crucial for maintaining production efficiency and product quality. The corn cob powder conveying system, as a key component in the processing chain, ensures the smooth transfer of corn cob powder from one processing stage to another. This article provides an overview of the corn cob powder conveying system, focusing on its structural design and operational principles, while highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in delivering advanced solutions for powder handling needs.
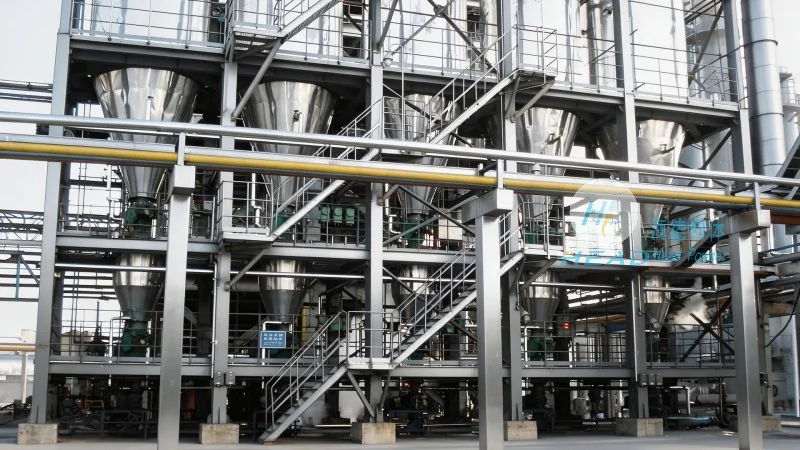
Corn cob powder, a fine particulate byproduct of corn processing, presents unique handling challenges due to its physical properties. These properties include a wide particle size distribution, varying bulk density, and potential moisture content, which can affect flow characteristics and system performance. Efficient conveying of corn cob powder requires equipment designed to accommodate these variations, preventing issues such as material bridging, segregation, or degradation. The corn cob powder conveying system must be engineered to maintain consistent flow rates and minimize downtime, ensuring that the material is transferred smoothly from storage to processing or packaging stages. The challenges posed by corn cob powder highlight the importance of specialized conveying solutions that address the material's specific needs.
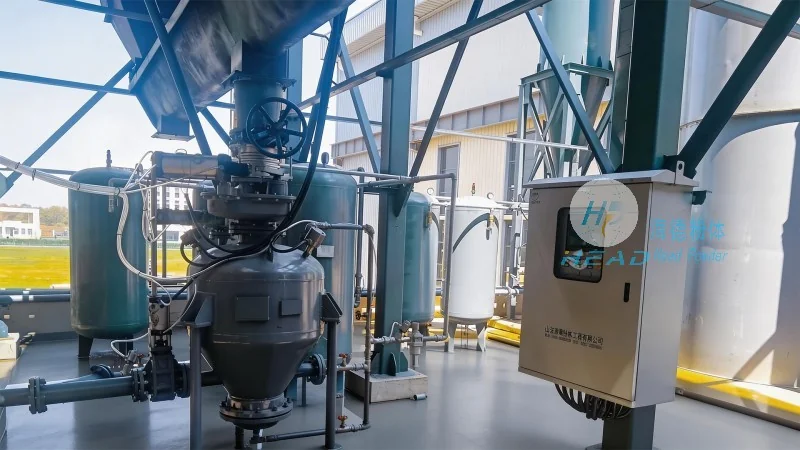
The structural design of a corn cob powder conveying system integrates several key components to achieve reliable material transfer. The system typically starts with a hopper, which stores the corn cob powder and feeds it into the conveyor. The hopper is constructed with appropriate dimensions and material to prevent material bridging and ensure uniform feeding. Next, the conveyor itself, which can be pneumatic or mechanical, transports the material. Pneumatic systems use air pressure to suspend and move the powder through pipelines, while mechanical systems, such as screw or belt conveyors, rely on mechanical force. The choice of conveyor type depends on factors like the conveying distance, material properties, and required flow rate. For corn cob powder, which can be abrasive and have varying particle sizes, a robust design with durable materials is essential to minimize wear and extend the system's lifespan. Additional components, such as control valves, filters, and dust collection systems, are integrated to regulate flow, maintain air quality, and ensure safe operation.
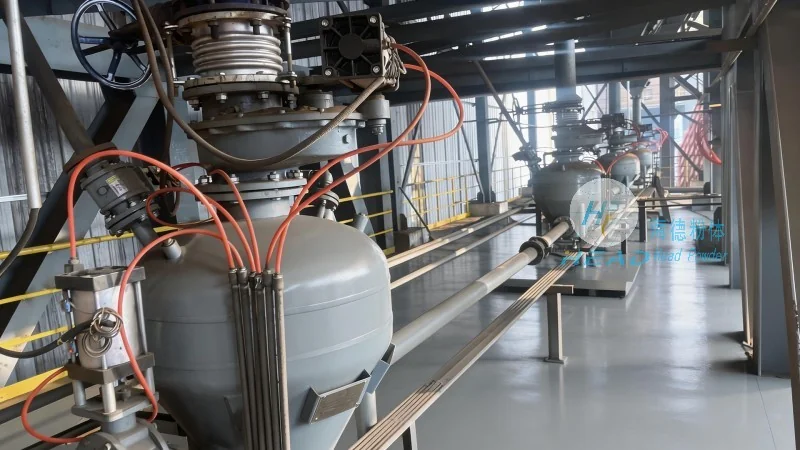
The operational principles of a corn cob powder conveying system involve the movement of material through the conveyor components. In pneumatic conveying, the corn cob powder is suspended in a stream of air and transported under pressure. The system uses a pressure differential between the source and destination to move the material, with control valves adjusting the air flow to maintain consistent pressure and flow rate. Filters are used to remove any particulate matter from the air stream, preventing clogging and ensuring clean operation. Mechanical conveying systems, like screw conveyors, use rotating screws to push the material along the conveyor path. The screw design, including pitch and diameter, is optimized for the particle size and density of the corn cob powder, ensuring efficient transfer without excessive wear. The operational principles must be carefully balanced to avoid issues such as overloading, which can lead to system failure or material degradation. Proper monitoring and control systems are essential to maintain optimal performance and prevent operational issues.
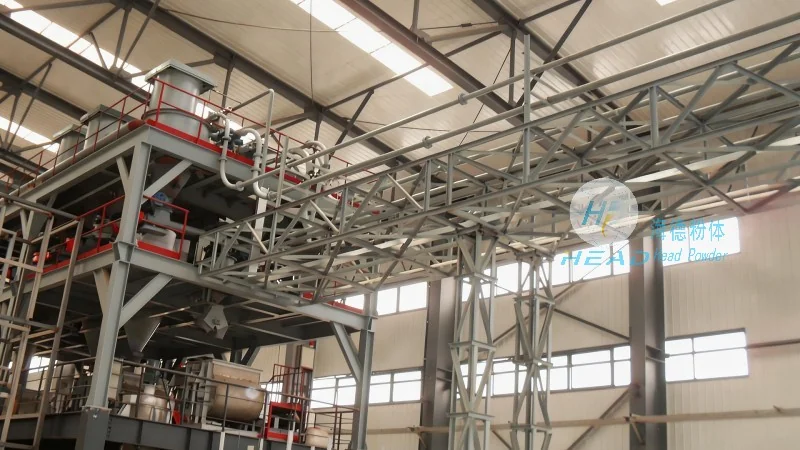
Shandong HeadPowder Engineering Co., Ltd., branded as headpowder, is a prominent manufacturer of specialized powder handling equipment, including corn cob powder conveying systems. HeadPowder specializes in designing and manufacturing customized solutions tailored to the unique requirements of the agricultural and food processing sectors. The company's team of experienced engineers and technicians works closely with clients to understand their production needs and develop systems that enhance efficiency and product quality. HeadPowder's expertise in material handling technology allows them to address the specific challenges of corn cob powder, such as its abrasive nature and variable particle size. The company's facilities in Shandong, China, are equipped with advanced manufacturing capabilities, enabling the production of high-quality, durable conveying systems. HeadPowder provides comprehensive services, from initial design and engineering to installation and maintenance, ensuring that clients receive reliable and long-lasting solutions. The company's commitment to quality and customer satisfaction has established it as a trusted partner in the industry, serving clients both domestically and internationally with innovative and effective powder handling solutions.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top