With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Ammonium bicarbonate, a vital chemical compound used in food processing, pharmaceuticals, and other industrial applications, requires efficient and safe handling during transportation and processing. The pneumatic conveying system is a sophisticated method designed to address these needs, ensuring the material is transported with minimal loss and contamination. This overview delves into the operational principles and structural design of such a system, highlighting its importance in modern industrial operations.
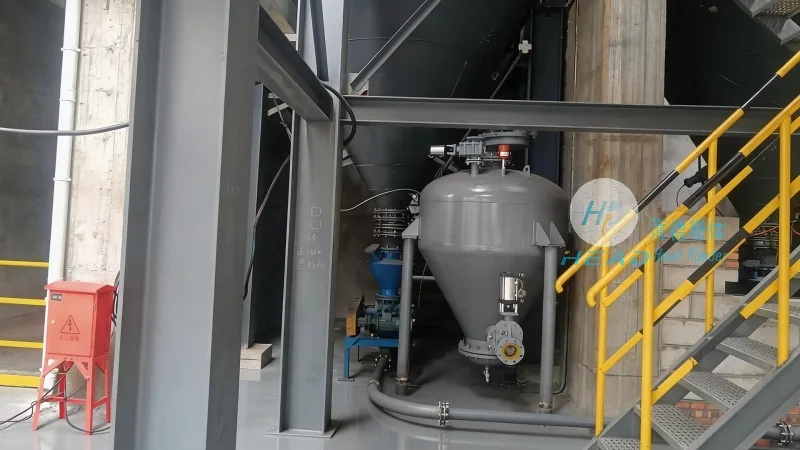
Headpowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading engineering firm dedicated to providing advanced solutions for powder handling and material transportation. With headquarters in Shandong, China, the company has built a reputation for excellence in designing and manufacturing customized pneumatic conveying systems. Headpowder's team of experienced engineers and technicians focuses on understanding the unique requirements of each client, developing tailored solutions that enhance operational efficiency and safety. The company's commitment to quality is evident in its adherence to international standards and continuous innovation in technology.
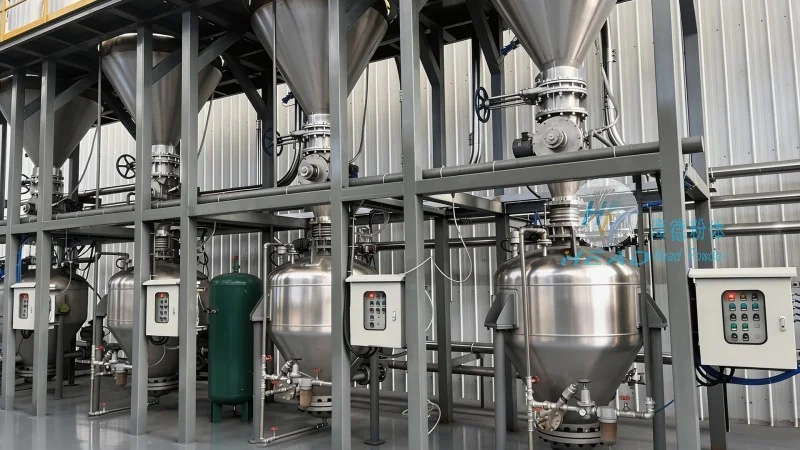
The pneumatic conveying system for ammonium bicarbonate operates on the principle of transporting material through a pipeline using compressed air. The system's structure comprises several critical components, each playing a vital role in the overall process. The hopper, typically made of stainless steel or other corrosion-resistant materials, serves as the primary storage and feeding unit. It is designed to hold the ammonium bicarbonate and feed it into the conveyor pipeline at a controlled rate. The conveyor pipeline, usually constructed from durable plastic or metal, is equipped with bends and elbows to navigate the system layout while maintaining low pressure drop. The blower or air compressor generates the necessary airflow, creating a pressure differential that propels the material forward. Control valves and regulators are integrated to manage the air pressure and flow rate, ensuring stable and consistent material transport. The system may also include filters and cyclones to separate the material from the air, preventing dust accumulation and maintaining air quality. The structural design prioritizes safety and efficiency, with features such as explosion-proof components for handling potentially hazardous materials and automatic shut-off mechanisms to prevent overloading.
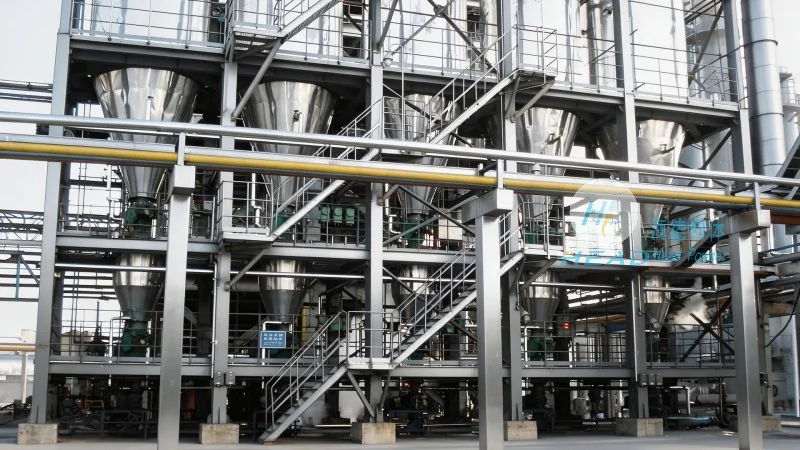
Adopting a pneumatic conveying system for ammonium bicarbonate offers numerous benefits that improve overall operational performance. One of the key advantages is the elimination of manual handling, which significantly reduces the risk of dust exposure and related health hazards. The enclosed system prevents material loss and contamination, ensuring the purity of ammonium bicarbonate is maintained throughout the transportation process. Additionally, the automated operation enhances productivity by reducing downtime and labor costs. The system's flexibility allows for easy integration with existing production lines, and its modular design enables scalability to accommodate increasing production demands. Furthermore, the consistent flow rate and pressure control provided by the system ensure reliable delivery of the material to downstream processing units, minimizing bottlenecks and improving overall efficiency. These advantages make the pneumatic conveying system a preferred choice for industries seeking to optimize their material handling processes.
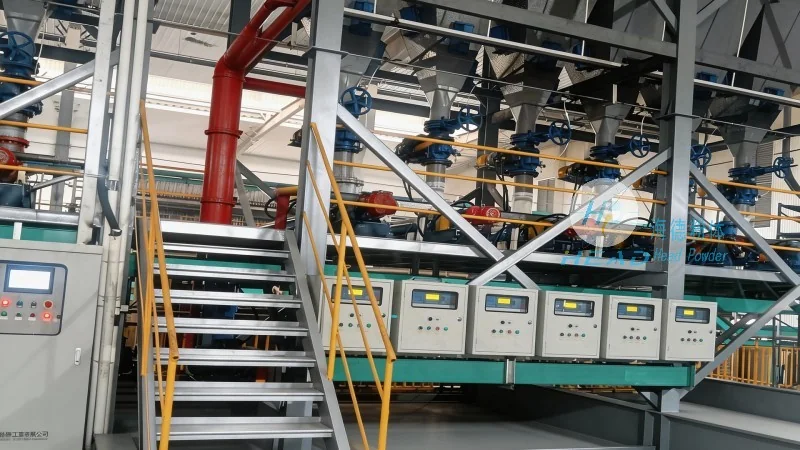
The pneumatic conveying system for ammonium bicarbonate finds extensive applications in various industries, including food and beverage, pharmaceuticals, and chemical manufacturing. In the food industry, it is used for transporting ammonium bicarbonate used as a leavening agent in baking, ensuring precise dosing and maintaining product quality. In pharmaceutical applications, the system is crucial for handling ammonium bicarbonate used in drug formulations, where purity and consistency are paramount. The system's ability to handle sensitive materials without degradation makes it ideal for these sectors. The impact of this technology extends beyond individual companies, contributing to the overall efficiency and safety of industrial operations. By reducing manual labor and minimizing material loss, the system supports sustainable practices and enhances the competitiveness of businesses in the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top