With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in industrial material handling solutions. The company's product line includes advanced tonne bag unloading material conveying equipment designed to optimize bulk material processing in various industrial applications.
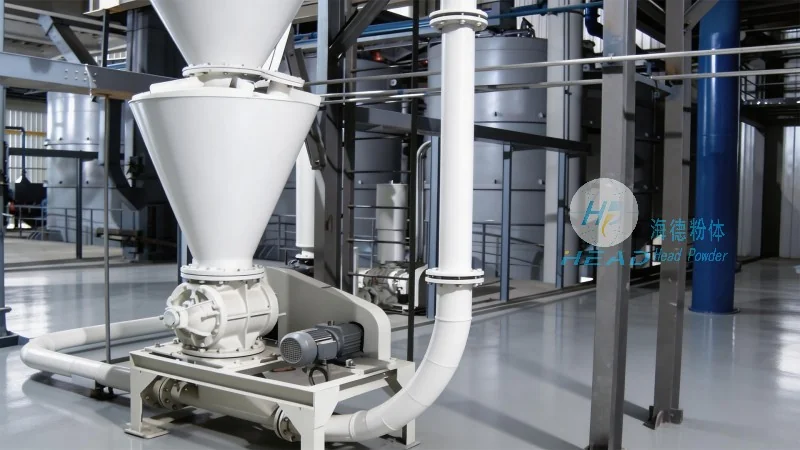
The tonne bag unloading material conveying equipment operates on a systematic principle that integrates multiple mechanical components to efficiently transfer bulk materials from large bags into processing systems. At its core, the equipment typically consists of a bag opening mechanism, a feeding hopper, and a conveyor system. The bag opening mechanism, often equipped with hydraulic or mechanical actuators, safely and reliably opens the top of the tonne bag to release the contained material. This is followed by a feeding hopper that collects the material and feeds it into a conveyor belt or screw conveyor. The conveyor system then transports the material to the next stage of processing, such as storage silos or processing units. The entire process is designed to minimize material loss and ensure consistent flow, making it suitable for handling a wide range of bulk materials like grains, chemicals, and powders.
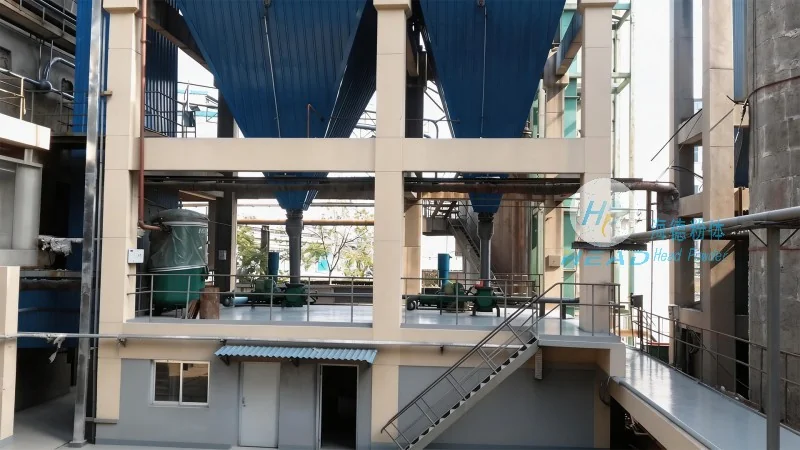
The working scene characteristics of tonne bag unloading material conveying equipment are tailored to meet the demands of diverse industrial environments. These characteristics include high efficiency, low maintenance requirements, and adaptability to different material types. In industrial settings, such as food processing plants, chemical manufacturing facilities, and mining operations, the equipment is deployed to handle large volumes of bulk materials with minimal human intervention. The design emphasizes durability and reliability, ensuring continuous operation even under heavy load conditions. The equipment is also engineered to handle various bag sizes and materials, providing flexibility in material handling. Additionally, the working scene often involves integration with other processing equipment, such as silos and mixers, to form a seamless material flow system. This integration enhances overall operational efficiency and reduces downtime, making the equipment a critical component in modern industrial material handling workflows.
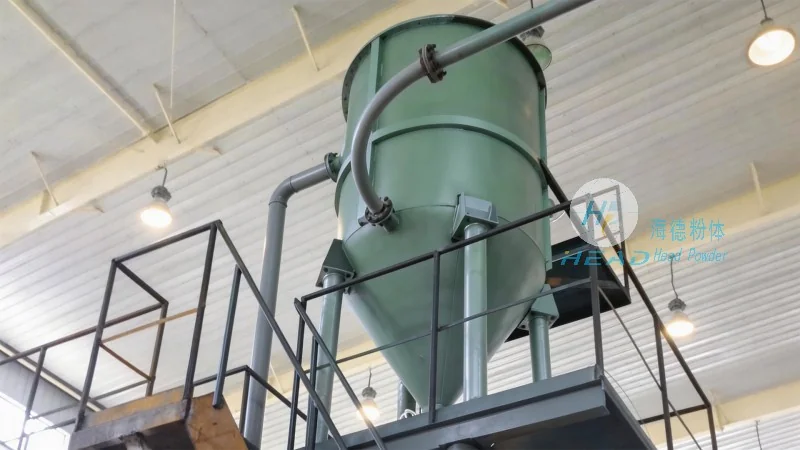
When deployed in real-world industrial scenarios, the tonne bag unloading material conveying equipment offers several key features and benefits that contribute to improved operational performance. One of the primary advantages is its ability to handle large quantities of material quickly and efficiently, reducing the time required for material transfer. The equipment's design minimizes material spillage and contamination, maintaining product quality and adhering to safety standards. Additionally, the system is equipped with safety features, such as emergency stop buttons and overload protection, to ensure safe operation in busy industrial environments. The low maintenance design of the equipment reduces operational costs and increases uptime, as fewer parts require regular servicing. Furthermore, the adaptability of the equipment allows it to be customized for specific material types and processing requirements, providing tailored solutions for different industrial applications. These features collectively enhance the equipment's effectiveness in various working scenes, making it a preferred choice for industries that rely on consistent and reliable material handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top